
Quick answer: An injection filling machine can support FDA and GMP expectations through hygienic design, controlled product-contact materials, cleanable components, documented functions, factory acceptance testing and qualification support. The machine itself should not be described as FDA-certified or as an automatic guarantee of GMP compliance.
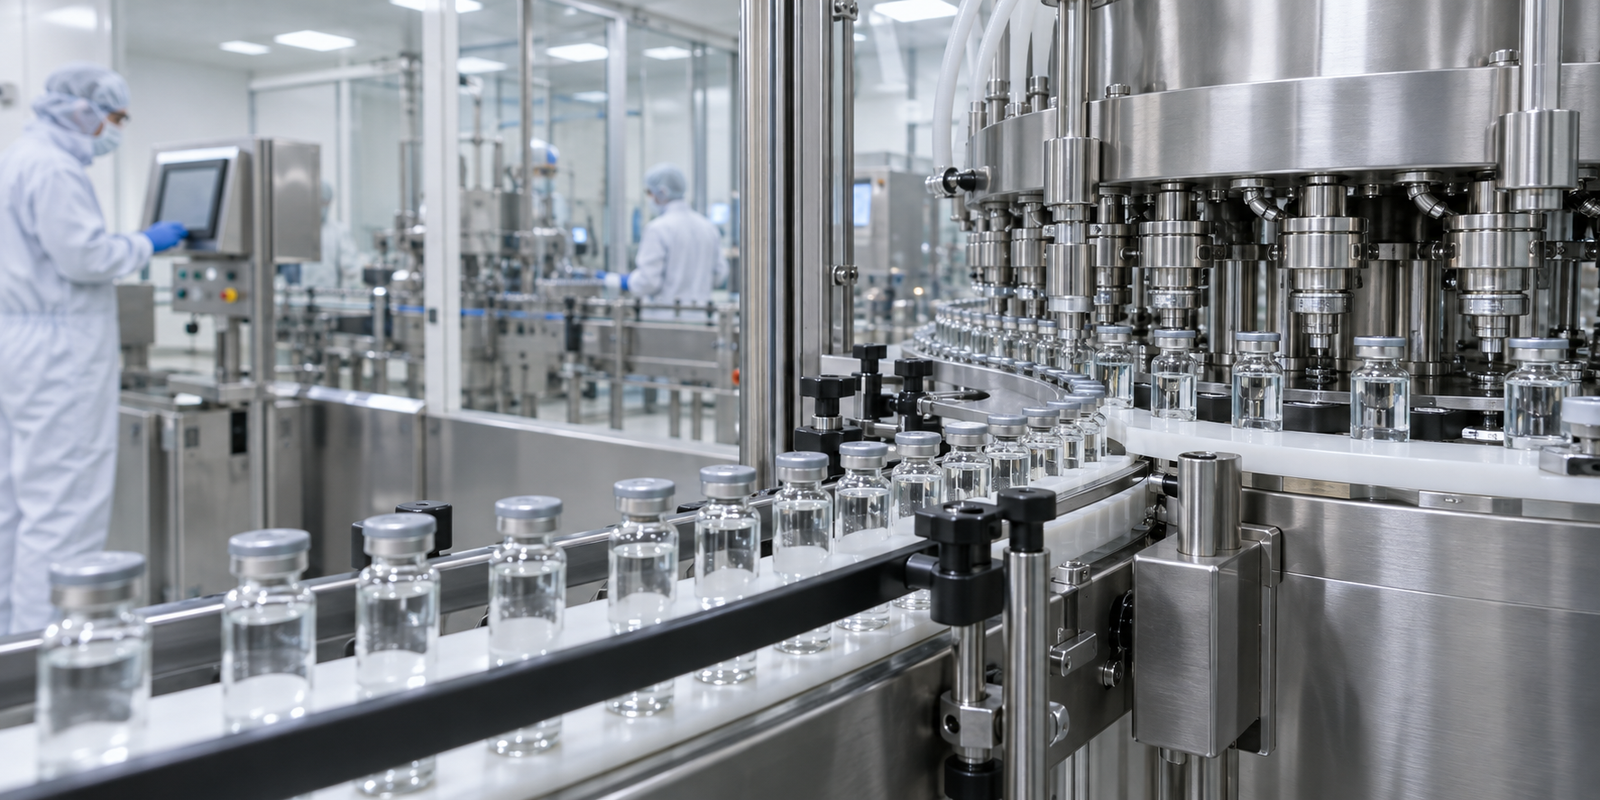
How an Injection Filling Machine Can Support FDA and GMP Requirements
Pharmaceutical buyers often search for an “FDA GMP injection filling machine” when they need equipment that can be integrated into a controlled manufacturing process. In practice, the question is broader than whether the machine is made from stainless steel. Quality teams also need to understand the product-contact path, cleaning access, materials, software or control functions, testing records, calibration and documentation.
FDA and GMP requirements apply to the complete manufacturing system: facility, utilities, procedures, personnel, materials, process controls, validation and quality management. The equipment supplier’s role is to provide a suitable machine and technical evidence that can support the customer’s qualification and validation program. Final compliance remains the responsibility of the manufacturer and its qualified quality and regulatory teams.
What customers usually mean by FDA and GMP requirements
Quality and regulatory expectations
Quality teams may ask for traceable product-contact materials, cleaning instructions, calibration records, change-control information, equipment qualification support, maintenance procedures and a controlled document package. They may also need evidence that critical alarms and interlocks have been tested.
Engineering and procurement expectations
Engineering teams normally review layout, utilities, product-contact parts, machine access, changeover, integration and maintenance. Procurement teams need a clear scope of supply, delivery terms, spare parts, training, warranty and FAT requirements. A good proposal addresses each group without using vague compliance language.
Hygienic design and cleanability
Hygienic design should be assessed against the intended application. Review smooth surfaces, minimized product traps, accessible product-contact parts, protected cables, suitable seals and the ability to inspect or remove components. Ask for drawings or photographs of the pump, tubing, valves, tank, filling needles and change parts rather than relying on a general phrase such as “GMP design.”
Cleanability is a practical question. Can the product pathway be flushed? Can parts be removed without excessive tools? Are there difficult-to-reach areas? Are cleaning status and line clearance identified? The answer depends on whether the design uses disposable tubing, removable stainless steel parts, fixed piping, CIP or another arrangement.
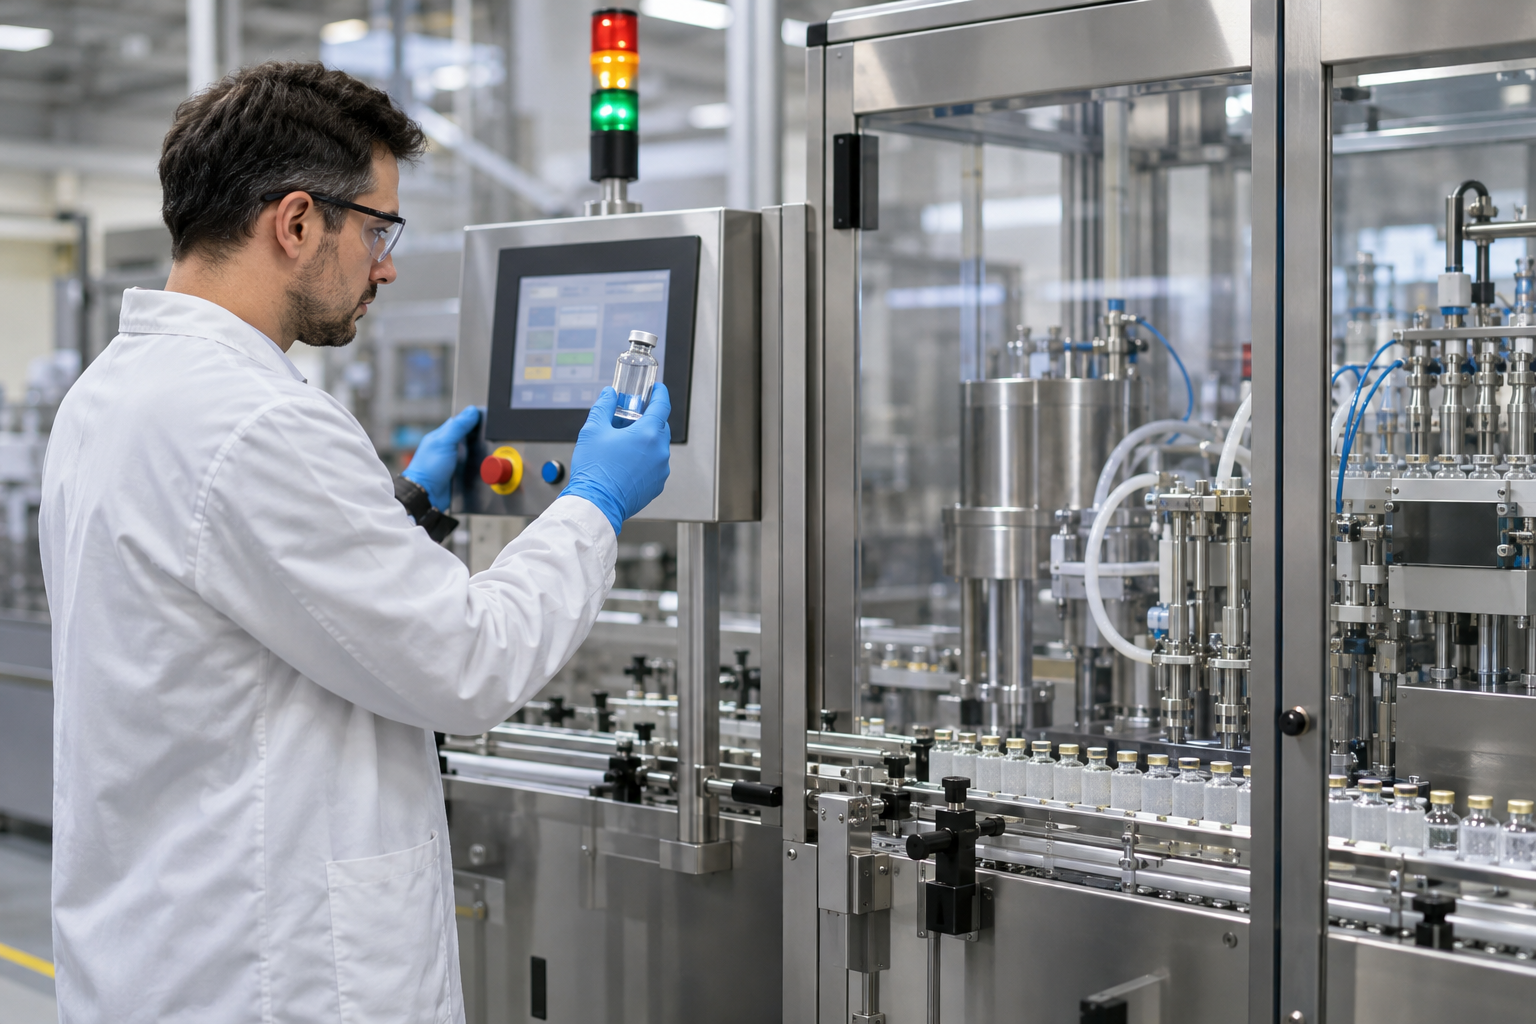
Material selection and traceability
Product-contact materials must be reviewed for compatibility with the formulation, cleaning agents and sterilization conditions. A documentation request may include stainless steel information, tubing specifications, seal and gasket materials, surface-finish information where relevant and certificates for critical parts.
The required level of documentation varies by project. Agree the document list before manufacture. It is much easier to plan certificates, drawings and test records at the beginning than to add them after shipment.
Cleaning and sterilization considerations
A filling machine should fit the customer’s cleaning and sterilization strategy. Ask whether product-contact parts are removable, how tubing is sterilized or replaced, whether CIP or SIP is required, how cleaning status is identified and which parts need separate preparation.
For some applications, a disposable product path can reduce cleaning complexity. For others, a fixed stainless steel path may be preferred because of batch size or facility design. The customer’s quality unit should approve the cleaning procedure and acceptance criteria. A supplier can provide recommendations and technical information but should not claim that an untested procedure is validated.
Supporting equipment qualification
Design qualification
The proposed equipment is reviewed against the User Requirement Specification. The review should identify included functions, excluded functions, utilities, product-contact materials and documentation.
Factory acceptance testing
FAT can verify start and stop functions, filling-volume adjustment, speed ranges, alarms, safety interlocks, no-container-no-fill, reject functions, sensors, recipes and format changeover. Use representative containers whenever possible.
Installation and operation checks
After delivery, the customer verifies installation, utilities, manuals, component identity and operation across the defined ranges. Performance qualification then evaluates the machine under approved production or representative conditions.
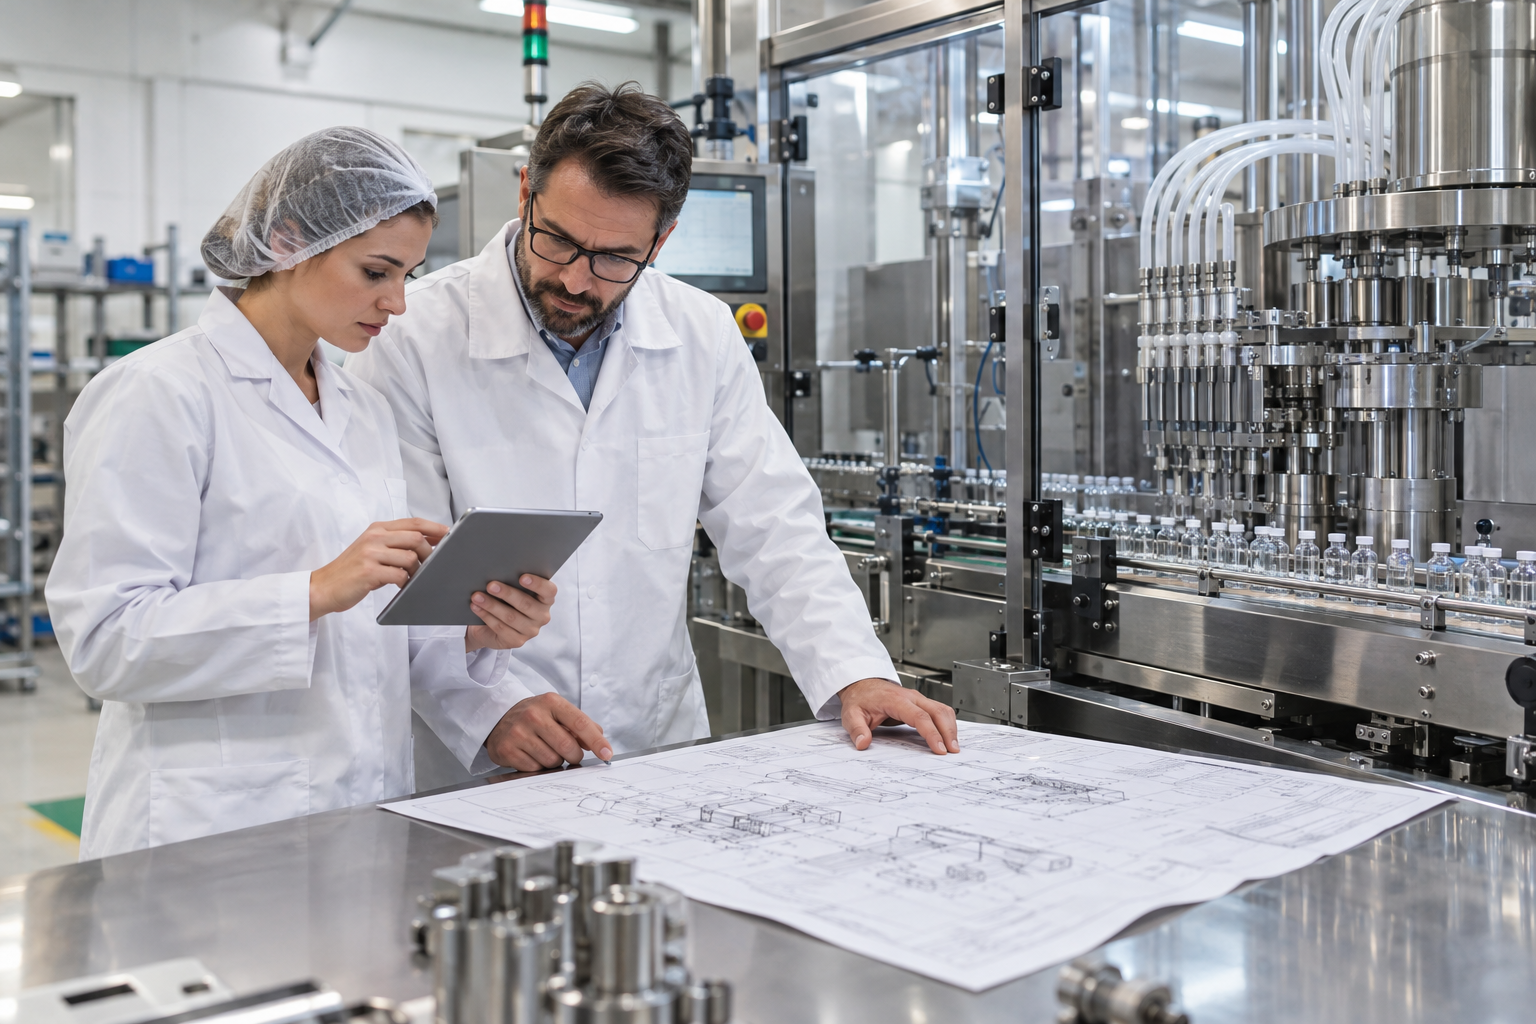
Documentation that may be requested
- User Requirement Specification response
- Functional or design specification
- General arrangement, electrical and pneumatic drawings
- Product-contact parts list
- Component manuals and certificates
- Calibration or verification records
- FAT protocol and report
- Operation, maintenance and cleaning instructions
- Spare-parts and consumables list
- Preventive maintenance recommendations
- Risk-assessment and qualification support information
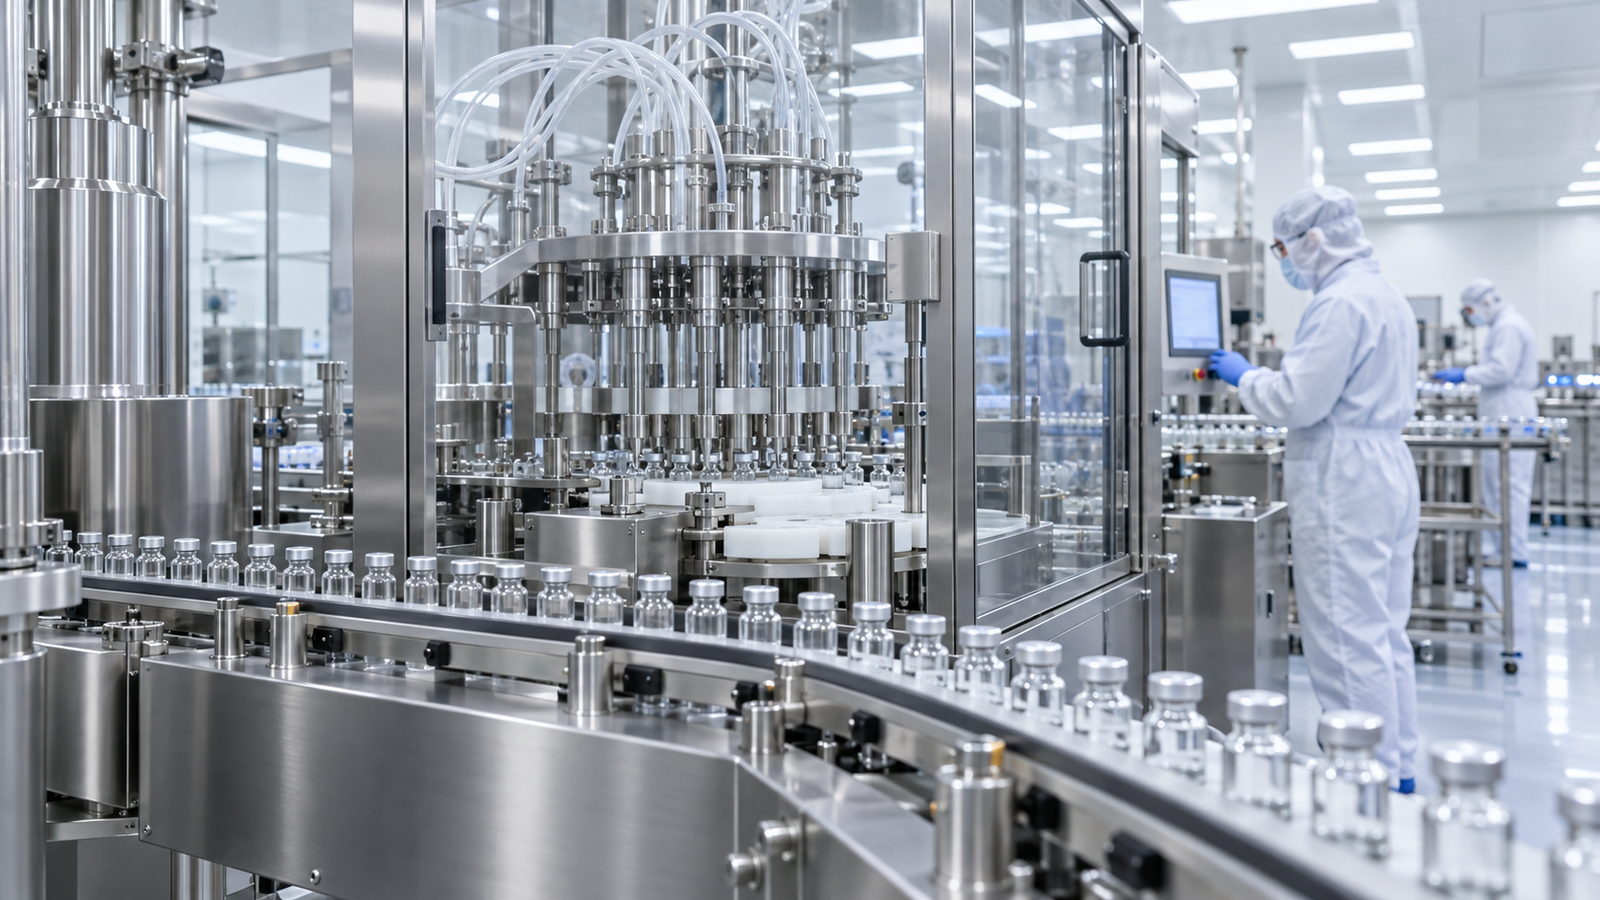
FAT, shipment inspection and installation preparation
FAT gives the customer an opportunity to identify open items before shipment. Test conditions, sample quantities, fill-volume checks and acceptance criteria should be written down. If the final product cannot be used at the factory, document the substitute liquid and the limitations of that test.
Shipment inspection should verify the approved configuration, change parts, spare parts, manuals, drawings, serial numbers and packing photographs. At the receiving site, prepare utilities, room access, lifting arrangements, cleanroom interfaces and operator training.
How to describe compliance accurately
Avoid phrases such as “FDA-approved machine,” “FDA-certified filling machine,” “GMP-certified equipment” or “guaranteed FDA compliance.” More accurate wording is: “designed to support pharmaceutical manufacturing requirements,” “suitable for integration into a GMP-controlled environment,” “documentation available within the agreed project scope,” and “qualification support available.”
For related equipment and project support, review the filling solutions, service and resources pages.
FAQ
Is an injection filling machine FDA certified?
A machine should not normally be described as FDA certified. FDA requirements apply to the regulated product and manufacturing process. The equipment can be designed and documented to support the customer’s qualification activities.
Does GMP design guarantee GMP compliance?
No. GMP compliance depends on the complete manufacturing system, including facility, utilities, procedures, personnel, controls and validation.
What documents should be requested?
Request drawings, product-contact materials, manuals, component records, calibration information, FAT documents, cleaning recommendations and the agreed qualification support package.
Can the supplier help with validation?
The supplier can provide technical documents, test protocols, certificates and support during FAT, installation and troubleshooting. The customer’s quality unit approves the final qualification program.
Conclusion and CTA
An FDA/GMP-oriented project should be managed as a documented equipment and process-support project. Hygienic design, material traceability, cleaning access, tested functions and a clear qualification package provide a more defensible basis for supplier evaluation.
Request the documentation package: Send your URS, container drawings, target output and required documents to our team. For project discussions, use the Contact King Pack page.
Build a documentation matrix before ordering
A documentation matrix should map each customer requirement to a document, test or responsible party. For example, product-contact material information may be supported by a component list and certificates; a filling-volume requirement may be checked during FAT and OQ; a cleaning requirement may need a supplier recommendation plus a customer-approved validation protocol. This matrix prevents the phrase “documentation included” from hiding important gaps.
The matrix should also distinguish supplier documents from customer documents. The supplier may provide drawings, manuals, test records and technical descriptions. The customer normally owns facility qualification, operating procedures, cleaning validation, process validation, environmental monitoring and final product release decisions.
Data, alarms and change control
Review what the control system records, which alarms are available, how recipes are protected and how changes are documented. The appropriate approach depends on the machine architecture and the customer’s data-integrity procedures. Do not assume that a touchscreen or a digital record automatically meets every regulatory expectation. Define the required records and review them with the customer’s quality and validation teams.
Change control is equally important after installation. A new product, container, pump, tubing material, software version or operating range may require an impact assessment. The supplier should identify the affected parts and recommended tests, while the customer decides whether its internal quality process requires formal approval.
Prepare the site before the machine arrives
Installation delays often come from site readiness rather than machine construction. Confirm doorway dimensions, floor loading, lifting access, electrical supply, compressed-air quality and pressure, drainage, HVAC interfaces and the location of upstream and downstream equipment. Confirm how the machine will be cleaned and where removed product-contact parts will be inspected.
Before SAT, prepare the approved drawings, utility checks, container samples, product or substitute liquid, test equipment and trained operators. The first site test should not be the first time the team discovers that a container is unavailable or a utility connection is unsuitable.
What a responsible supplier should clarify
- Which functions are standard and which are optional?
- Which product-contact materials are proposed?
- What is included in FAT, and what is tested at SAT?
- Which documents are included before shipment?
- Which requirements depend on the customer’s facility?
- Which statements are recommendations rather than validated results?
- How are open actions and post-installation support handled?
Clear answers are a sign of a manageable project. They also help the buyer avoid overreliance on unsupported phrases such as “fully FDA compliant” when the real need is a documented, testable and maintainable machine configuration.
Define critical equipment functions
Not every machine function has the same quality impact. The project team should identify critical functions such as fill-volume control, no-container-no-fill, container presence detection, stopper placement, cap handling, reject logic, emergency stop and alarms. For each function, define the expected behavior, test method, responsible person and record that will be produced.
This approach helps the customer focus its qualification effort. A non-critical convenience function may need an operation check, while a function that affects product quality or operator safety may require a more detailed test and documented acceptance range. The final categorization should be approved by the customer’s quality and engineering teams.
Review software and recipe control
If the filling machine uses recipes, review how the recipe is selected, edited, protected and backed up. Identify which parameters are operator-adjustable and which require a higher access level. The supplier should explain the control architecture and provide the information needed for the customer’s internal data-integrity review.
A recipe should not be treated as a substitute for a validated process. The customer still needs to establish the approved operating range, verify the correct container and product, and control changes according to its quality system. If a software or controller change is made later, evaluate whether re-testing is required.
Risk assessment and supplier communication
A practical risk review considers contamination, mix-ups, incorrect format parts, incorrect recipe selection, dosing variation, component failure, loss of utilities, alarm response, cleaning access and operator error. The supplier can provide technical input about the machine, but the customer should evaluate the risk in the context of its facility and process.
Write down open questions instead of accepting broad statements. Ask which parts are product-contact parts, which components have certificates, which functions are tested at FAT, what the customer must prepare for SAT and what limitations apply to substitute-liquid testing. This creates a useful evidence trail for procurement and quality review.
Qualification evidence should reflect the actual project
A generic factory test report is less useful than a project-specific record that identifies the approved machine configuration, serial numbers, change parts, software version, sample containers, test liquid, test speed and acceptance criteria. If the customer has several container formats, test the formats that are included in the order and list any future formats as options.
During installation, compare the delivered equipment with the approved drawings and packing list. Confirm utility connections, guards, sensors, manuals and calibration status. During operation checks, challenge the relevant ranges rather than checking only one nominal setting. During performance testing, use the product and operating method defined by the customer’s approved protocol.
Cleaning records and maintenance ownership
Clarify who owns each part of the cleaning workflow. The supplier may recommend how to disassemble a pump or remove a nozzle, but the customer decides the approved cleaning agent, inspection method, release status and record format. Maintenance ownership should be equally clear for tubing, seals, sensors, pumps, valves and format parts.
Provide operators with photographs or diagrams that identify the correct parts and assembly direction. This is especially useful when the line handles more than one product or container. A clear maintenance and cleaning record can support investigation if a residue or accuracy issue appears later.
Prepare for audit questions without overclaiming
During an audit or customer review, a team may be asked how the equipment was selected, which requirements were tested, how product-contact materials were controlled, how cleaning was defined, how changes are approved and how failures are investigated. A transparent file containing the URS, supplier response, drawings, FAT record, installation checks, operating tests and change history is more useful than a marketing claim about certification.
For customers evaluating a sterile filling line, the equipment file should be considered one part of the wider contamination-control and validation strategy. The facility, utilities, environmental monitoring, sterilization, container closure and process controls must be reviewed together.
King Pack can support the equipment side of this review through the solution, service and resource pages. Final requirements should be confirmed through the customer’s approved specifications and quality procedures.
Final compliance review questions
Before approval, ask whether the proposed equipment is traceable to the URS, whether the product-contact parts are identified, whether cleaning access has been reviewed, whether critical functions are included in FAT, whether the document list is agreed and whether the customer’s facility responsibilities are clear. Also ask how open actions, deviations and post-installation changes will be recorded. These questions do not replace the customer’s quality system, but they make the equipment package easier to qualify and maintain. They also support honest supplier communication because the project team can separate what is included, what is recommended and what must be proven during customer testing.
Use the contact page to request a project-specific documentation discussion.
Keep the compliance statement specific
The safest project language states what the equipment is designed to support, what has been tested, which documents are supplied and which activities remain with the customer. Specific wording improves trust and gives quality teams a clear basis for review.