
Temperature-Controlled Veterinary Filling
Veterinary Roll-On Applicator Filling & Capping Solution
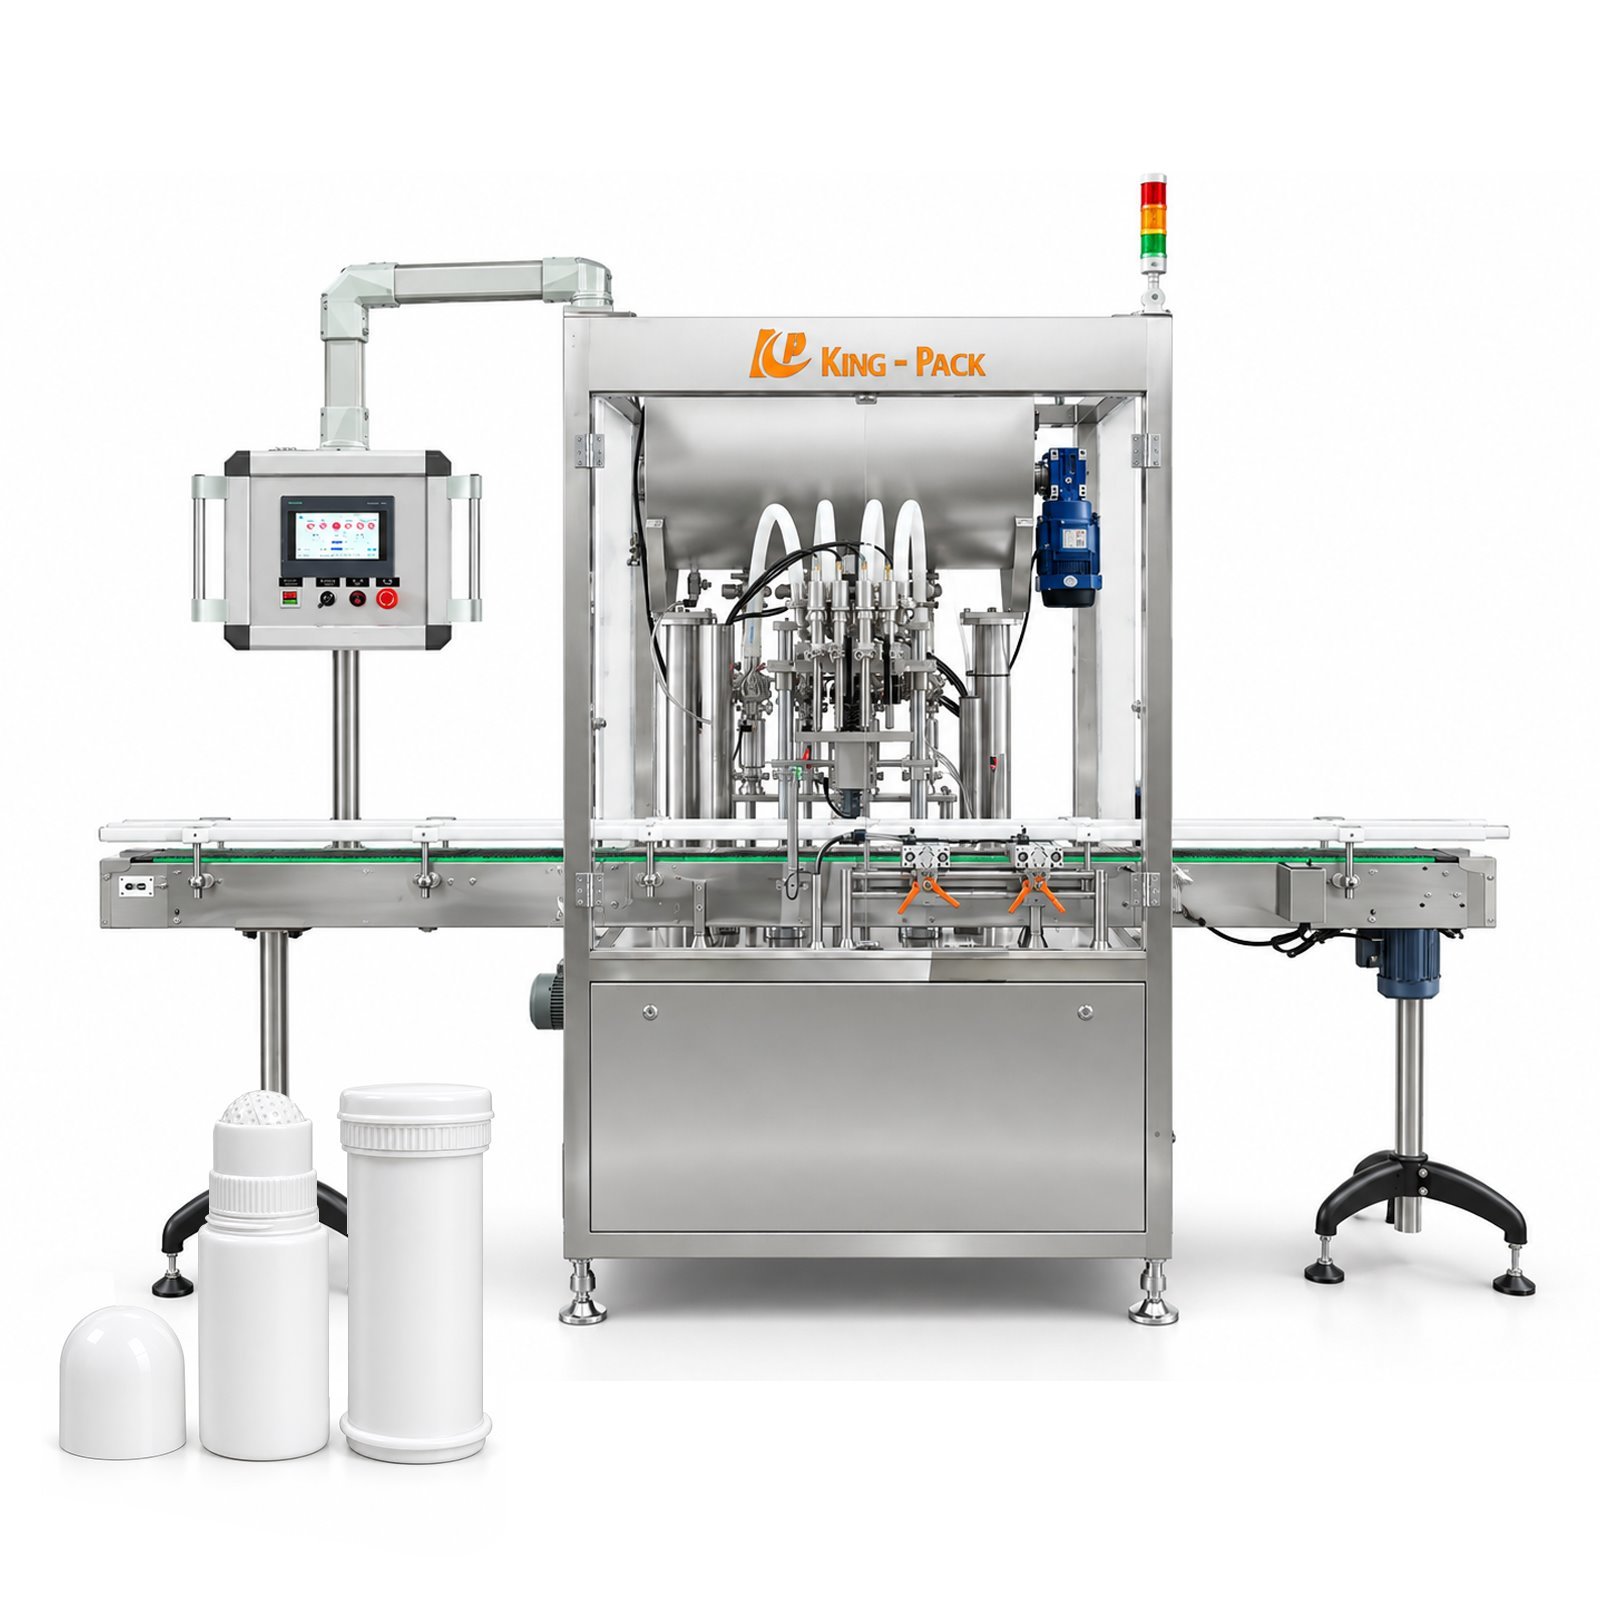
A configurable line for gel and semi-fluid products that combines heated product handling, four independently controlled servo piston pumps and package-specific roll-on closure handling.
Application Definition
Stable dosing starts with the product path, not only the filler.
Veterinary gels and nutritional pastes can thicken as temperature falls. KING PACK treats the hopper, metering pumps and transfer lines as one controlled system so the product reaches the filling nozzles under repeatable conditions.
Configured Process
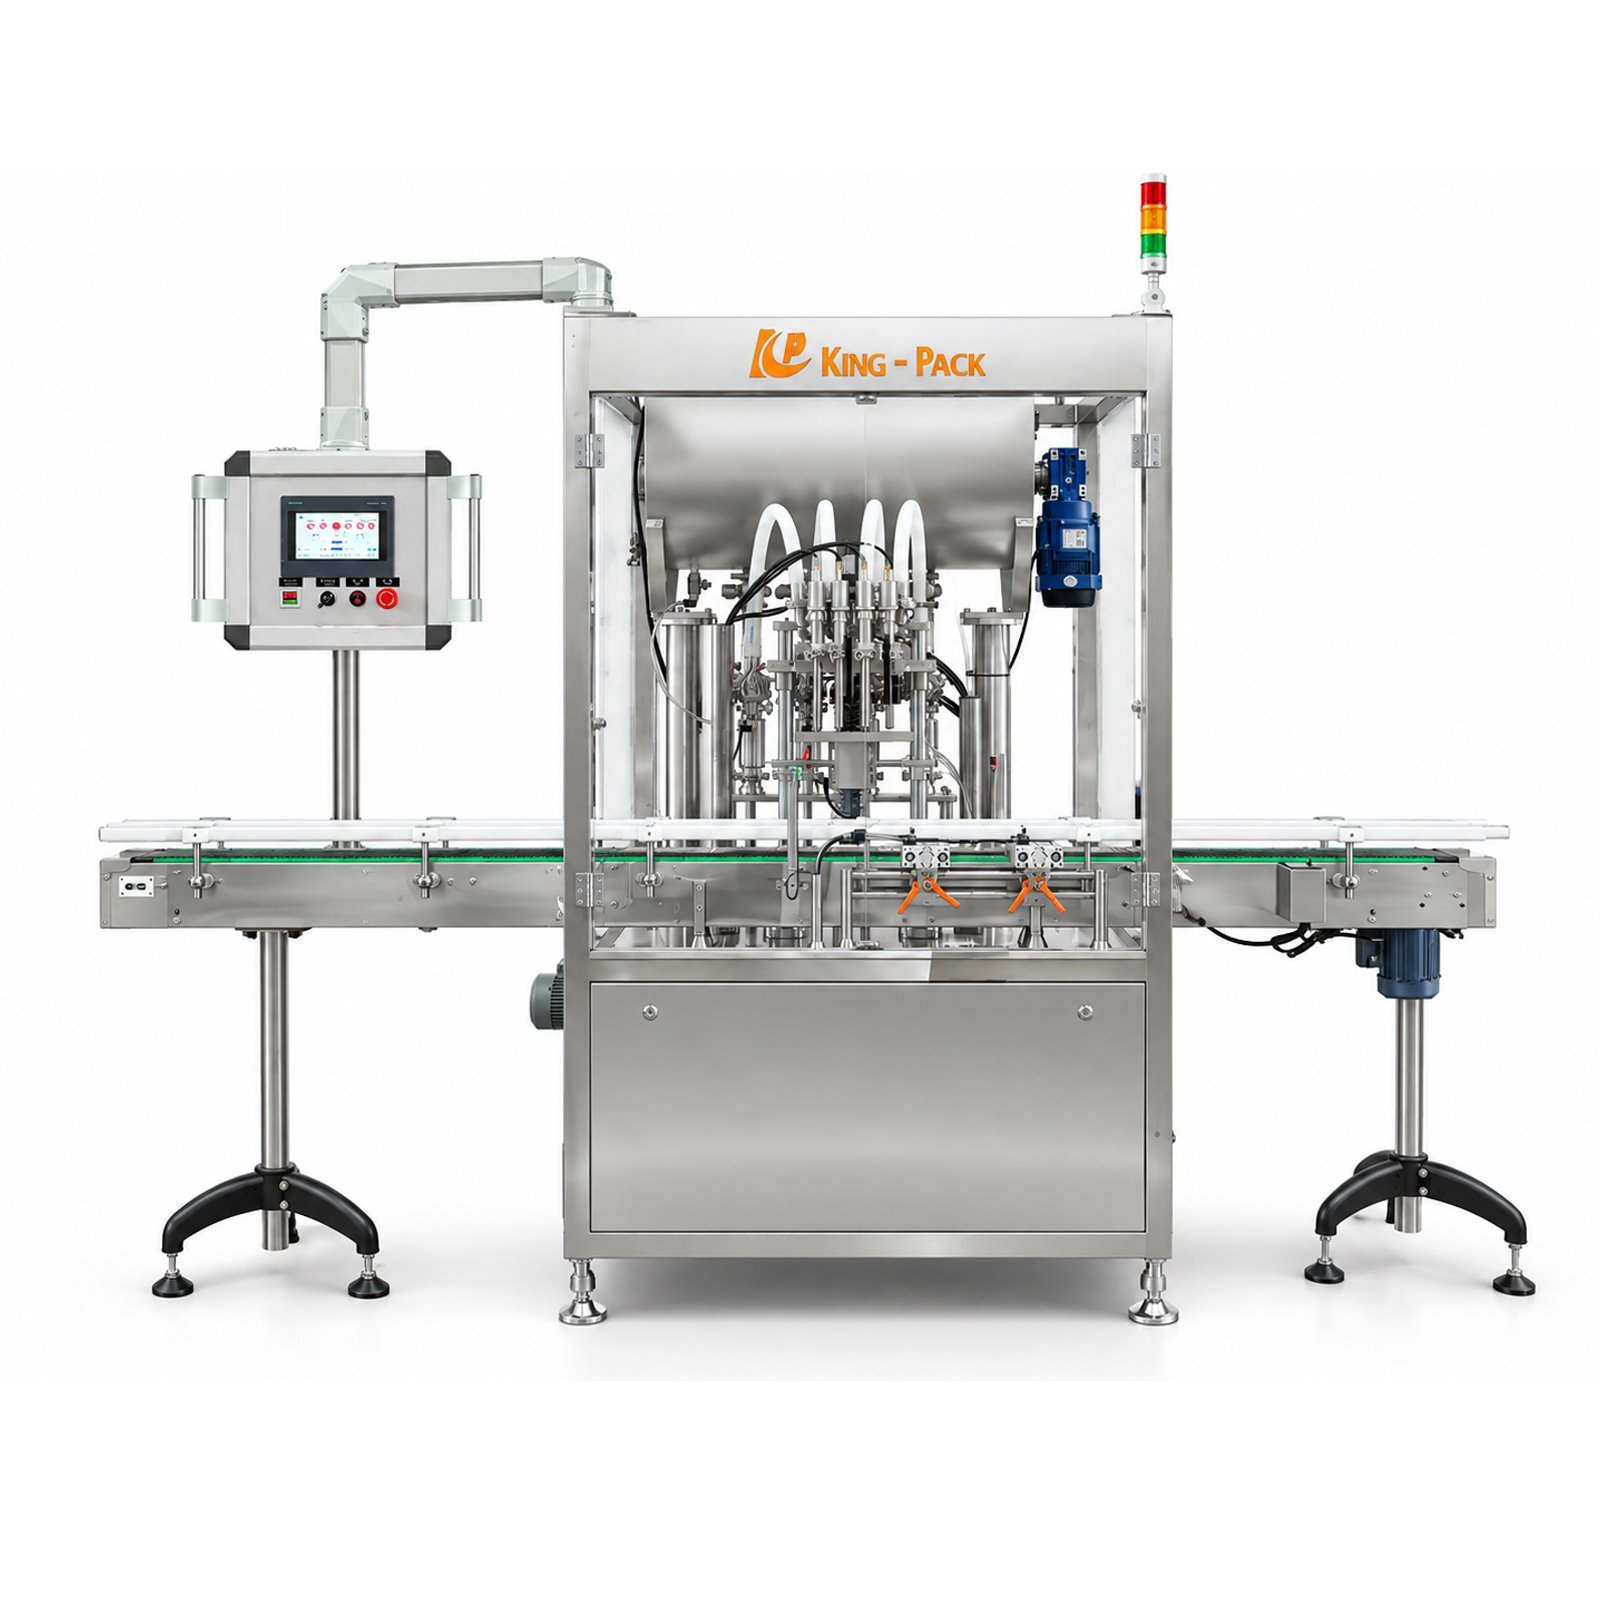
From bottle infeed to a closed roll-on package.
The final sequence is matched to the bottle, ball housing, fitment and cap construction. Automation level can be selected after component trials.
Bottle infeed & positioning
Containers enter the linear conveyor and are indexed by a package-specific positioning fixture.
Temperature-controlled filling
Four servo piston pumps meter the conditioned product while the nozzles follow the liquid level.
Roll-on fitment placement
The ball housing or roll-on insert is oriented and seated using tooling validated with the real component set.
Cap tightening & discharge
A matched capping method applies the closure before the finished bottle exits for downstream inspection or packing.
Uninterrupted Temperature Control
Keep viscosity predictable from storage to the nozzle.
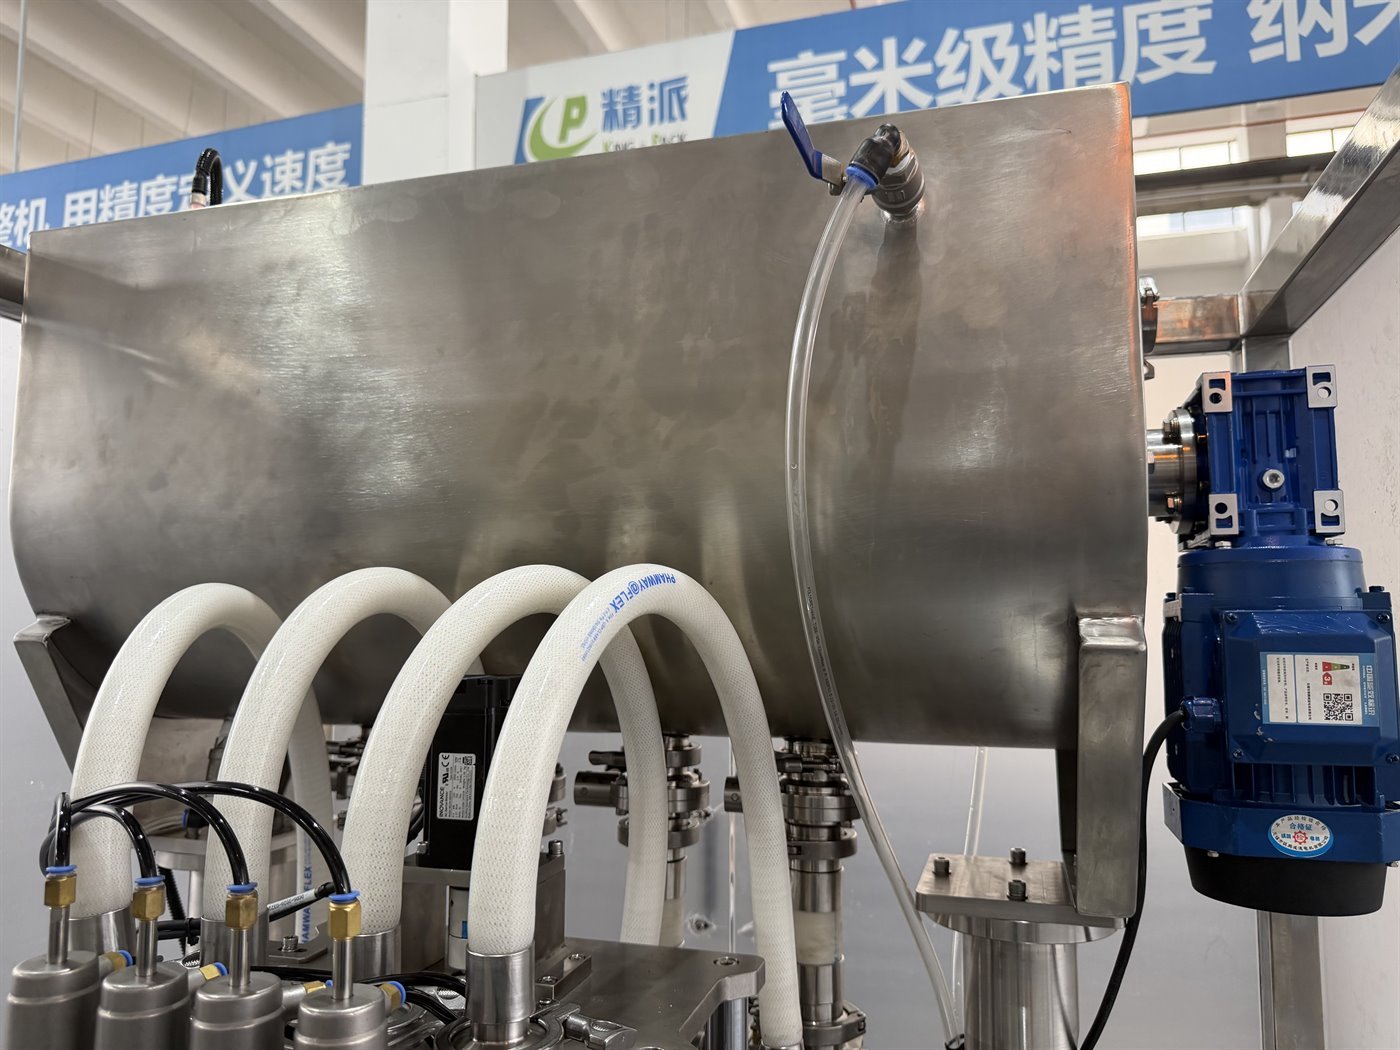
The reference configuration heats the filling hopper, piston-pump area and product lines. This reduces low-temperature thickening and supports steady flow during continuous production.
Servo Metering & Clean Cutoff
Four pumps, four recipes, one coordinated control layer.
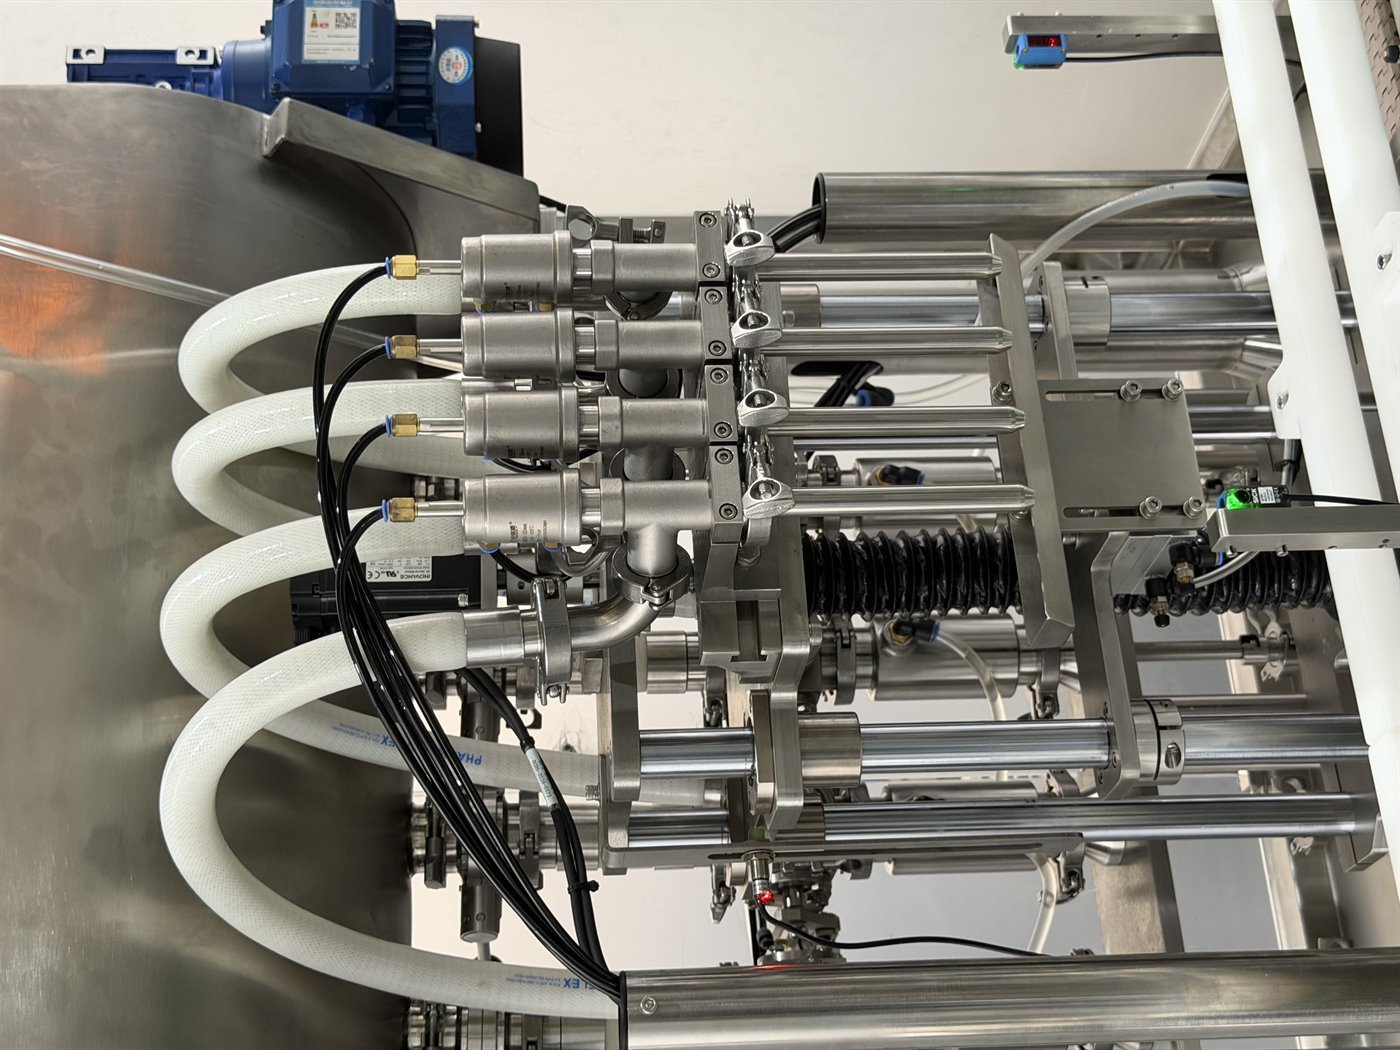
Four 316L piston pumps operate independently. Fill quantities can be set per pump, allowing mixed specifications or partial-head operation when output needs change.
Lifting nozzles travel with the product level to reduce impact and trapped air. At the end of the dose, the heads rise clear of the bottle to limit stringing, dripping and neck contamination.
Production-Ready Engineering
Built for controlled changeover, cleaning and repeatable operation.
Tooling-led changeover
Dedicated fixtures adapt the straight-line platform to round, flat or irregular bottles without changing the conveyor drive architecture.
Sanitary construction
SUS304 machine structure, product-contact components selected for the formula and sanitary quick-release connections simplify disassembly and cleaning.
One HMI for the process
Fill volume, speed, nozzle stroke and production recipes are coordinated from the main control interface instead of dispersed local adjustment.
Simple production route
Infeed, filling, closure handling and discharge follow one straight path for clear access and practical integration with downstream equipment.
Traceable electrical selection
The reference project uses Siemens control, Inovance servo systems and industrial components from established international suppliers.
Clean, rounded surfaces
Smooth transitions and guarded motion areas reduce sharp contact points and material traps around the operator and package path.
Machine Detail
See the product path, controls and dosing hardware.
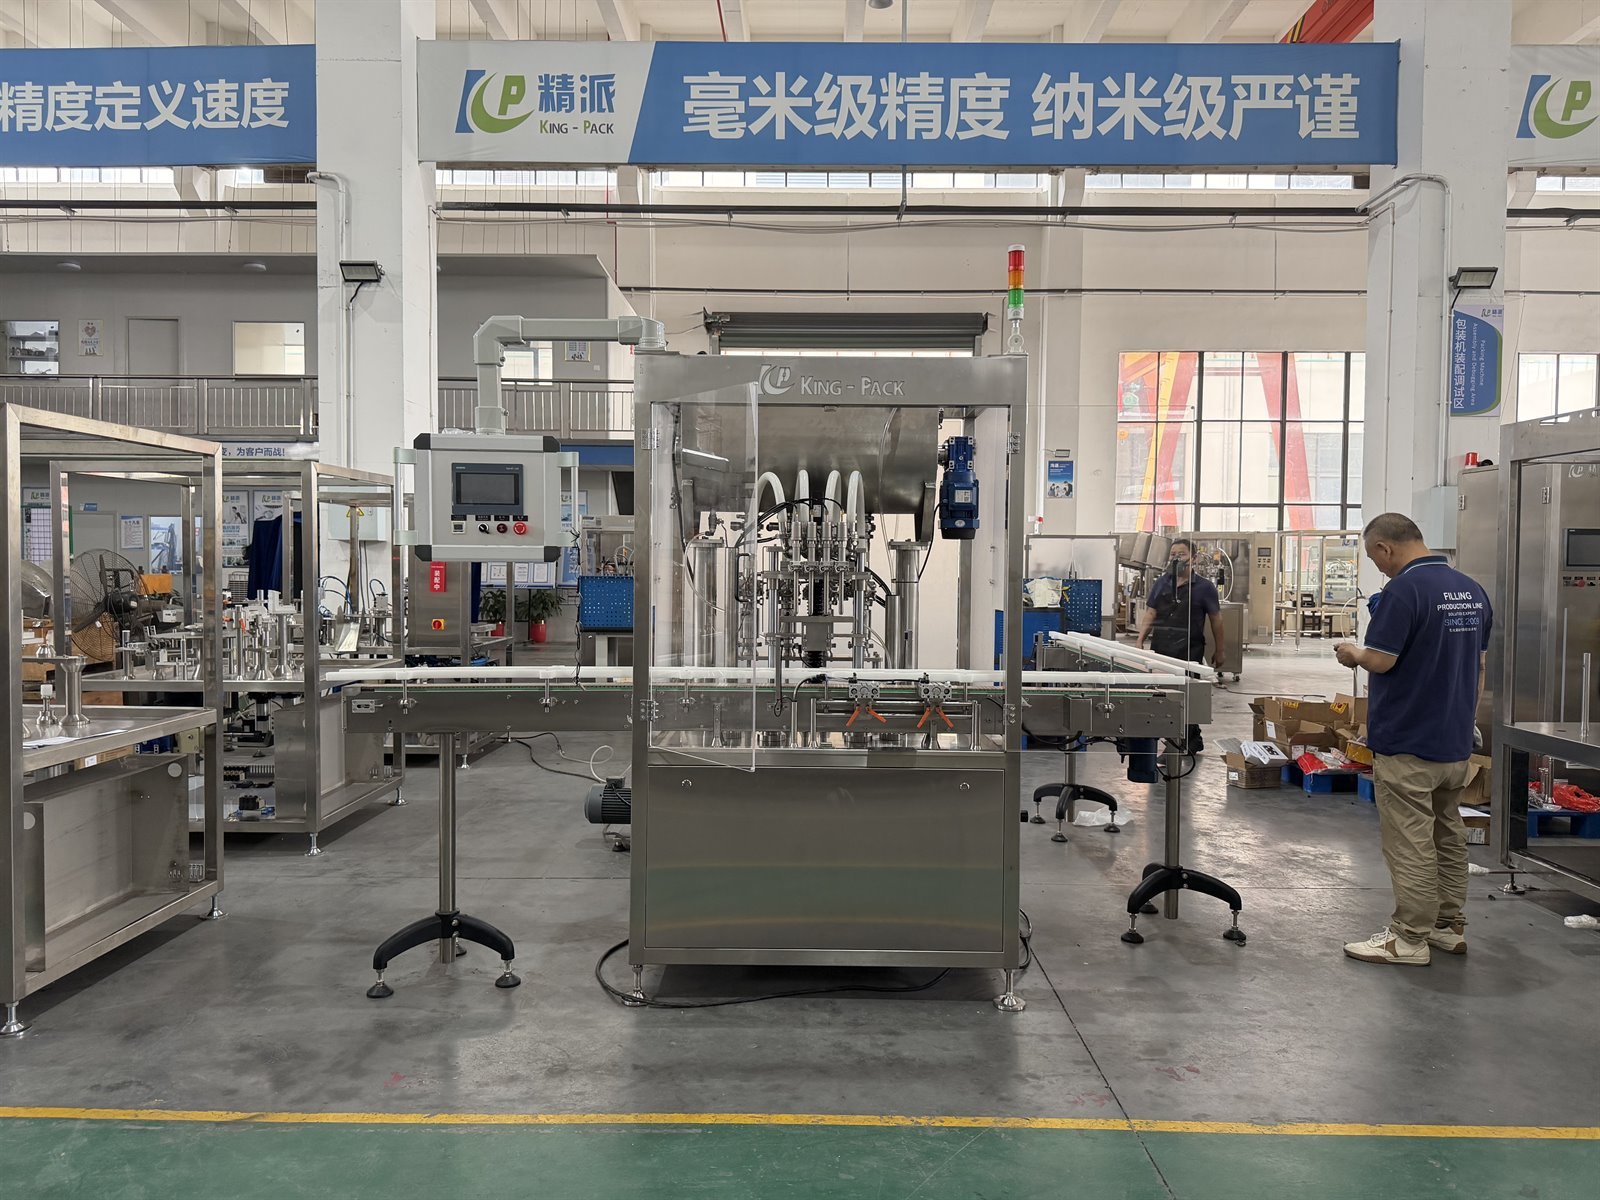
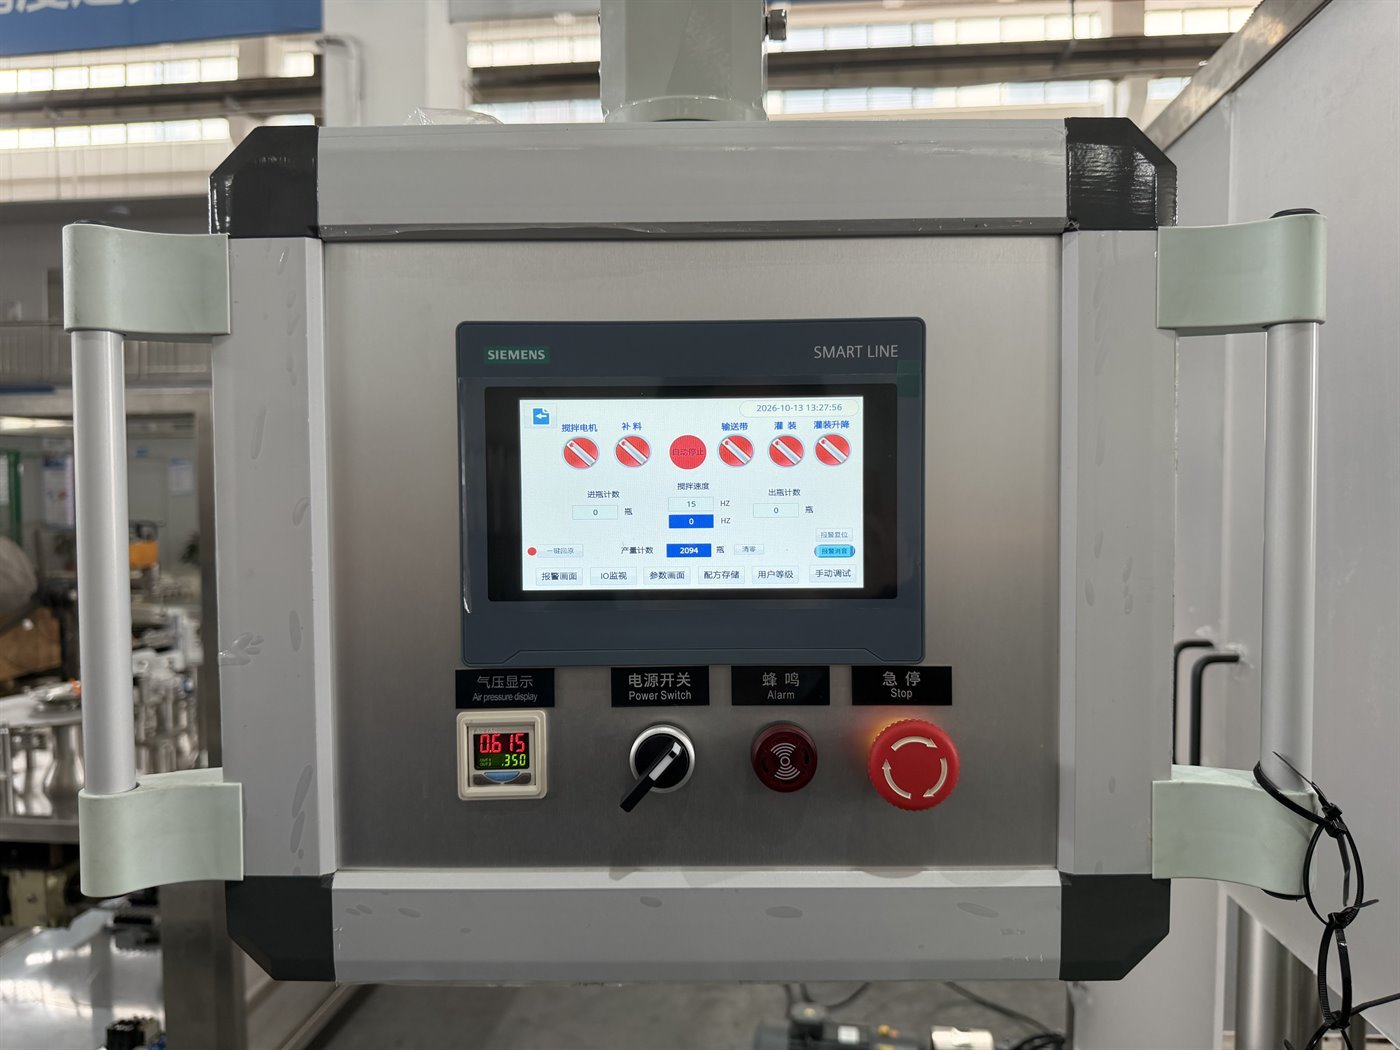
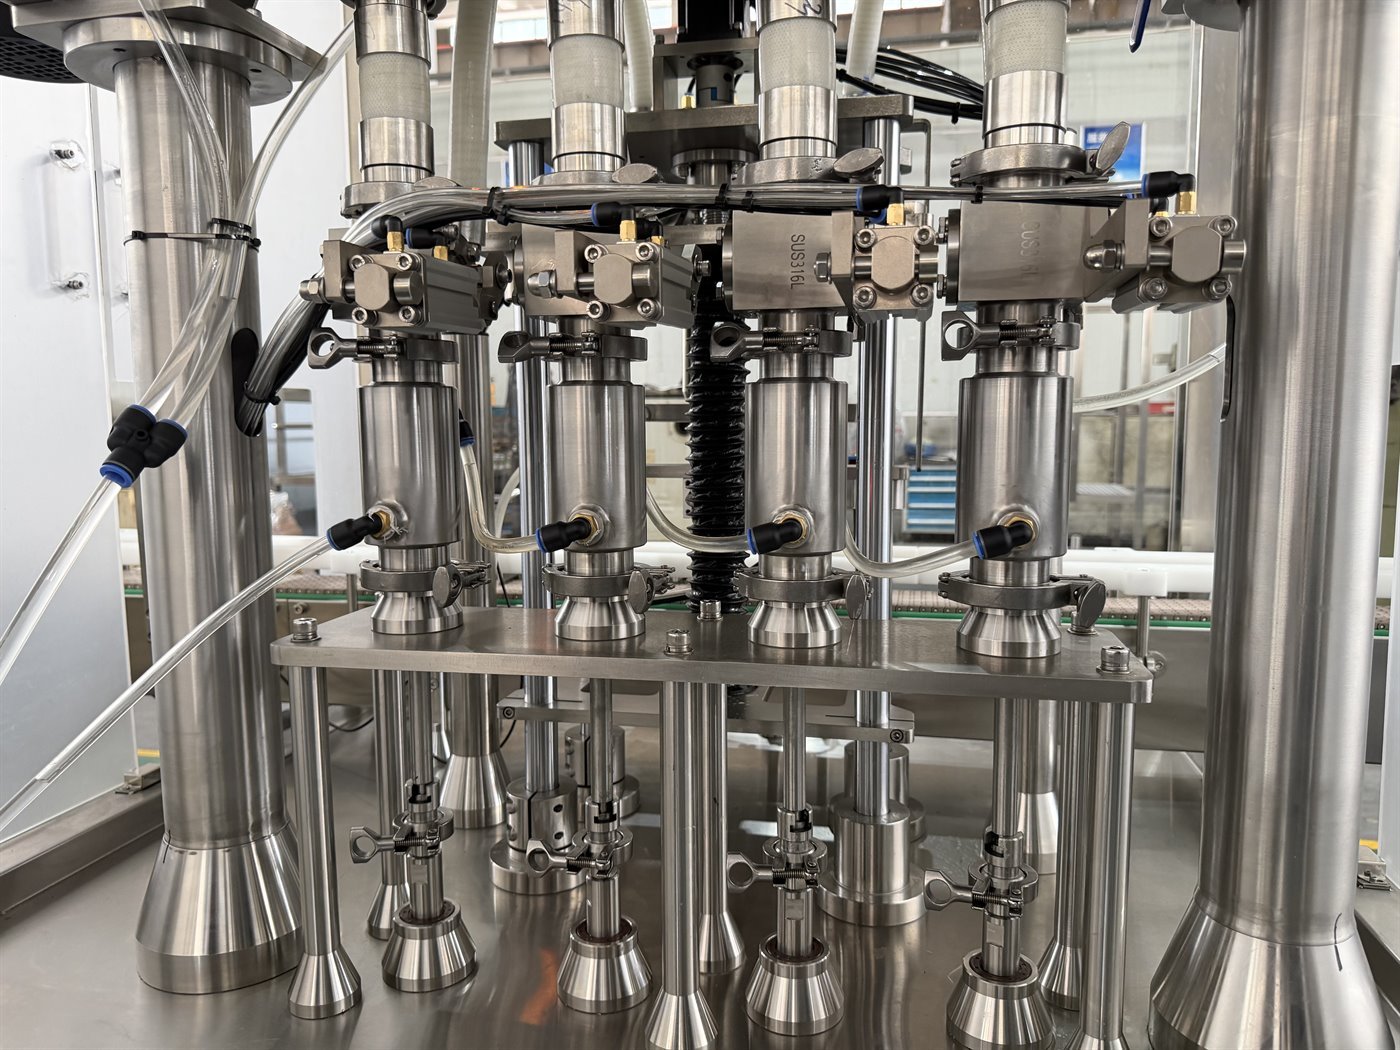
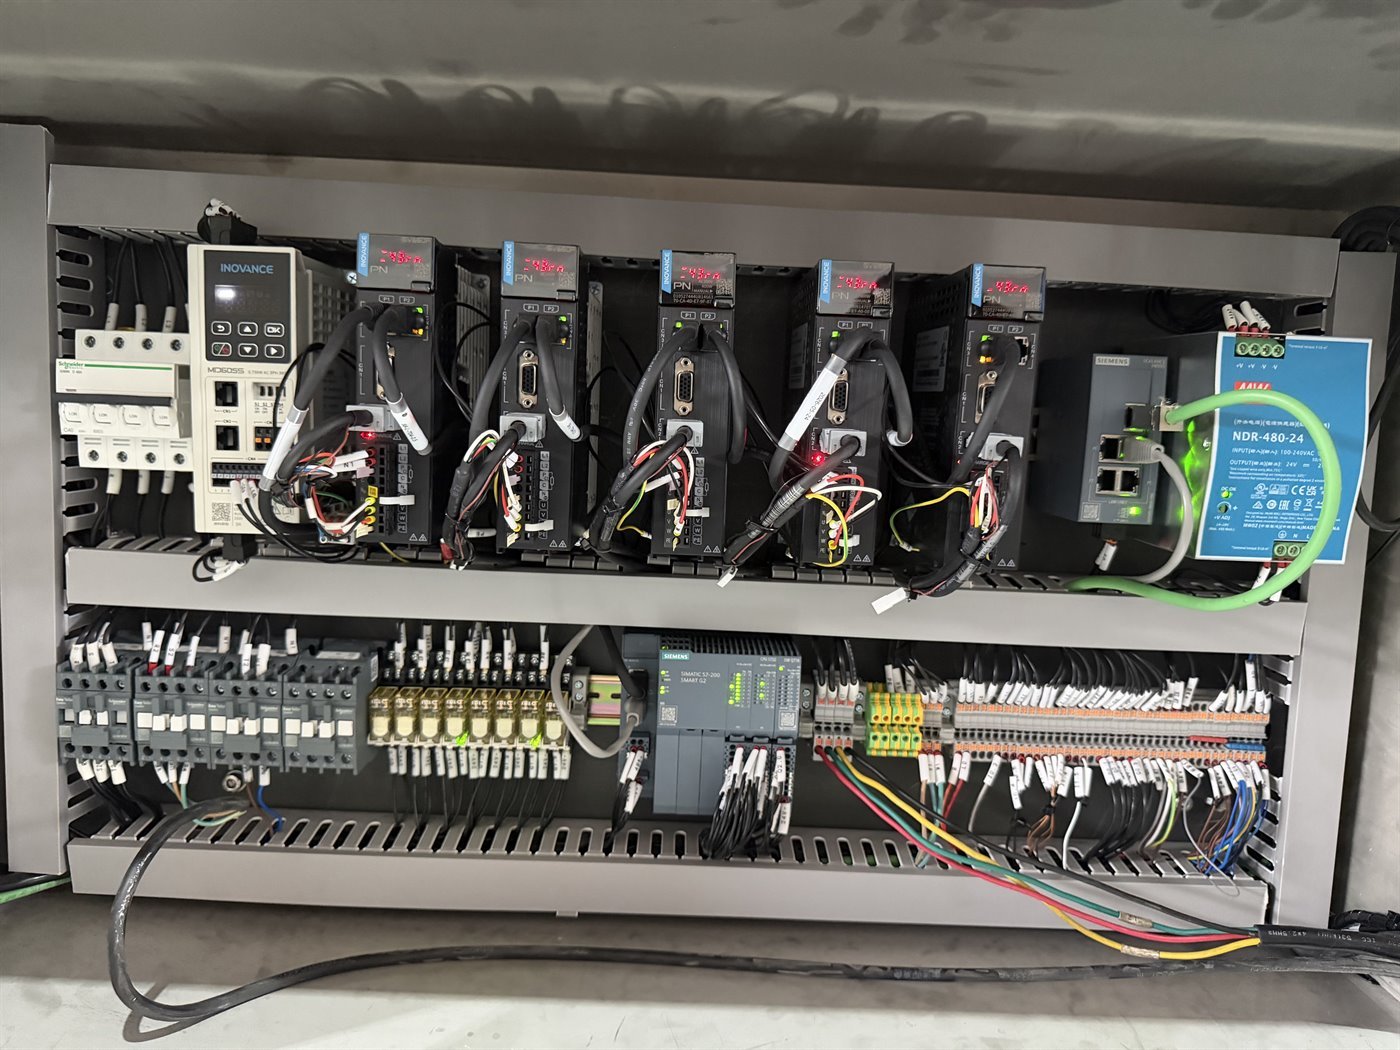
KPGZ-4 Project Reference
Useful starting points—not a substitute for sample trials.
These values come from the supplied production-task specification. Final performance depends on the formula, temperature, bottle and closure set.
Request a configured proposal| Reference fill | 67 g gel / semi-fluid product |
|---|---|
| Dosing system | 4 independent servo-driven 316L piston pumps |
| Temperature range | Ambient to 60°C adjustable (project reference) |
| Output reference | 30–40 bottles/min, subject to trials |
| Fill-volume reference | 20–100 ml offered for the project |
| Machine utilities | 220 V / 50 Hz / approx. 4 kW; air ≥0.5 MPa |
| Structure | SUS304 frame; sanitary quick-release product path |
| Control reference | Siemens PLC/HMI; Inovance servo system |
Accuracy requirements in the source specification vary by test and acceptance stage. A guaranteed value will be stated only after formula and package trials establish the correct operating window.
Acceptance Planning
Prove the result with the real formula and package.
Test protocols should reproduce production viscosity, temperature, bottle handling and closure conditions—not only a water run.
FAT before shipment
The reference plan includes approximately 30 minutes of continuous operation at rated capacity with fill and weight checks. Trial material and production-intent components are recommended.
SAT after installation
Site acceptance verifies operation across the agreed capacity range, repeatability and package quality under the customer’s utilities and production conditions.
Frequently Asked Questions
What needs to be confirmed before line selection?
Can the machine fill different bottle sizes?
Yes. The straight-line platform uses package-specific positioning fixtures. Final compatibility is confirmed from bottle drawings and physical samples, including the bottle’s centre of gravity and neck geometry.
Can each filling head use a different volume?
The four servo piston pumps can be adjusted independently. The viable combination depends on the selected pump range, cycle time and product behaviour.
Is the roll-on fitment and cap applied automatically?
It can be configured as an automated route, but the feeding, insertion and tightening method depends on the actual ball housing, fitment and cap set. Samples are required before the closure modules are finalized.
How is the correct temperature selected?
The project reference allows adjustment from ambient to 60°C. The production setpoint should be determined from viscosity, thermal stability and filling trials rather than selected from the machine limit alone.
What samples should we send?
Please provide the formula or representative trial material, filled and empty bottles, roll-on components, caps, target fill volume, required output and your acceptance criteria.
Configure The Actual Package
Send your veterinary gel, bottle, roll-on fitment and cap samples.
KING PACK will review the product behaviour, temperature window, dosing range and closure geometry before recommending the filling and capping route.