 Skip to content

Introduction
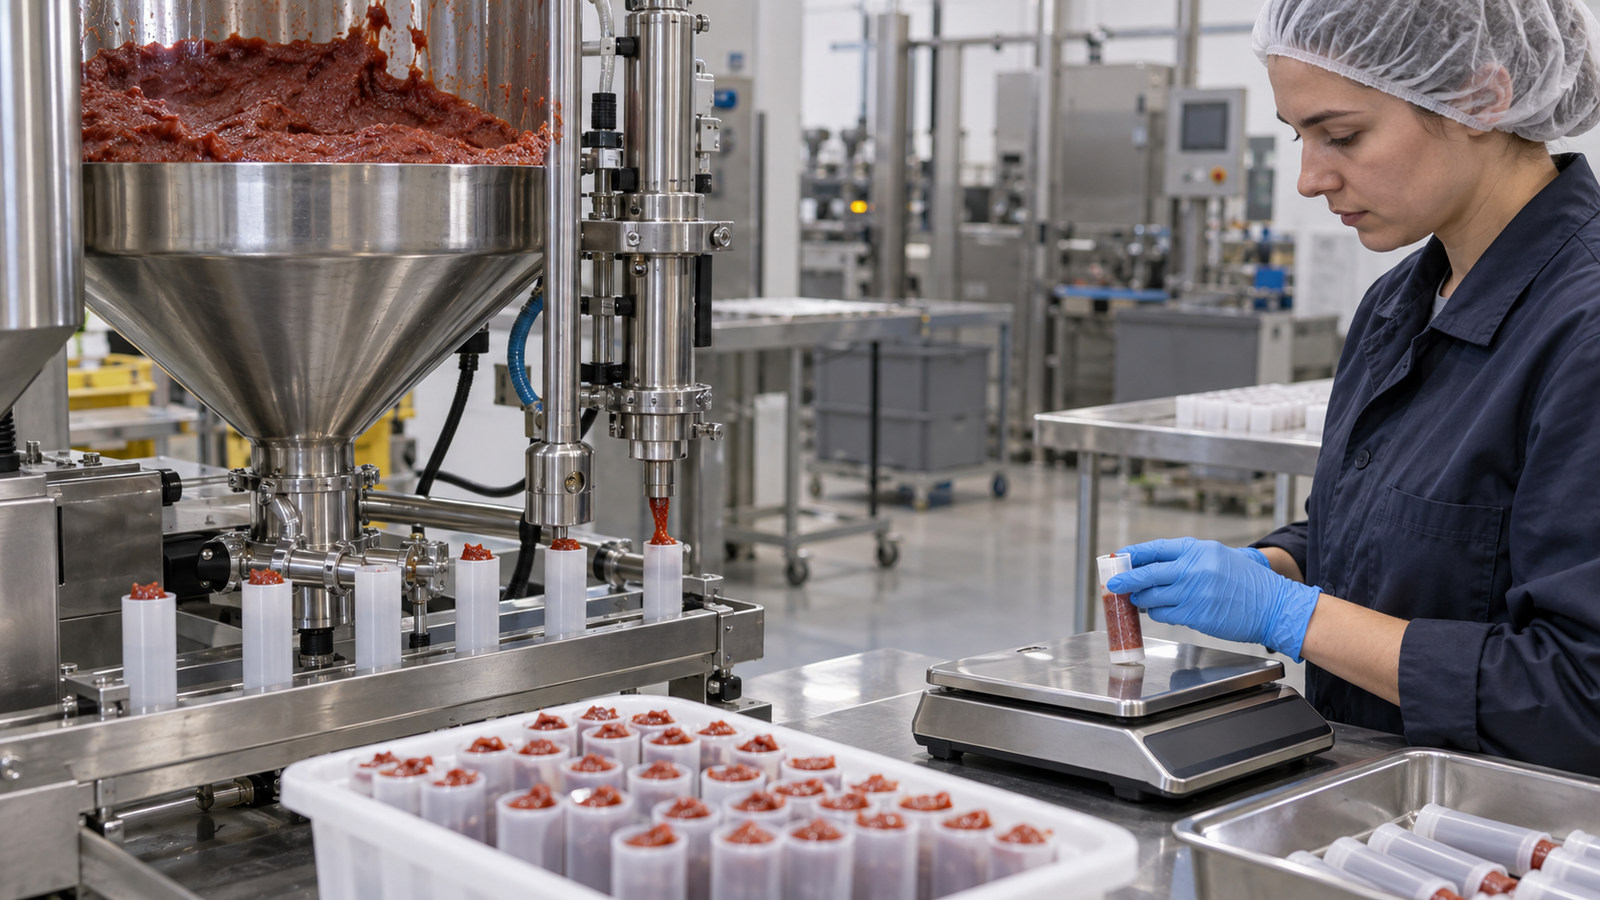
A rodenticide paste filling machine doses soft rat bait paste into syringe-style point-application tubes. It follows the same syringe filling route as insecticide gel bait, yet it has to handle a softer, oilier, and more temperature-sensitive paste. That single difference drives the pump choice, the seals, the cut-off, the feed vessel, and the way net content is held through a shift.
This article looks at what those differences mean on a production floor, drawn from our factory testing and from the sample trials customers run with us before they commit to a line.
One boundary first: this covers filling paste into point-application tubes and tips, not pressed bait blocks, solid bait-station refills, or loose grain bait, which are different products on different machines.
What Counts as Rodenticide Paste, and Where This Machine Fits
Rodenticide paste is a bait matrix, usually built on a fat, oil, or wax base, coloured and often blended with a bittering agent, filled or extruded into a syringe-type applicator. The end user presses the plunger and places measured dots of bait along a run, a wall edge, or inside a bait station. Because the product is sold by mass, net content in grams is the control point, not the barrel's rated volume.
The machine that fills it is a positive-displacement syringe filler, sized for high-viscosity paste. It meters by volume, inserts the piston, closes the tip or cap, checks weight, and rejects out-of-tolerance units. The layout looks familiar to anyone running insecticide gel bait; the material behaviour does not. New to the syringe side? The parts and their names are covered in our guide to selecting gel bait syringes for automated filling.
Where this machine does not apply
If your product form is a pressed block, a coated grain, or a solid bait-station insert, the forming step is moulding or pressing, not paste filling. Specify a paste filling machine only when the bait is soft enough to flow or extrude and the pack is a tube, tip, or syringe barrel. A machine bought for the wrong product form cannot be fixed by tuning settings.
How Rodenticide Paste Differs from Insecticide Gel Bait
The table below is the fastest way to see why we treat these two products separately during a trial.
| Property | Insecticide gel bait (roach / ant) | Rodenticide paste (soft bait) |
|---|---|---|
| Body and texture | Thick paste, often thixotropic; holds a peak | Softer and more spreadable; can slump |
| Common base | Water and gel systems | Fat, oil, or wax based |
| Colour | Pale, amber, or clear | Blue or green in many markets |
| Notable additives | Attractant; some particles or fibres | Bittering agent common; fillers abrasive |
| Temperature response | Thins when warm, firms when cool | Same direction, often more sensitive |
| Oil behaviour | Rarely separates | Oil or fat can separate and bleed |
| Cut-off behaviour | Strings on elastic pastes | Strings and smears more; sticks to surfaces |
| Net-content control | Sold by gram | Sold by gram; density moves with temperature |
Texture, oil, and wax
Insecticide gels vary a lot, but many are thixotropic: they thin when sheared and firm up at rest. Rodenticide pastes are often softer and more oil-rich, and some carry a wax fraction. Soft paste spreads under its own weight, so the dose geometry after filling is less predictable and the pack must hold the material without slumping.
Colour, bittering agents, and cleaning
Many rodenticide pastes are strongly coloured and carry a bittering agent. Neither affects dosing accuracy, but both raise the cleaning bar. Colour and bittern carry into the next batch if the shared parts are not stripped and washed to depth, which matters far more on a multi-product line than a single-product one.
Temperature sensitivity and stringing
Oil and wax systems respond to temperature more than water-based gels do. A paste that cuts cleanly at one temperature can smear at another, and surface oil can bleed into the cap threads. This is the main reason we ask for the filling temperature window before we size a pump.
What These Differences Demand from the Filling Equipment
Soft, oily, temperature-sensitive paste places a few specific demands on hardware. Each one maps to a failure we have seen at a customer site.
Push and feed force
Thicker, stickier paste resists flow, so the feed system has to push harder without shearing the material or letting it bridge in the hopper. A pump sized for a light gel may stall on a heavy oil-based paste. In our experience the answer is a larger feed path and a slower, steadier transfer, not a faster pump.
Seals, O-rings, and wetted parts
Oil, fat, and some active ingredients attack the wrong elastomer. Seals swell, harden, or crumble, and a leaking seal becomes a net-content drift and a contamination problem at once. Wetted parts and seal material have to be chosen for the specific paste, and the customer's SDS is the first document we ask for. The equipment makes no claim about product compliance; that stays with the customer and their market's regulator.
Wear-resistant metering components
Some pastes carry abrasive fillers, minerals, or fibrous material. Those wear the metering element, the nozzle, and the valve seat. Hardened or coated contact parts and a defined inspection interval matter more here than on a smooth gel. Wear shows up first as slow fill drift, not a sudden failure.
A cut-off that actually cuts
Because this paste strings and smears, suck-back (a short reverse stroke), a closing nozzle valve, and lift-and-dispense timing all have to be tuned to the material. A cut-off setting copied from a gel bait job usually leaves a tail, and a tail lands on the tip and the cap threads.
Vessel agitation and heat retention
A fat-based paste separates. Left standing, oil or fat rises to the surface, so the top of the batch fills lighter than the bottom. Gentle, continuous agitation keeps the matrix together. In cooler plants, jacketed or heated vessels hold the paste in its working window. We confirm both needs during installation preparation, because they are hard to retrofit later.
Paste behaving badly on your own line right now? Send us your paste, tube, and closure details, and we will point to the likely cause and the fix that fits your setup. An engineer replies, no pressure.
Temperature, Flow, and Net-Content Consistency
Net content in a syringe is the mass of paste in grams, and the rated barrel volume is not that mass. For a temperature-sensitive paste, the link between what the pump displaces and what the scale reads moves with temperature, because density does. Warmer paste is thinner and less dense, so the same volume weighs a little less. Cooler paste stiffens and may not fill the tip, which shows as a short fill or an air pocket. Neither is a machine fault; both are conditions the line has to hold.
How we verify it at the sample trial
We do not trust a single reading. At the trial we:
- Run the actual paste at the low end, the middle, and the high end of the customer's temperature window.
- Weigh a set of units at each point, using the same scale and the same tare procedure throughout.
- Watch the cut-off at each temperature, because stringing changes before the weight does.
- Check the pack surface for oil bleed after a short rest, since that is a shipping risk, not a filling risk.
The goal is a temperature window, not a single number. If the plant cannot hold that window, the paste may need reformulating or the vessel may need heating or cooling. Both are cheaper to find in the trial than in production.
Front Filling or Rear Filling for Soft Paste
Route choice matters more with soft paste than with a firm gel. Front filling doses through the tip with a narrow nozzle and higher pressure; rear filling doses through the open tail and inserts the piston after dosing, which is simpler for sticky material but adds a venting step. We pick the route from the customer's pack, not habit.
Packaging Formats and Sealing
Paste for rodent control ships in a few pack shapes, and each one changes the line.
Single-tube and multi-tube formats
Some products ship as single tubes, with or without a plunger. Others are multi-tube cards, where several smaller tubes share one applicator or run in sequence. Multi-tube packs add an assembly step before the tubes reach the filler, so confirm the format early.
Tip, cap, and seal
The closure can be a separate cap, an attached tip, or a tip-and-cap combination. Each has its own sealing surface and its own press or torque value. For an oily paste the cap seal is the weak point: surface oil, a smeared tip, or an over-tight cap all lead to leaks.
Leak and transit checks before shipment
Before the line ships we run the sealing setup against the customer's own tube and cap. At shipment inspection we also check the packing method: tubes upright, layers supported, no load sitting on the closure. A cap that seals in the plant still leaks if the carton is stacked so the tubes lie on their side. We have opened returned cartons where the leak traced to orientation, not the cap.
Many plants run rodenticide paste and insecticide gel bait on the same filler to spread the capital cost. That is workable if the cleaning and isolation rules are set up first.
- Sequence the run so the strongest colour and the strongest odour go last, or plan a full teardown between products.
- Strip and wash every wetted part, not just the vessel, because colour and bittern sit in the pump head, the nozzle, the valve, and the feed line.
- Check the nozzle and the valve seat by hand, since a smear inside the valve body is easy to miss and shows up as a coloured fleck in the next batch.
- Keep retention samples if the customer runs their own check between campaigns.
The isolation scope depends on the customer's product, their market rules, and their own quality system. We set the cleaning depth with them during the trial, not after the first complaint.
Material Handling and Operator Protection
Rodenticide paste is handled according to its SDS and the rules of the market where it is made and sold. The machine itself makes no safety or compliance claim. In hardware terms we look at sealed transfer of paste from drum to vessel to cut operator contact, a vessel that can be closed during agitation, and easy access for cleaning so residues do not build up in corners.
Rooms are usually kept ventilated, and operators follow the PPE their own risk assessment and local rules require. None of that is decided by the filling machine. Safety and registration questions belong with the customer's own regulatory team, not the equipment supplier.
Trial and Acceptance: What We Look At First
A sample trial is the cheapest place to find a mismatch, and where most of the real answers come from. We run paste jobs the same way as gel bait, and the checklist in our sample trial guide for buyers is a good place to start before you ship anything to a supplier.
When a customer's sample arrives
When a paste sample reaches us, we look at four things before we touch a setting:
- How the paste behaves at rest. Does oil sit on the surface? Does it hold a peak or slump?
- How it behaves under shear. Some pastes thin and stay thin; others recover fast. That decides the pump family.
- How it cuts. We dose a few shots manually and watch the tail.
- What is in it. Fillers, fibres, and abrasive minerals change the metering part and the wear interval.
Then we run it on the actual barrel, piston, tip, and cap the customer will use. A good result on our lab tube and a poor result on theirs is a common outcome, which is why we ask for their pack.
Acceptance points to agree in advance
| Check | What we record | Why it matters |
|---|---|---|
| Net-content tolerance | Target grams, actual weights, method, sampling plan | The label and the market rule are set on mass |
| Cut-off and tip condition | Tail length, tip cleanliness after several cycles | A dirty tip becomes a leaking cap |
| Continuous run stability | Weights and defects across a set run time | Shows drift, not just a good first shot |
| Cleaning time | Minutes to strip and wash the wetted path | Sets the real changeover cost |
| Changeover time | Minutes between formats or products | Decides the multi-spec economics |
Agree the measurement method, the sampling plan, and the defect definitions before the line ships, so the factory acceptance test runs against numbers everyone signed. That step prevents most disputes, because it settles what "good" means before anyone is under shipping pressure.
FAQ
Q: What is a rodenticide paste filling machine used for?
It fills soft rat bait paste into syringe-style point-application tubes. The machine meters the paste by volume, inserts the piston, closes the tip or cap, and checks net content. It suits any bait matrix that flows or extrudes. It is not used for pressed blocks, coated grain, or solid bait-station inserts, which are formed rather than filled.
Q: Can I run rodenticide paste and insecticide gel bait on the same machine?
Often yes, with a defined cleaning and isolation scope. Rodenticide paste adds colour and a bittering agent that carry into the next batch if the wetted path is not stripped to depth. Strong colour and odour products usually run last. The exact isolation level depends on the customer's product and their market rules.
Q: Why does my net content drift over a shift?
Temperature is the usual cause. An oil-based paste changes density and flow as it warms or cools, so the same displaced volume can weigh differently later in the shift. Confirm the filling temperature window, hold the paste inside it with vessel heating or cooling, and weigh at set intervals using the same method each time.
Q: Why does oil separate in my feed vessel?
Fat and oil systems separate when they stand still. Left alone, oil rises and the top of the batch fills lighter than the bottom, so weight drifts without any change to the setting. Gentle, continuous agitation keeps the matrix mixed. A closed vessel also limits skinning at the surface and keeps the paste cleaner.
Q: What should I test before buying a rodenticide paste filling machine?
Run the real paste, barrel, piston, tip, and cap. Test at the low, middle, and high ends of your temperature window. Record net-content weights with a fixed method and sampling plan, watch the cut-off, check for oil bleed on the pack, and time the cleaning and changeover. Agree factory acceptance criteria before the line ships.
Conclusion
Rodenticide paste is not the same job as insecticide gel bait, even though both run through a syringe filler. The paste is softer, more oil-rich, and more temperature-sensitive, and those traits drive the feed force, the seals, the metering wear parts, the cut-off, and the vessel's agitation and heat. Net content is a mass figure that moves with temperature, so the line has to hold a window, not a single setting.
The practical route is the one we recommend for any paste: run the real product and the real pack in a sample trial, test across the temperature window, agree the acceptance numbers before the line ships, and set the cleaning scope during the trial, not after a complaint. Handle the paste per its SDS and the rules of its market; the machine decides none of that.
Get a Quote
Tell us what paste you run and what pack it goes into. Send your tube, piston, tip, and cap samples, the SDS, viscosity and density data at your filling temperature, and your net-content target in grams, and we will propose the metering principle and the line layout that fits. An engineer will reply.
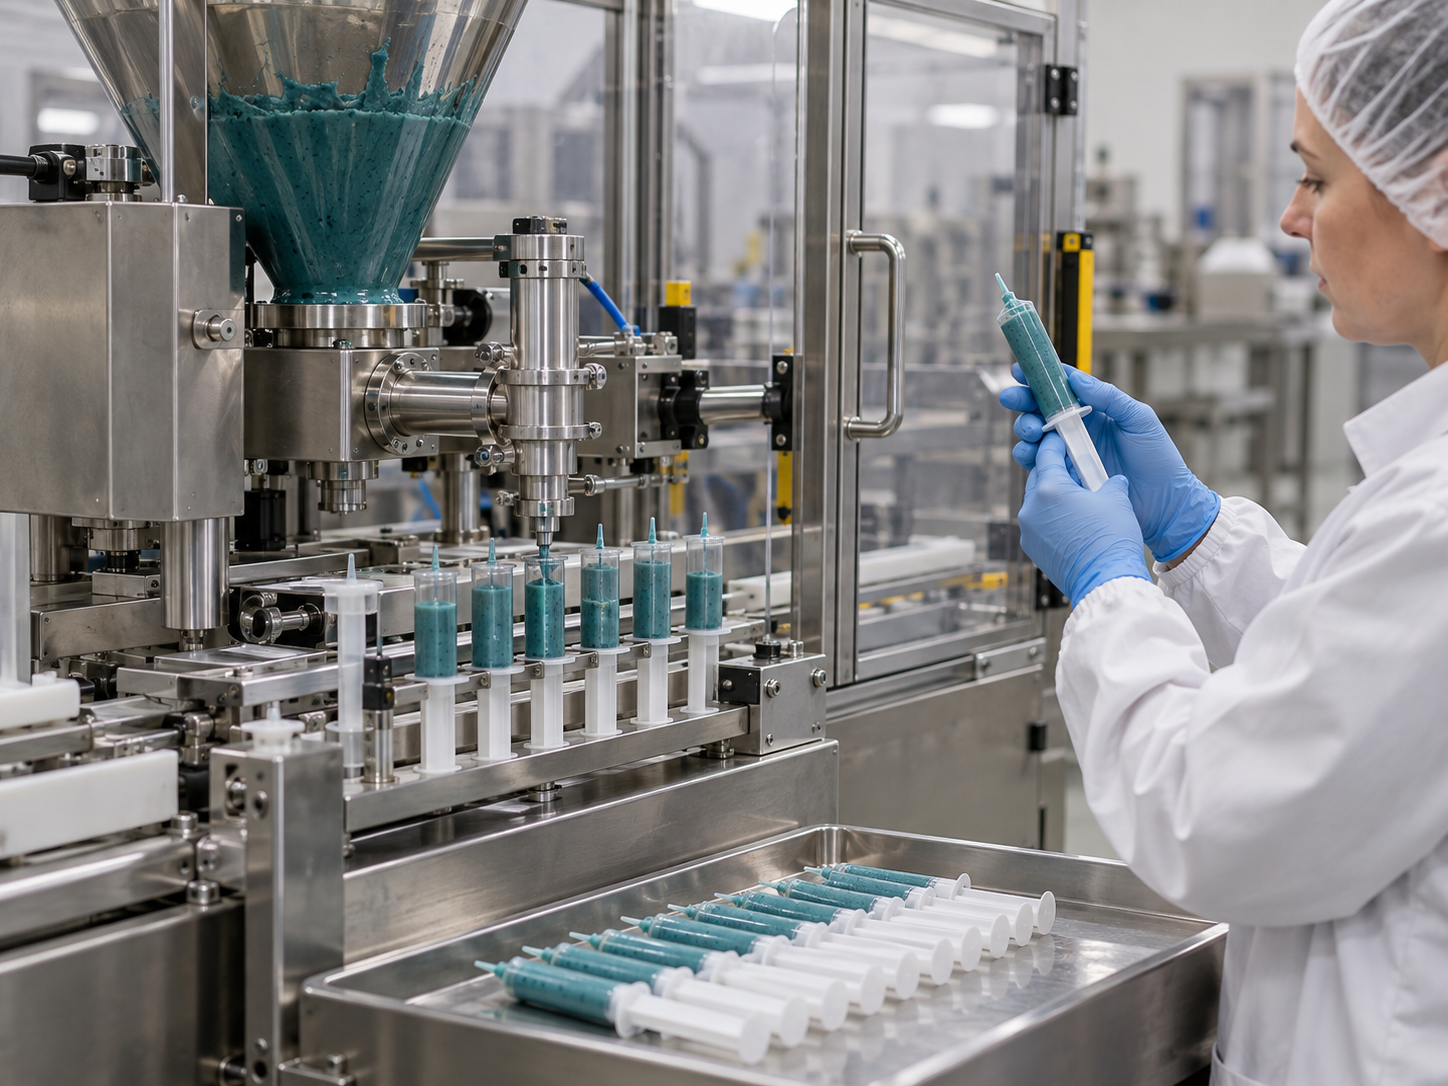
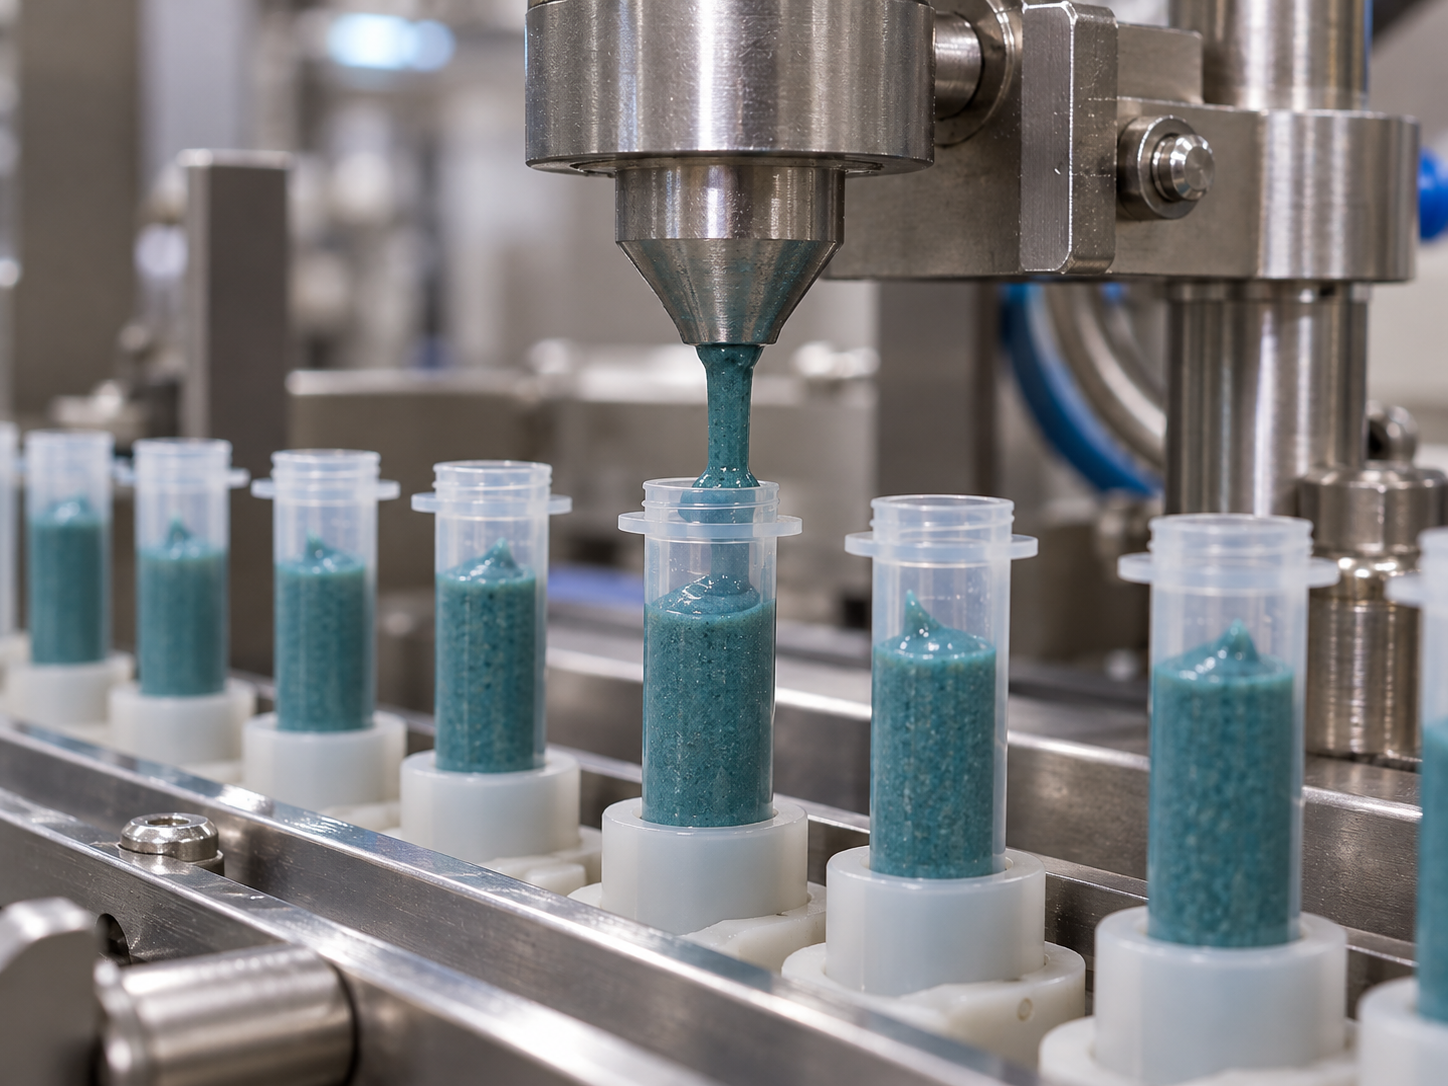
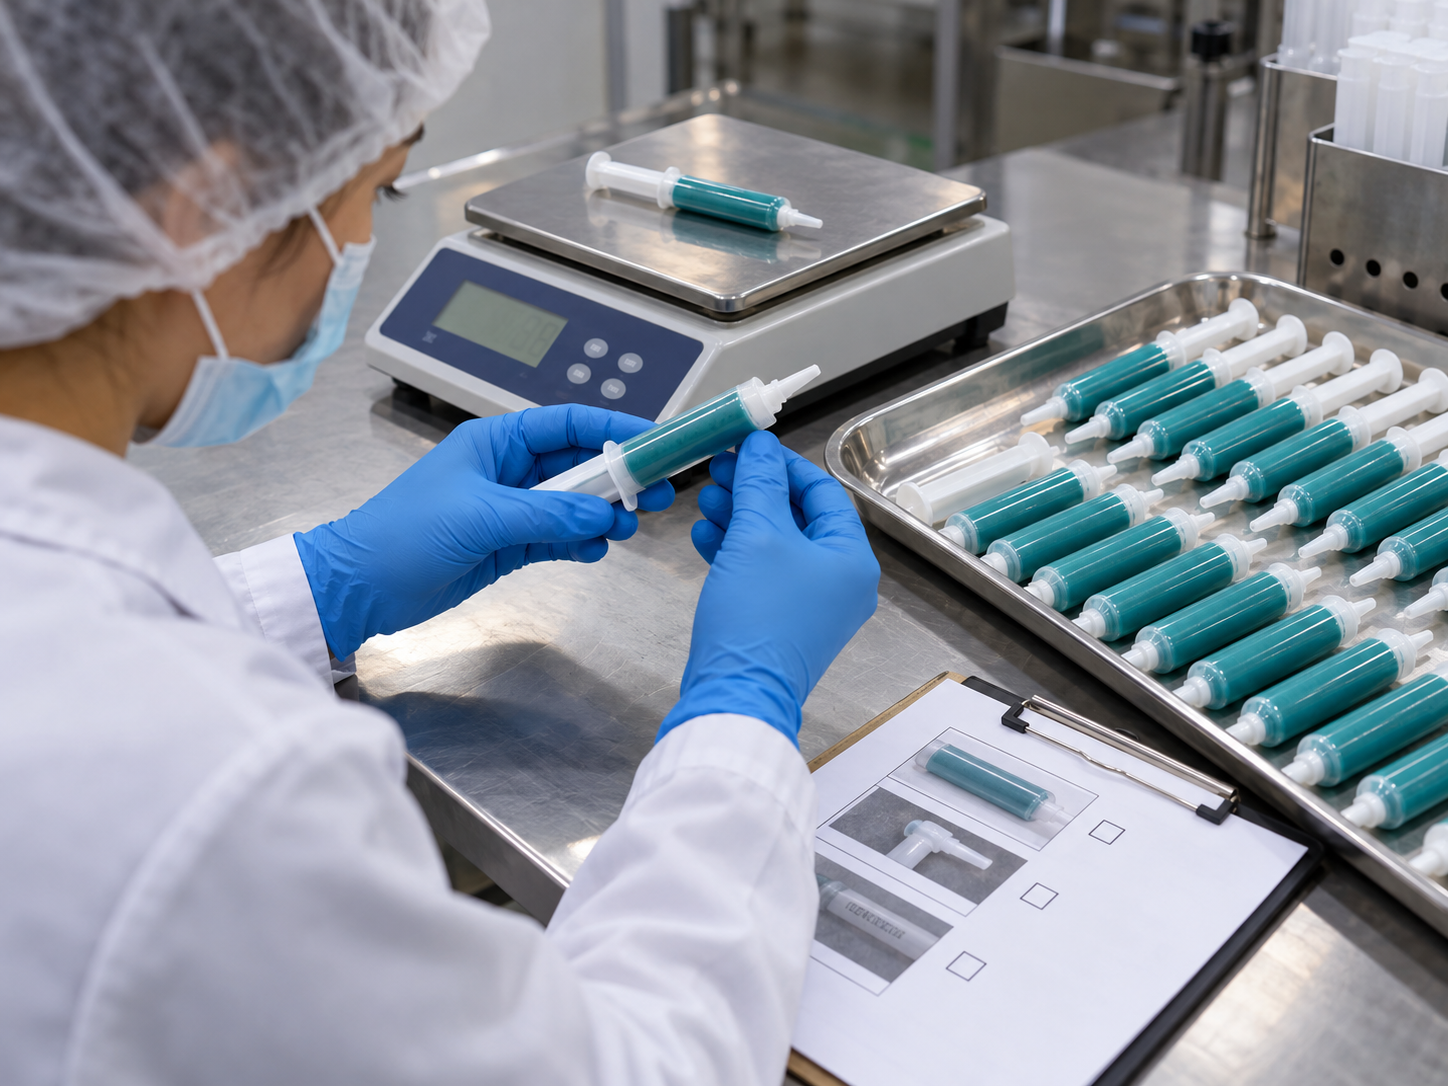
The following visuals are illustrative production and inspection references. They do not represent guaranteed output or measured validation results.
Related equipment and project resources
For equipment selection, compare the relevant filling machine product range with the packaging solution overview. Application context is available in the veterinary medicine solutions and pharmaceutical packaging guide. Where the process includes a closure step, review the filling and capping line and tube sealing equipment.
Before a trial, document product rheology, fill volume, container dimensions, contact materials, cleaning method, closure requirements and inspection points. Related planning resources include tube filling and sealing machine selection, how to choose a tube filling machine, tube sealing quality control, manual to automatic syringe filling and syringe format changeover planning.
For a project-specific review, contact the technical team, send your requirements for a quote or review the syringe filling machine range. Include samples or drawings when available so the machine scope can be assessed against real product and packaging conditions.
Need help with the next step? Request a quote with the product, package, fill volume and target checks.
