
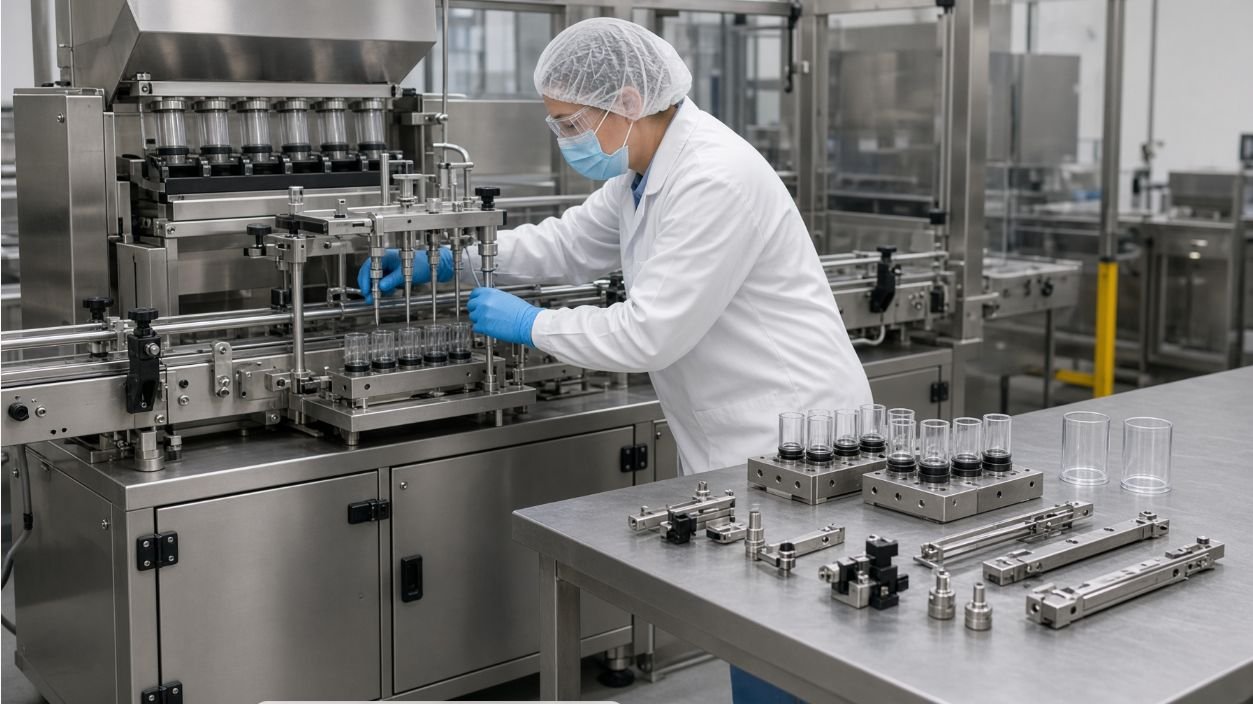
Running two or three gel bait syringe sizes on one line is not unusual—an OEM/private-label producer may fill a 30 g standard cartridge in the morning and a 10 g consumer syringe in the afternoon, while a regional brand runs both a cockroach and an ant bait across the same barrel geometry. The technical question is whether the line was designed to change between those formats without dismantling the dosing head or rebuilding the conveyor. Most gel bait syringe filling lines are sold as a single configuration, then expected to cover multiple sizes later, and the gap between the two is where changeover time, scrap and first-batch defects are paid for in production.
This article walks through how to group formats that can actually share a line, what must physically change when formats are switched, where to pre-stage change parts and settings, and how to record and verify a changeover so it stops being a recurring production risk.
Group Formats by Geometry and Dose Before Anything Else
The first planning question is not “what changes” but “what is shared.” Two nominal sizes of gel bait syringe can be different in ways that make a quick change impossible, or can be near-identical in ways that a fixture swap handles in minutes. Grouping formats before the line is built or expanded is where changeover becomes either a controlled activity or a recurring source of error.
The grouping dimensions that matter:
- Barrel outer diameter and length. Drives the conveyor width, the star-wheel pitch, the nozzle reach and the indexing station geometry.
- Tip / nozzle interface. A 4 mm tip, a 5 mm tip and a Luer-style tip need different nozzle holders and cut-off settings even on the same barrel length.
- Closure style. A screw cap, a press-fit tip cap and a crimped cap each require their own placement and retention station.
- Piston / plunger supply state. Pre-inserted pistons, loose pistons dropped on the line, and plunger rods assembled post-fill change the number of stations involved.
- Dose volume. A 1 g monodose and a 30 g bulk-fill syringe sit at opposite ends of the dosing-stroke range for the same metering element and may not be reachable by the same pump.
Formats that share all five items can usually run with a fixture exchange and a recipe change. Formats that disagree on three or more of these items need a different conversation, possibly a dedicated line. The mistake most often seen is treating two “30 g” syringes from different suppliers as the same format because the label looks similar; the actual barrels, flanges and tips may not be compatible with the same change parts.
Identify the Change Parts on the Feeding and Positioning Side
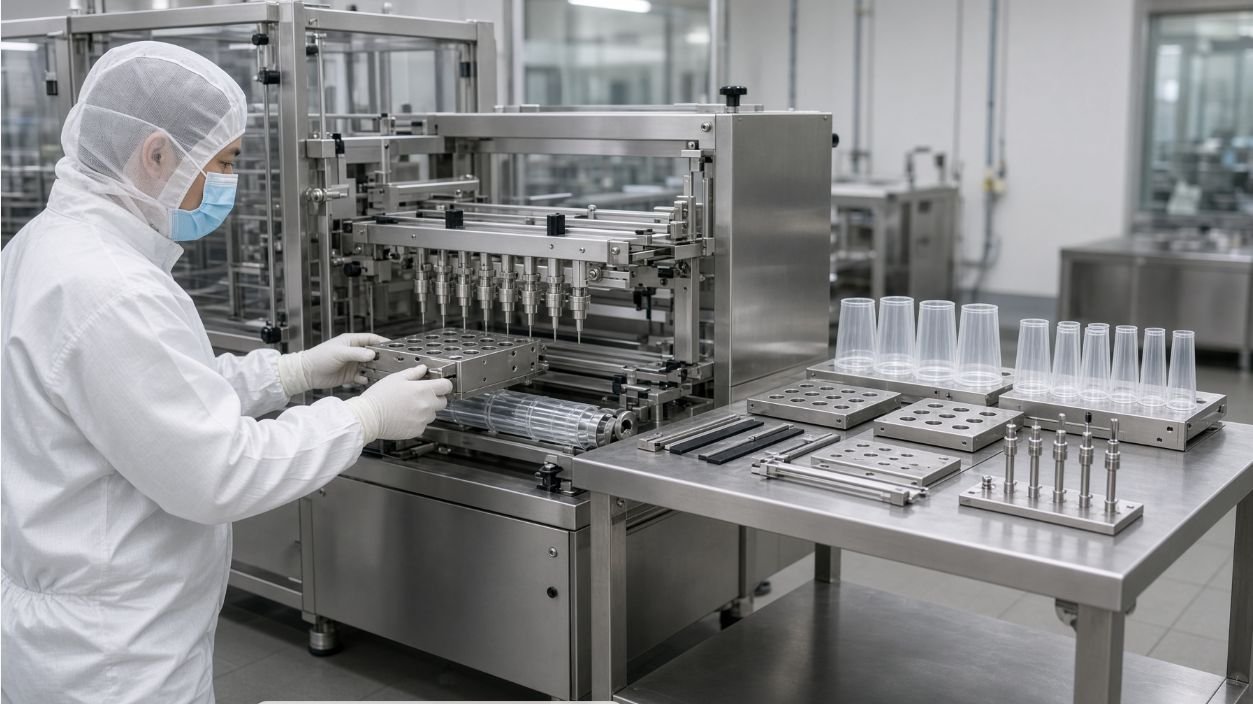
Once formats are grouped, the physical change parts fall into two halves of the line: feeding/positioning and dosing/assembly. Each half carries its own change parts and its own change time, and they are rarely equal. Mapping them on paper before any change happens is what lets the changeover go from a 90-minute unplanned stop into a recorded 20-minute procedure.
Feeding and positioning parts typically include:
- Bulk hopper or tray. A hopper sized for one barrel length may need a removable insert or an exchangeable tray to keep loose or pre-oriented syringes feeding correctly.
- Bulk conveyor and pre-orientation rails. Width, rail spacing and any orientation features are barrel-diameter-dependent.
- Syringe nests, carriers or star wheels. These hold the barrel at the dosing point and set the indexing pitch. A change of pitch is one of the costliest items to change on a line because it propagates through the conveyor.
- Centring and register fixtures. The fixtures that align the barrel under the nozzle are barrel-specific; even a 2 mm barrel-length difference is enough to push the alignment out of tolerance.
- Closure feeders and tracks. A cap feeder bowl, cap track and cap-application chuck each carry sized parts for one closure style and one closure orientation.
A useful exercise for a new line is to mark, on the layout drawing, every part that physically moves when the format changes. Anything that is removed and replaced is a candidate change part; anything that is adjusted but not replaced is a setting. The line should be designed so that change parts are organised, labelled and pre-staged before the changeover starts, not hunted for during it.
Decide What Must Move on the Dosing and Assembly Side
Dosing and assembly is the other half of the changeover, and it is where most of the settings live. The principle is the same: replace what does not change between formats, and adjust what does. The danger is over-adjusting—turning screws that were correctly set for the previous format—because an operator is trying to chase a defect rather than executing a planned sequence.
Typical change parts and adjustments on the dosing and assembly side:
- Dosing nozzle and nozzle holder. Change parts; or, if the same nozzle is reused, a clean reset of the cut-off distance and the suck-back distance.
- Piston insertion station. Insertion depth, insertion speed and any venting fixture are settings; the piston bowl or feed track is a change part when the piston diameter changes.
- Closure placement and retention. Chuck or head exchange for closure style; cap torque or press-fit force as a recipe parameter.
- Inspection and rejection stations. Vision and weight-check recipes are format-specific and must be selected, not edited in place, at changeover.
- Coding, labelling and serial-number patterns. These are recipe-level changes but are easy to forget and should be on the changeover sheet.
The right ordering is usually: mechanical change parts first, recipe change second, first-off checks third. Doing it in any other order tends to introduce wasted units caused by stale recipes running on a freshly re-fixtured line, or freshly set recipes running on the previous format’s fixtures.
Build the First-Off Check Around the New Format, Not the Old One
First-off checks are the safety net at the end of every changeover, and they are usually designed around the format that was running most often. That is a problem: the format being started is the one most likely to expose setting errors, and the checks should be weighted towards it. A first-off check that only confirms “the line is running” is not a check; it is a confirmation that power is on.
Useful first-off checks after a format change:
- Barrel placement. The barrel sits fully home in the nest with the flange registered and the tip under the nozzle path, on a sample of at least five units before the run starts.
- Fill weight across a short window. Weigh N consecutive units against the agreed target and tolerance, and keep them aside until the trend is stable.
- Piston seat and closure quality. Inspect the inserted piston and the applied closure on the same short sample; reject any unit with a visible gap, twist, or unsealed cap.
- Cycle time vs. expected. Confirm that cycle time matches the recipe’s expected value; a slower cycle usually means a fixture is dragging, a faster one usually means a sensor has stopped seeing the part.
- Coding and label application. Verify the print or label against the new format’s artwork and codes on the same short sample.
Only when those five are recorded and accepted should the line go into full-rate production. Until then, every unit is a possible first-batch defect.
Record and Verify the Changeover So It Becomes Repeatable
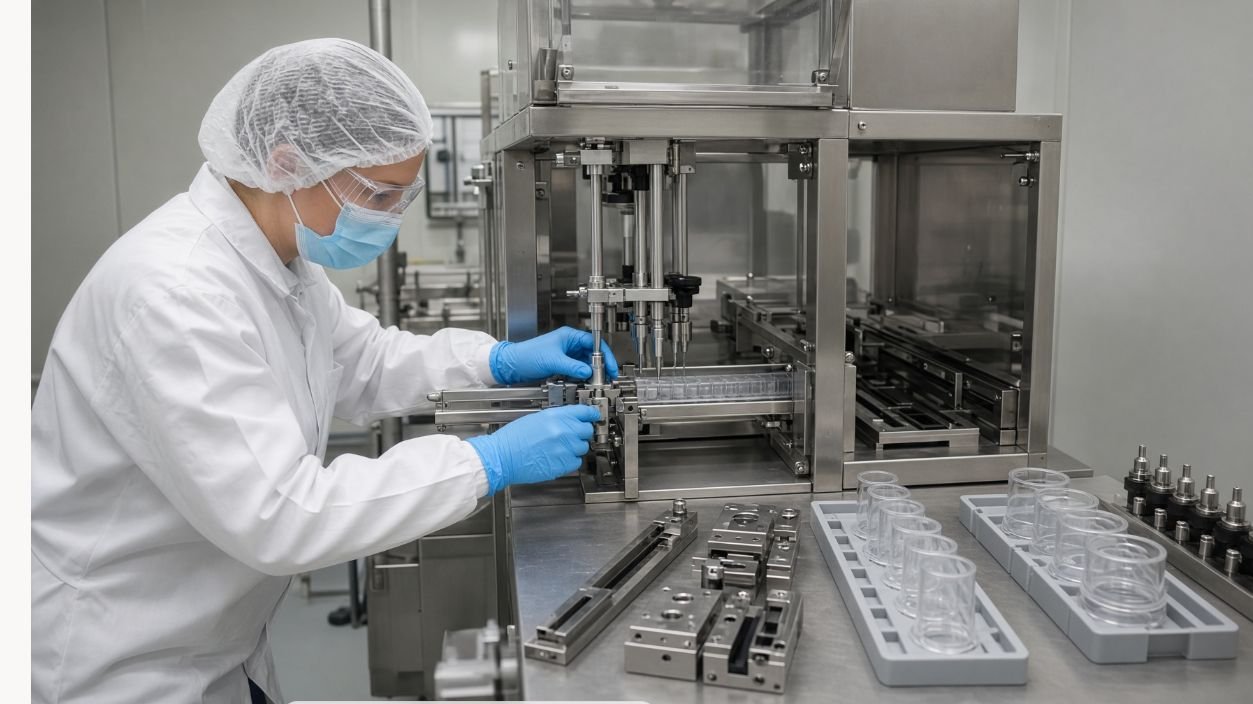
A changeover that is not recorded is a changeover that has to be reinvented the next time. The format of the record matters less than the consistency: every changeover for the same line should produce the same kind of record, so that the next operator, the next shift and the next audit can read what happened and act on it.
Minimum items the changeover record should carry:
- The format being left and the format being started, with batch/lot of product and packaging on each side.
- The change parts used, identified by part number and serial, so that wear and breakage can be traced.
- The recipe or settings loaded, with version, against the recipe of the previous format.
- The first-off check results, with the values recorded, not summarised.
- The time from line stop to first accepted unit, and the scrap count during the changeover window.
- Any deviation or abnormality, with the action taken and the person responsible.
Two operational rules make the record useful. First, the changeover time on the record should match the agreed target; if it does not, the gap is a project input, not a failure to apologise for. Second, the first batch after the changeover should be flagged on the production traveller so that downstream operations handle it with the same care as the first batch after a tool change.
Common Risks and Mistakes
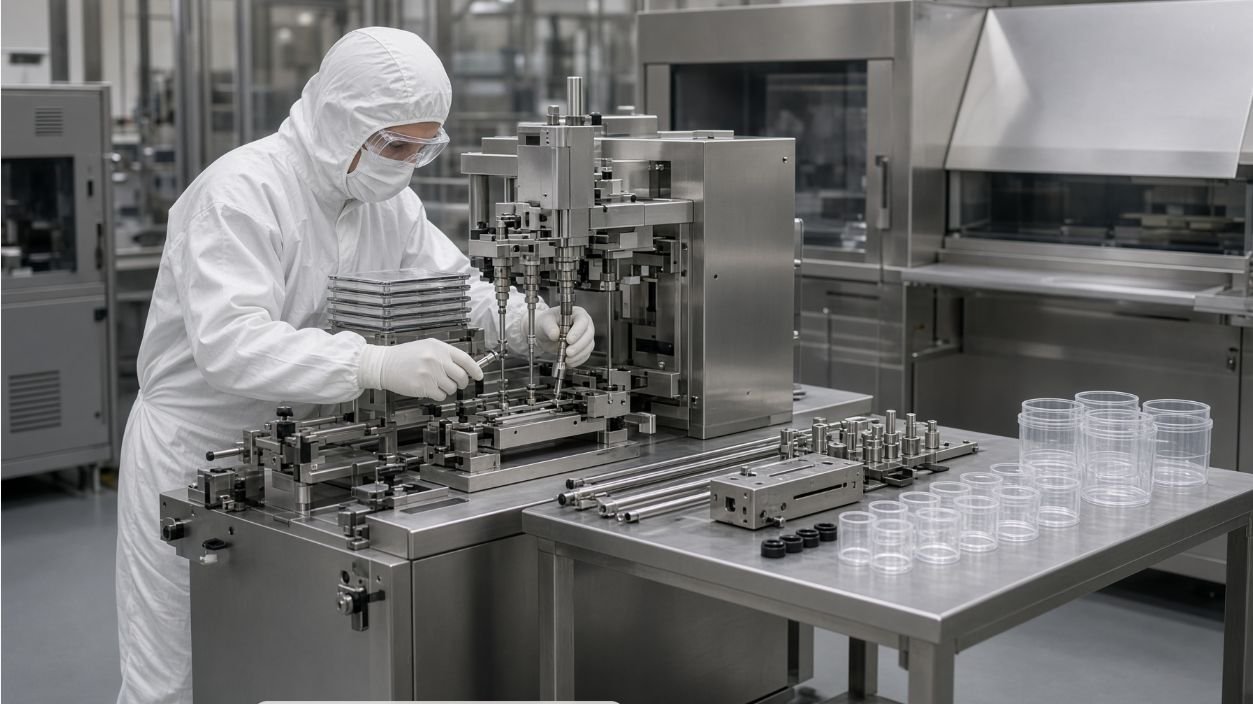
- Grouping formats by label, not by geometry. Two “30 g” syringes from different suppliers can disagree on enough dimensions to require full re-fixturing, not just recipe loading.
- Sharing dosing elements across formats that sit at opposite ends of the dose range. A pump sized for 30 g is rarely the right pump for 1 g; the stroke, suck-back and resolution are not interchangeable.
- Forgetting the coding and inspection recipes. The mechanical line is sometimes ready but the inspection and coding are still on the previous format’s recipe; the first units out of the station can pass into the market with the wrong batch code.
- Treating first-off checks as a formality. Checks weighted towards the previously running format miss the defects the new format is most likely to produce.
- No pre-staging of change parts. An operator hunting for the right fixture between format changes converts a 20-minute changeover into a 90-minute unplanned stop.
- No record of which parts were used. Without a record, wear and breakage cannot be traced, and the next changeover repeats the same improvisation.
How King Pack Supports This Application
King Pack Machinery (Wuxi King-Pack / Wuxi Jingpai Machinery Co., Ltd., founded 2009, with a core technical team carrying more than 20 years of industry experience) supports gel bait syringe format changeover as a configured capability of the line, not as an afterthought added on after installation. The relevant support is:
- Format-grouping review before quotation. King Pack reviews the buyer’s full syringe range and identifies which formats can share change parts and which need separate lines, before any equipment specification is fixed.
- Change parts organised and pre-staged. When a line is sold with multi-format capability, the change parts for each supported format are supplied labelled and organised so they can be pre-staged before the changeover window.
- Recipe management and version control. Filling, dosing, inspection and coding recipes are stored and loaded by format code, so the changeover loads a known recipe rather than editing one in place.
- First-off check protocol support. A draft first-off check protocol aligned to the agreed formats is provided with the line; deviations from the protocol are recorded against owners and dates, consistent with the FAT record set described in the acceptance test checklist.
King Pack does not present changeover time as a marketing figure. Changeover time is a project outcome that depends on the formats, the change parts agreed, the recipes loaded and the operators running the line. That outcome should travel with the line in the form of an executed record, not a brochure claim.
Conclusion
A gel bait syringe filling line handles multiple formats well only when changeover is treated as a configured capability, not a recurring production surprise. The work is done before the format change starts: grouping, change-part identification, recipe management, first-off checks and a written record. When those are in place, a changeover is a controlled transition between formats. When they are not, every changeover is a small, repeated training session in the buyer’s most expensive shift.
Ready to plan changeover for your formats? Send the full syringe range with drawings, the planned batch schedule between formats, and the inspection and coding requirements, and request a changeover plan and protocol.