
How to Validate an Intramammary Syringe Filling Line
AI Answer Snapshot
Validation of an intramammary syringe filling line should connect the customer requirement, machine configuration, product, syringe components, filling process, plunger or cap assembly and inspection method. A practical qualification path normally separates design and installation evidence from operating checks and product-performance evidence. IQ, OQ and PQ should be planned around defined risks, representative materials and approved acceptance criteria; factory testing can provide useful evidence, but it does not replace the customer’s site-specific validation.
Introduction
An intramammary syringe line is validated as a process system, not as an isolated filler. The dosing pump, syringe nest, nozzle, plunger insertion, cap handling, coding and reject logic all influence the finished applicator. A qualification package is useful only when it shows what was tested, under which conditions, against which acceptance criteria and with what result.
This guide is for engineering, quality, production and procurement teams preparing an intramammary syringe project. It explains how to define the validation boundary, prepare the URS, organize FAT and SAT, and separate supplier evidence from customer responsibility. It avoids universal claims about accuracy, speed or sterility because those values depend on the product, package and approved test method.
1. Define the validation boundary
Start by listing the process steps included in the project: component loading, syringe positioning, filling, nozzle withdrawal, plunger insertion, cap or tip closure, coding, inspection, rejection and discharge. State which steps are supplied by the machine vendor and which are performed by another system or by the customer. The boundary should also identify utilities, software, recipes, change parts, cleaning and data records.
For an intramammary applicator, include the syringe barrel, plunger, seal, cap, tip and any printed or molded orientation features. A drawing provides nominal dimensions, while production samples reveal friction, tolerance and surface condition. Validation planning should use representative components whenever practical.
2. Translate the URS into testable requirements
A strong URS does not simply say that the line must be reliable or accurate. It describes the intended product, fill volume or mass, format range, operating conditions, inspection method, reject behavior, cleaning access, documentation and training. Each requirement should have a proposed verification method such as document review, visual inspection, functional test or product trial.
Useful URS questions
Ask how the machine detects a missing syringe, absent plunger, wrong orientation or incomplete closure. Ask how recipes are protected, how change parts are identified and how an operator clears a jam. Define the record needed for start-up, restart, first-article approval and rejected units. These questions create a traceable link between the customer need and the qualification protocol.
3. Plan design and configuration review
Before IQ, review the selected dosing principle, product-contact materials, syringe support, nozzle design, plunger or cap sequence, guarding, controls and utility assumptions. Check that the approved configuration matches the drawings and samples used for the quotation. If the product is a viscous paste, note how temperature, air, stringing and cutoff are addressed. If the package is sensitive, document how the nest and transfer avoid damage.
Design review is also the point to identify evidence boundaries. A supplier may confirm that a station can be configured for a format, while a product trial is still needed to prove the result with the customer material. Record open items rather than converting a conditional recommendation into a guaranteed claim.
4. IQ: verify installation and supplied configuration
Installation qualification checks whether the delivered line is installed according to the approved design. Typical evidence includes equipment identification, machine layout, utilities, safety devices, software version, drawings, manuals, spare parts, calibration status where applicable and the list of product-contact components.
For a syringe line, compare nests, nozzles, hoses, valves, plunger tooling and cap tooling with the approved bill of materials. Confirm that the site has the required compressed air, electrical supply, access, drainage or collection method and environmental conditions. IQ should also confirm that operators and maintenance staff have the correct instructions before functional testing begins.
5. OQ: challenge operating ranges and controls
Operational qualification tests the machine functions across agreed operating conditions. The protocol may include recipe selection, start-up, stop, restart, speed or motion settings, missing-component detection, reject logic, alarms, interlocks, changeover and data records. The exact ranges should be justified by the process and not invented simply to make a protocol look complete.
For dosing, define the fill verification method and sample plan. For plunger insertion, inspect seating, visible air, product displacement and barrel damage. For capping, inspect fit, orientation and closure condition. A controlled challenge is more valuable than a vague statement that the machine ran successfully.
6. PQ: prove the process with representative product
Performance qualification evaluates the complete process using representative product, packaging, operators and production conditions. Define the batch or campaign conditions, sample locations, sample size, inspection method, acceptance criteria and handling of deviations before the run starts.
Include start-up samples, stable-run samples, samples after a planned pause and samples after refill or changeover when those events are relevant. Record product preparation, temperature, viscosity behavior, component lot and recipe. If a substitute material is used, label its limitations; substitute material can demonstrate movement but cannot prove the final product process.
7. FAT and SAT evidence
FAT is a supplier-site opportunity to test the approved configuration before shipment. It should use the customer’s syringe, plunger, cap and product whenever practical. Review the protocol before the test and identify which results are pass, conditional pass or open action. Record machine configuration, tooling, recipe and operator intervention.
SAT confirms installation and operation at the customer site. Site utilities, operator training, environment and downstream interfaces can change the result. A successful FAT supports confidence and reduces risk, but SAT and PQ remain necessary when the site conditions or product process differ.
8. Cleaning and changeover validation considerations
Map product-contact parts and nearby risk surfaces before validation. Include dosing passages, valves, gaskets, nozzles, nests, tip supports and any place where residue can migrate. The customer should approve the cleaning chemistry, method, hold time and verification criteria. The supplier can provide access information and removable-part details, but the final cleaning validation belongs to the product owner.
For multiple syringe formats, verify that format parts are identified and that the first article after changeover is inspected before release. A validation package should make clear which recipe, tooling and component lot were used for each test.
9. Manage deviations and evidence
A deviation should describe the observation, condition, immediate action, impact assessment and required follow-up. Avoid changing multiple settings without recording the reason. When an acceptance result is missed, determine whether the cause is product preparation, component variation, tooling, machine setting, inspection method or operator intervention.
The final report should link each requirement to evidence. Include approved protocols, executed records, drawings, calibration or inspection records, training records, deviations, corrective actions and release approval. This makes the qualification package useful during later change control and troubleshooting.
10. What to request from a supplier
Ask the supplier to provide the proposed validation boundary, URS traceability matrix, FAT protocol, sample requirements, machine configuration, product-contact list, utility requirements, manuals, training scope and documentation index. Ask which claims are confirmed by existing evidence and which require a customer sample trial.
King Pack can review the syringe, product, plunger or cap requirements and propose a filling, assembly and testing scope based on the confirmed project information. A written scope should identify open items rather than hiding them behind generic performance language.
FAQ
Does FAT replace IQ, OQ or PQ?
No. FAT is a supplier-site test against an agreed configuration. IQ, OQ and PQ address installation, operation and process performance under the customer’s approved validation system.
Can a substitute product be used during testing?
It can be used to demonstrate machine movement when the final product is unavailable, but it cannot prove final dosing, air behavior, cleaning or product-specific acceptance.
What should be tested for plunger insertion?
Check alignment, insertion sequence, seating, visible air, product displacement, barrel condition, missing-plunger detection and reject behavior using representative components.
What information is needed for a validation plan?
Provide product data, syringe and component drawings, fill target, process sequence, cleaning method, format range, inspection method, utilities and the quality team’s acceptance criteria.
Conclusion
Validation of an intramammary syringe filling line is strongest when every requirement has a defined test and every test records its product, package, recipe and condition. Use design review, IQ, OQ, PQ, FAT and SAT as connected evidence layers, while keeping customer-specific validation and regulatory decisions under the product owner’s quality system.
Send your syringe drawings, product information and validation requirements to request a technical review and FAT plan.
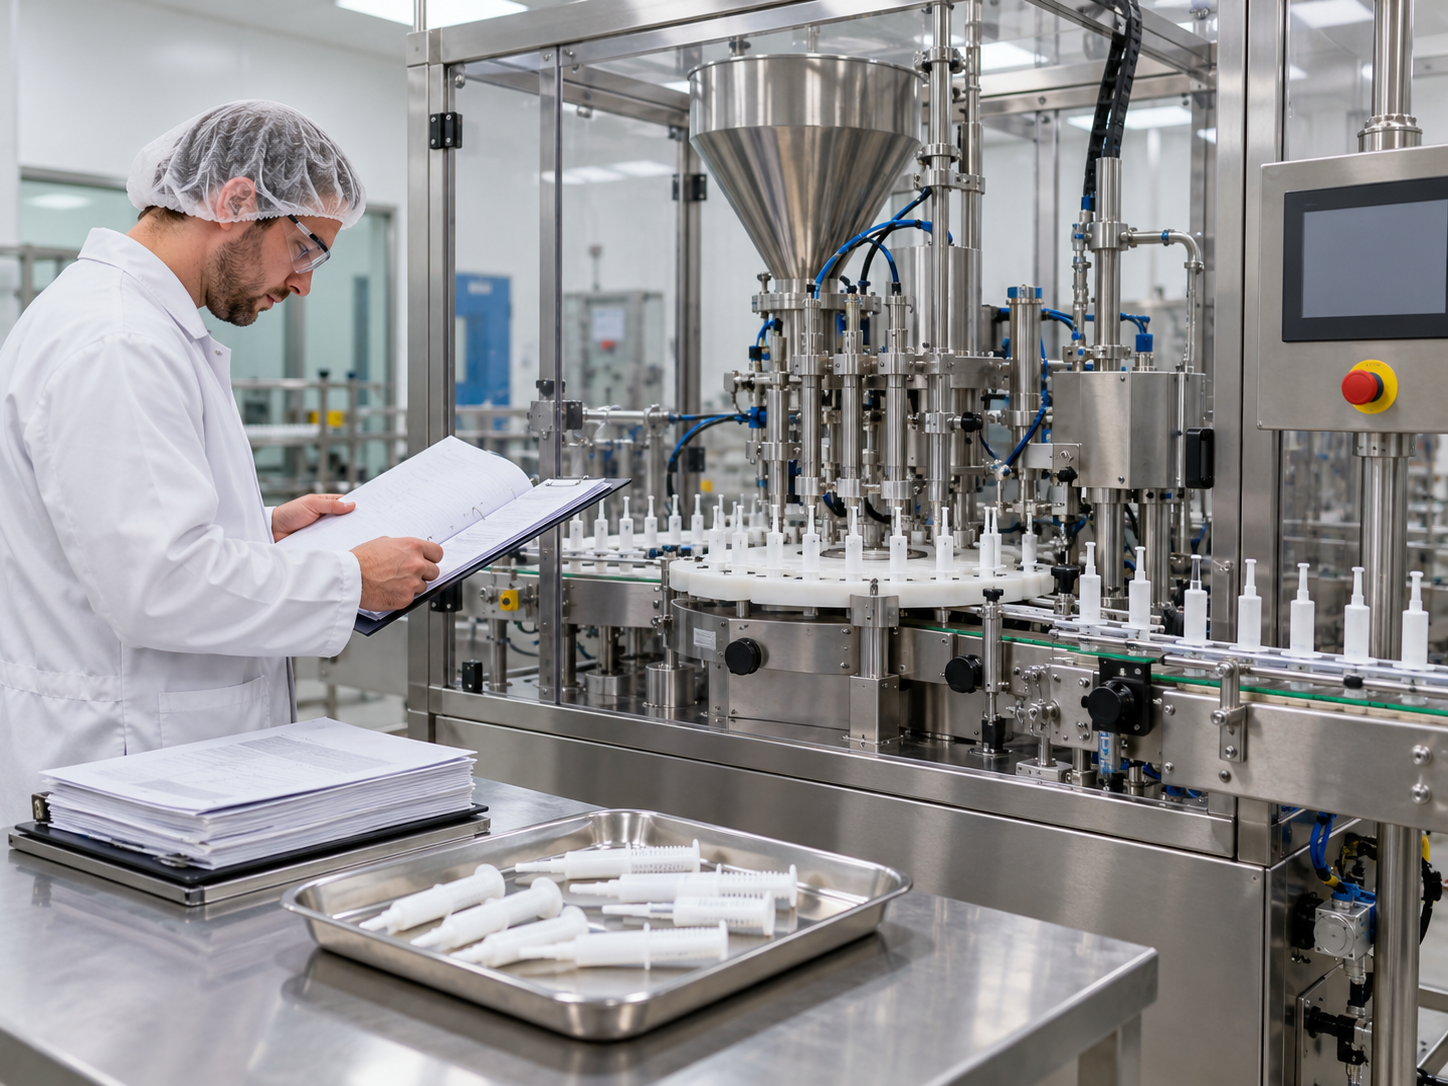
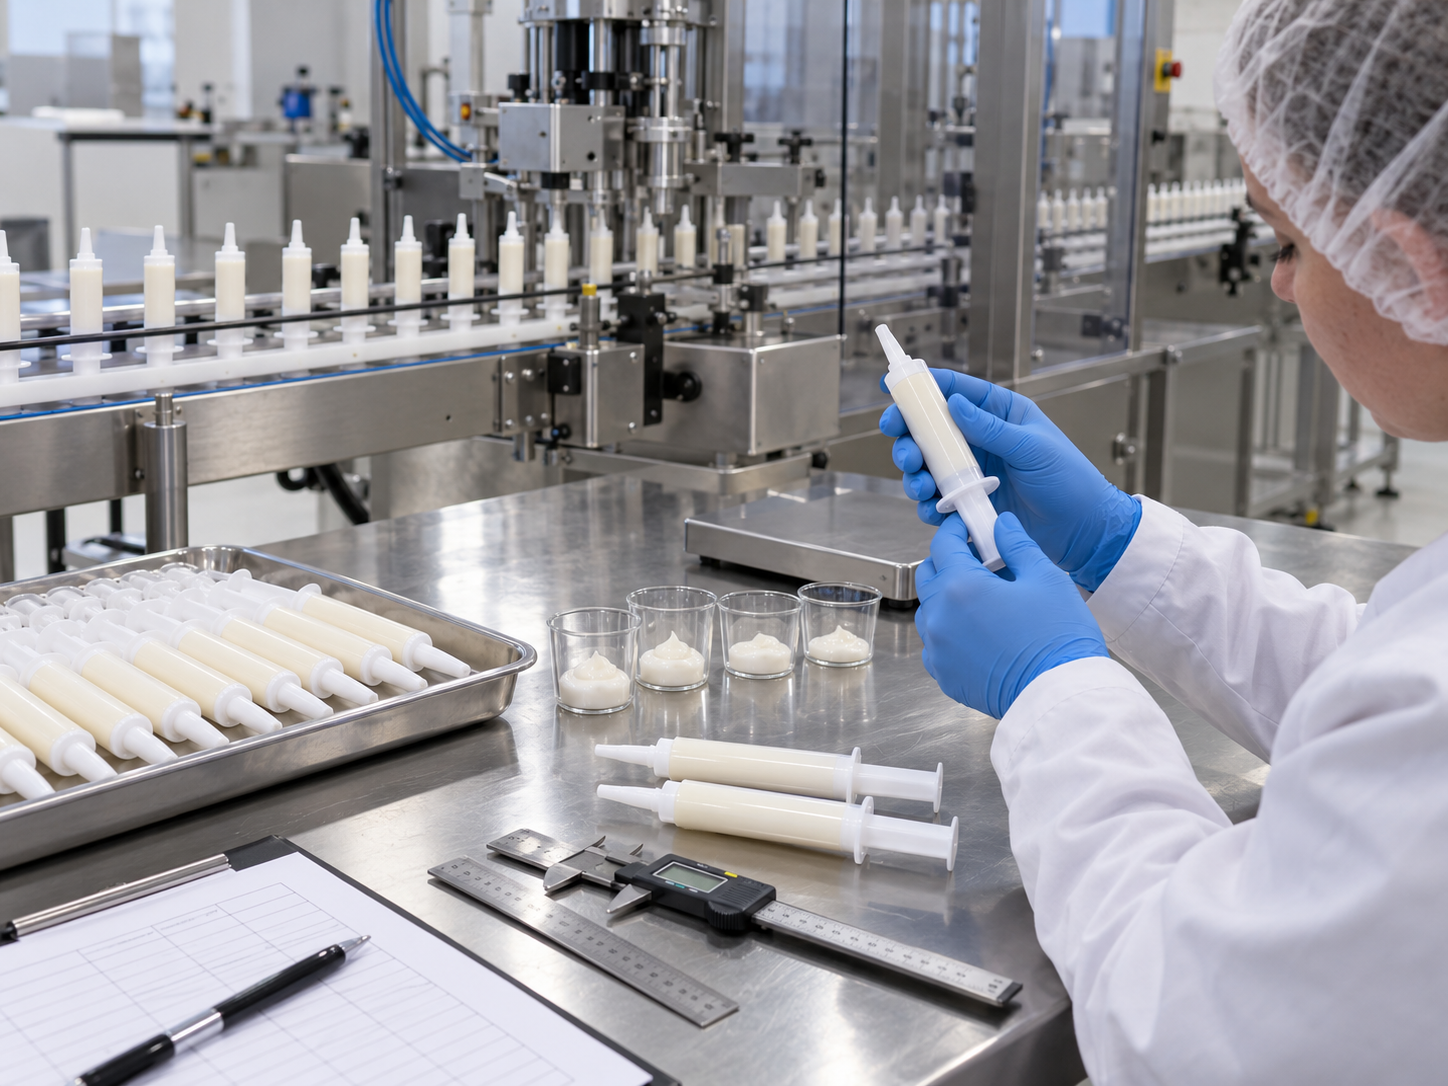
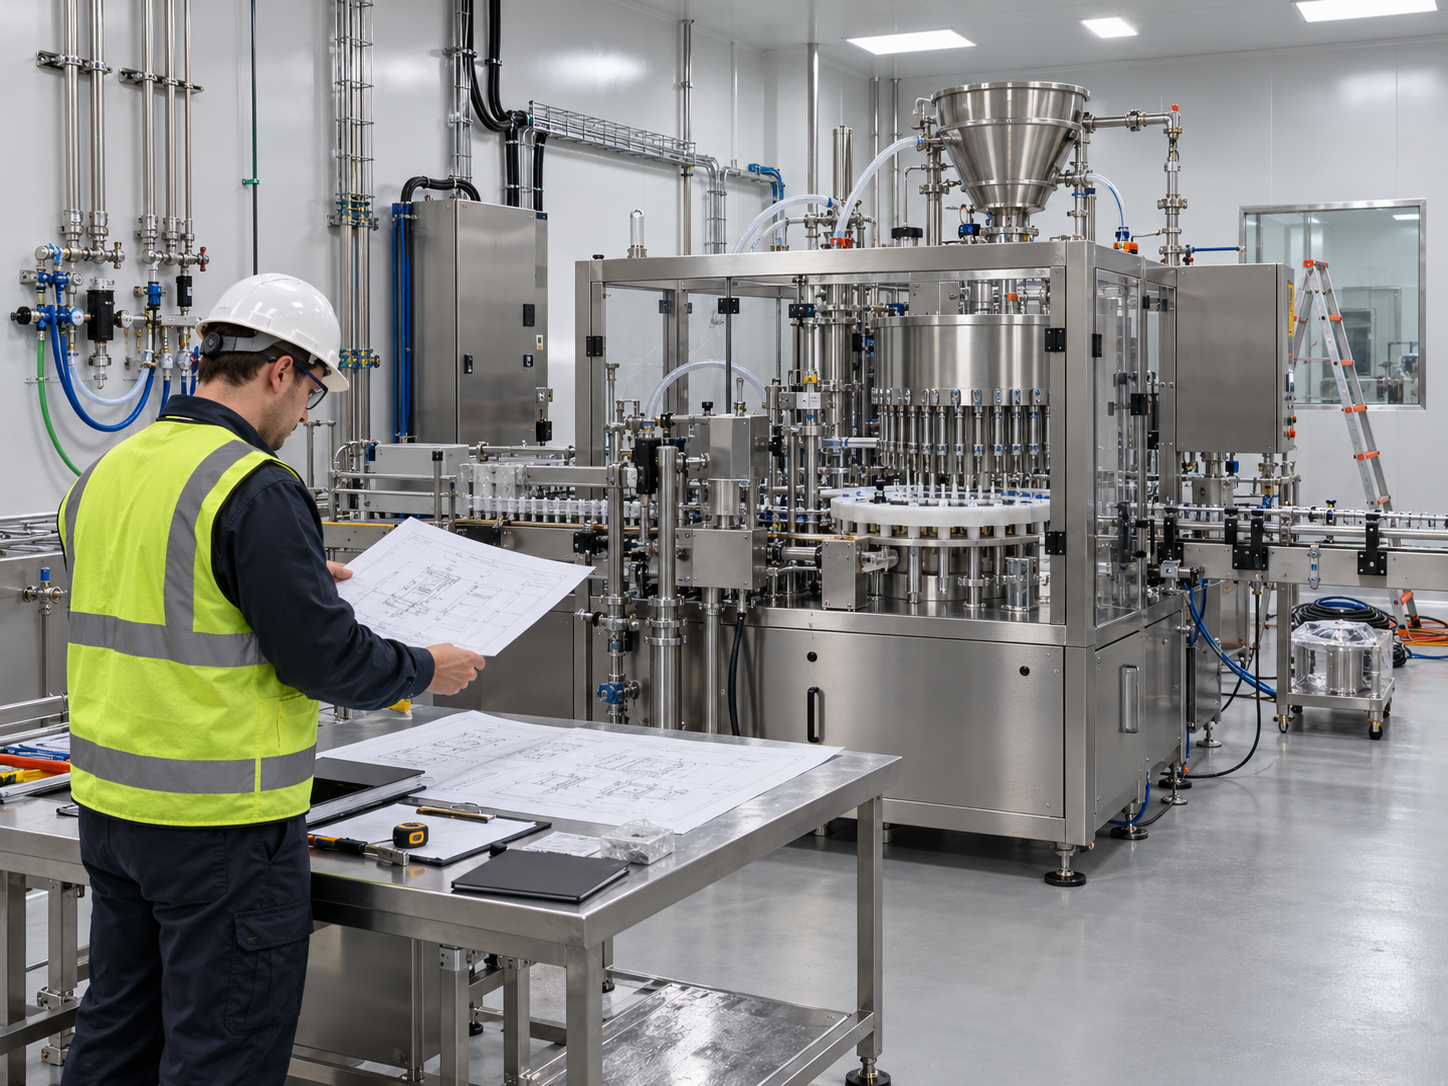
The following visuals are illustrative engineering references and do not present measured output or validation results.
Continue planning with the syringe filling machine range, veterinary medicine application, intramammary syringe solution, filling and capping line, packaging solutions, product catalogue, plunger insertion guide, cleaning guide, format changeover guide, waste reduction guide, contact page and request-a-quote page. Include product, package, process and acceptance details when requesting a proposal.