 Skip to content

AI-generated illustration: define cap retention evidence before cartoning.
Introduction
For an intramammary applicator, the cap is more than a final cosmetic component. It protects the fine tip, completes the package presentation and must remain in place through discharge, cartoning, export packing and handling at the customer site. A cap that is present at the closing station but loosens later can create a complaint, a reject or an avoidable shipment-inspection issue.
Cap retention should therefore be defined before equipment acceptance rather than judged only by a visual check at the machine. The suitable test method, sampling plan and acceptance criterion belong to the product owner’s quality system. The filling-line project must supply the mechanical route, component handling and documented evidence needed to perform those checks consistently.
This article gives a practical framework for veterinary manufacturers and procurement teams preparing an intramammary applicator project. It does not set a universal force value or replace package qualification; actual criteria depend on the approved cap, barrel, product, distribution environment and internal quality requirements.
The direct answer
Cap-retention testing should confirm that the intended cap is correctly fed, seated and retained on the actual intramammary barrel after filling and closing, then remains acceptable through the next packaging handoffs. A useful plan combines defined component lots, a documented closing condition, visual and mechanical checks, reject handling and a clear boundary between factory evidence and site or product qualification.
Request a closure-review checklist
Send your barrel and cap drawings, component samples and intended cartoning route. We can identify the cap-feeding, seating and inspection questions to include in a sample trial or FAT.
Start with the package function
Before selecting a cap feeder or test, define what the cap must do for this package. It may protect a narrow cannula from physical damage, keep the tip clean, prevent an unintended opening, support user handling or preserve a controlled visual presentation. The function determines the risks that should be considered.
Document the cap and barrel interface: material, engagement features, orientation, fit condition, expected seating position, acceptable cosmetic marks and component supply state. Physical parts are essential. A cap can appear compatible on a drawing but behave differently because of molding variation, static charge, surface finish or stiffness.
Confirm component supply conditions
Record whether caps arrive loose, in bulk bags, trays or another presentation. The route from incoming container to cap feeder can affect orientation and surface condition. If a cap is lightweight or prone to static, the feeding approach may need particular attention. The line should not rely on operators correcting a recurrent orientation problem by hand without documenting it.
Use representative barrel and cap lots during the trial. When the customer expects to source components from more than one supplier, identify that early. A test with one lot is useful evidence for that lot and condition, but it does not automatically demonstrate compatibility with an untested alternative.
Separate presence, seating and retention
These three checks are related but not identical.
- Presence asks whether a cap is on the applicator.
- Seating asks whether it reached the intended position or engagement state.
- Retention asks whether it remains attached when the package experiences the defined handling forces and movements.
A presence sensor can show that a cap exists without proving correct seating. A closing station can complete a movement without proving the cap will remain retained through cartoning. The quality plan should make these distinctions visible so the correct equipment functions and test evidence can be selected.
Define the closing route before defining the test
Cap retention begins with how the cap is presented and seated. A complete route may include cap separation, orientation, transfer, applicator location, closing motion, position confirmation and reject discharge. For each step, identify the component feature that controls orientation and the surface that receives mechanical contact.
Feeding and orientation
Fine-tip applicator caps may have a small geometry that is difficult to orient consistently. During factory testing, observe whether the feeder separates caps reliably, whether the transfer maintains orientation and whether any manual intervention is needed. Intermittent feeder errors should be recorded. A short smooth run does not prove that the component feed is robust for the planned campaign.
Seating motion and package support
The barrel must be supported while the cap is seated. If the package is allowed to move, the apparent closing condition can vary. Tooling should locate the barrel at a repeatable datum and protect the cannula from unintended contact. Where the project uses a monitored closing motion, agree what data is available and how it will be interpreted by the customer’s quality team.
Build a test plan that fits the real risk
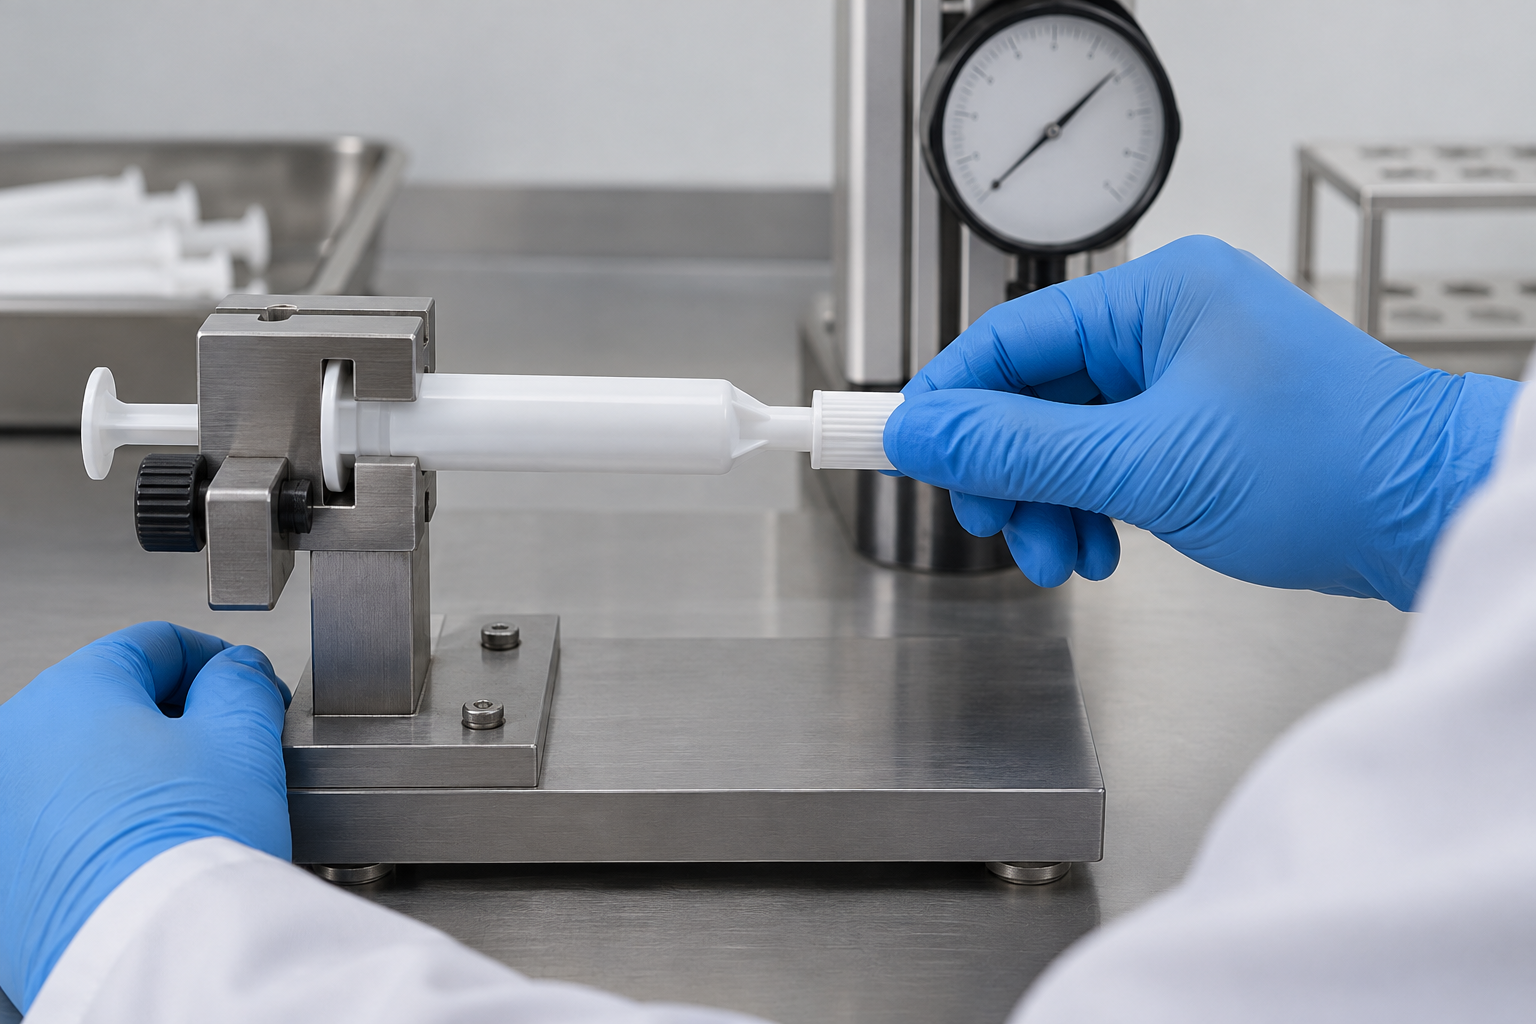
AI-generated illustration: A cap-retention test should use an agreed method and clearly state what condition it evaluates.
The product owner should define test methods and criteria based on the package and distribution requirements. The filling project can support this by documenting the samples, closing condition and inspection points. A practical plan commonly includes the following elements.
- Identify the barrel and cap lot, drawing revision and sample condition.
- Record the line configuration, change parts and closing route used.
- Confirm cap presence and intended visual seating after closing.
- Perform the customer-defined mechanical or handling check on a documented sample set.
- Inspect the barrel, cap and cannula after the check for visible damage or displacement.
- Record rejects, adjustments and any open actions.
Avoid using an unverified universal pull-force target in a marketing document. The appropriate value and method must come from the customer’s approved packaging and quality requirements. What equipment suppliers can demonstrate is that the configured station repeats the agreed mechanical process with the tested components.
Include cartoning and shipment handoffs
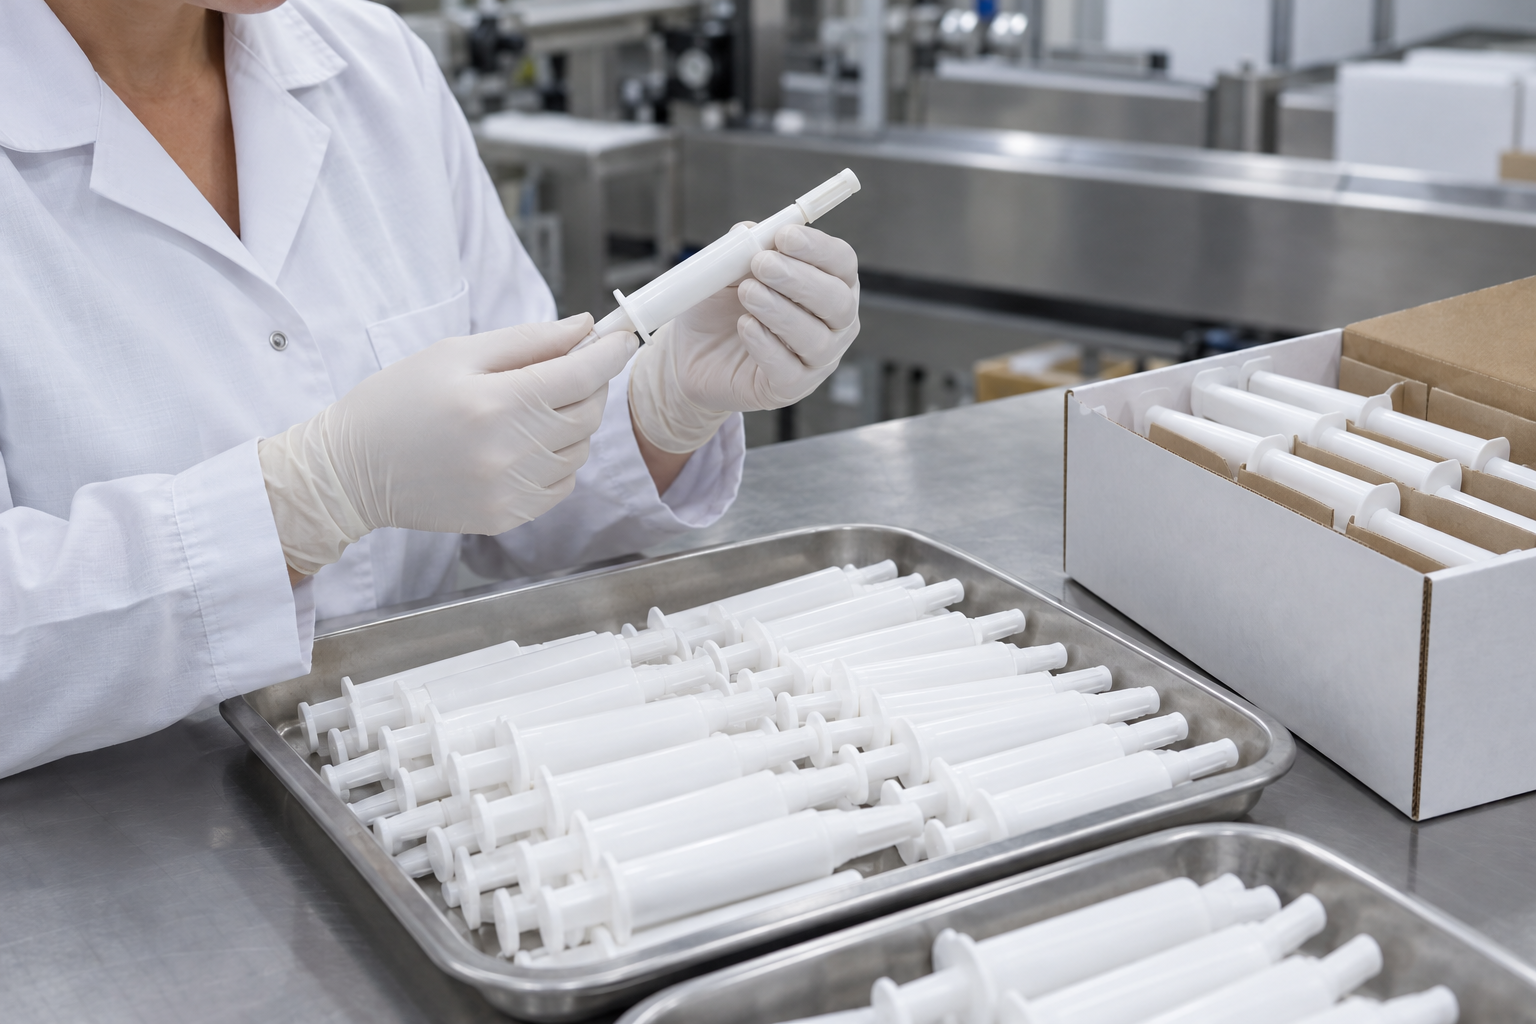
AI-generated illustration: Shipment inspection can confirm the condition of capped units before the secondary-packaging handoff.
A cap can be acceptable immediately after closing yet encounter a problem when applicators are accumulated, transferred, loaded into a carton or packed for export. Map the route from the cap station through discharge and cartoning. Look for drops, uncontrolled contact, excessive compression, guide-rail interference and points where a fine tip can touch another package.
For export projects, shipment inspection is a useful additional check. Before crating, confirm that finished applicators are protected in the intended secondary package, that change parts and documentation are identified and that the packing arrangement reflects the approved handling route. This is not a claim that the equipment guarantees distribution performance; it is a practical way to verify that the supplied package protection and handoff plan are understood.
Factory trial, FAT and site acceptance
Use the factory trial to learn how the actual parts feed and seat. Use FAT to confirm the final supplied equipment against the agreed scope. Use site acceptance to confirm that the installed line, local utilities, actual incoming components and trained operators reproduce the intended process. These stages are connected, but they are not interchangeable.
The FAT record should identify which cap lots were used, what the machine checked, which handling challenges were observed and any criteria that remain the customer’s responsibility. If the customer needs a specific retention-test method, it should be agreed before FAT with the correct instruments, samples and acceptance logic available. Do not label a machine as package-qualified simply because it closed a limited set of trial parts successfully.
Mid-article CTA — Send your closure samples
Share the barrel, cap and intended secondary-packaging sequence. We can prepare a project-specific review of cap feeding, support tooling, inspection points and factory-test observations.
Train operators to recognise real defects
Operators should have a clear visual reference for acceptable and unacceptable cap conditions. Use actual project photos where possible: correct cap seating, missing cap, visibly tilted cap, damaged cap, scuffed barrel and affected cannula. Define the immediate operator action and the escalation path. A defect library is often more useful on the floor than a long generic procedure.
During start-up, check the first acceptable samples against the approved reference. During the run, follow the manufacturer’s documented frequency for in-process checks. When a problem appears, record the component lot, station, condition and adjustment. This data helps distinguish a component-supply issue from a feed, closing or downstream-transfer issue.
Define a practical sampling and escalation route
The number of samples, timing and acceptance criteria must come from the customer’s approved quality plan. Even so, the project team should decide when checks happen and what information travels with a failed sample. A sensible workflow distinguishes start-up confirmation, routine in-process observations, checks after a planned adjustment and review after an interruption that may affect the closing route. It should identify the lot, time, line condition and station so the observation can be understood later.
An escalation route also prevents operators from repeatedly correcting a symptom without preserving evidence. For example, a missing-cap reject might point to cap-feed separation, a tilted cap to orientation or applicator support, and a loose cap after cartoning to a downstream contact point. The immediate action may be to stop or segregate product according to the customer’s procedures, but the technical review should begin with the actual condition and component lot rather than a generic adjustment.
| Finding | First evidence to collect | Review focus |
|---|---|---|
| No cap detected | Cap lot, feeder status and transfer observation | Separation, orientation and presence inspection |
| Cap present but visibly high or tilted | Seating image, barrel location and closing condition | Package support, tooling position and component fit |
| Cap displaced after discharge | Transfer-point photo and guide settings | Downstream contact, accumulation and handoff control |
| Visible cap or cannula damage | Part sample, contact zone and route record | Tooling clearance and packaging protection |
The table is not a release procedure. It is a way to make the factory trial, FAT and routine production conversations more evidence-led.
Check the interface with secondary packaging
Cartoning equipment and manual packing arrangements should be reviewed as part of the closure route, especially when applicators are placed in a specific orientation or accumulated before loading. The applicator should not be pushed, compressed or dropped in a way that was absent from the factory closure demonstration. If the secondary package uses dividers, trays or a defined orientation, include representative examples in the project discussion whenever practical.
For an export shipment, the same thinking applies to spare parts and documentation. During shipment inspection, identify the installed closing tooling, any format-specific parts and the component drawings used for the trial. This makes it easier for the receiving team to confirm that it is starting with the same mechanical assumptions. It does not replace distribution testing or prove a product’s shelf life; those remain customer-owned package-qualification activities.
Set clear responsibilities before FAT
The equipment supplier and product owner contribute different parts of a cap-retention project. The supplier can describe the cap-feed, seating, handling and inspection functions within the supplied scope, run agreed samples and record observations. The customer must provide approved components, product information where relevant, quality criteria, sampling logic and final disposition rules. A third-party test laboratory or the customer’s packaging group may own any specialised retention or distribution test method.
Agree these boundaries before FAT. If a specific gauge, fixture or calculation is expected during the test, confirm who provides it, what condition the samples must be in and how results will be recorded. This avoids an unproductive situation in which a mechanical trial is mistaken for final package qualification or a quality requirement reaches the project after the closing station has already been designed.
Use the review to improve the next component lot
Cap-retention observations become more useful when they feed back into controlled component management. Retain a small reference set of the barrel and cap lots used at the factory when the customer’s procedures allow it, together with the drawing revision, sample condition and trial record. If a later lot behaves differently, the team has a factual reference for checking engagement features, molding condition and supply presentation before changing the machine.
This matters where supply chains change over time. A new cap supplier, an unannounced drawing revision or a different packaging method can alter feeding and seating even though the nominal part name is unchanged. The customer’s change-control system should determine when a review or requalification is required. The filling-line supplier can support the discussion by identifying the handling datums and station settings that were used with the original samples.
The same approach helps with preventative maintenance. If cap seating becomes less consistent, inspect the closing tooling, locating features and transfer route against their documented condition before assuming that the cap specification is at fault. Controlled observations, rather than trial-and-error adjustments, protect both production time and the package evidence needed by the quality team.
FAQ
Is cap presence inspection enough?
No. Presence confirms that a cap exists. It does not necessarily confirm correct seating or retention through cartoning. Use the checks defined by the package and quality plan.
Can a cap-retention value be set from a generic article?
No. The appropriate method and criterion depend on the specific barrel, cap, product and distribution requirements. They should be defined and approved by the product owner.
What samples should be used for a factory trial?
Use representative barrels and caps, preferably with known lot information, together with the intended applicator format and agreed product condition. Include the secondary-packaging sequence where it affects handling.
The line should remove it through a defined, visible reject route. The manufacturer’s quality system should define segregation, reconciliation and disposition requirements.
Does an AI illustration prove an acceptable cap condition?
No. Illustrations explain the review process but must not become product acceptance evidence. Use customer-approved photographs and physical samples from identified components for operator references. Define functional retention requirements separately from a visual seating judgement, using the customer’s approved assessment method.
Conclusion
Cap retention is a package-performance question supported by a controlled closing route. The strongest project plan separates cap presence, seating and retention; uses representative components; reviews downstream handoffs; and records exactly what the trial, FAT and site acceptance demonstrate. That approach protects the fine-tip applicator and gives production and quality teams a practical basis for managing the closure process before cartoning.
Discuss your intramammary closure project
Contact Us: KINGPACK can review intramammary barrel and cap samples, define the questions for a closing-route trial and configure the associated filling-line handling stations. Contact us to request a closure review, sample plan or equipment proposal.
—
