
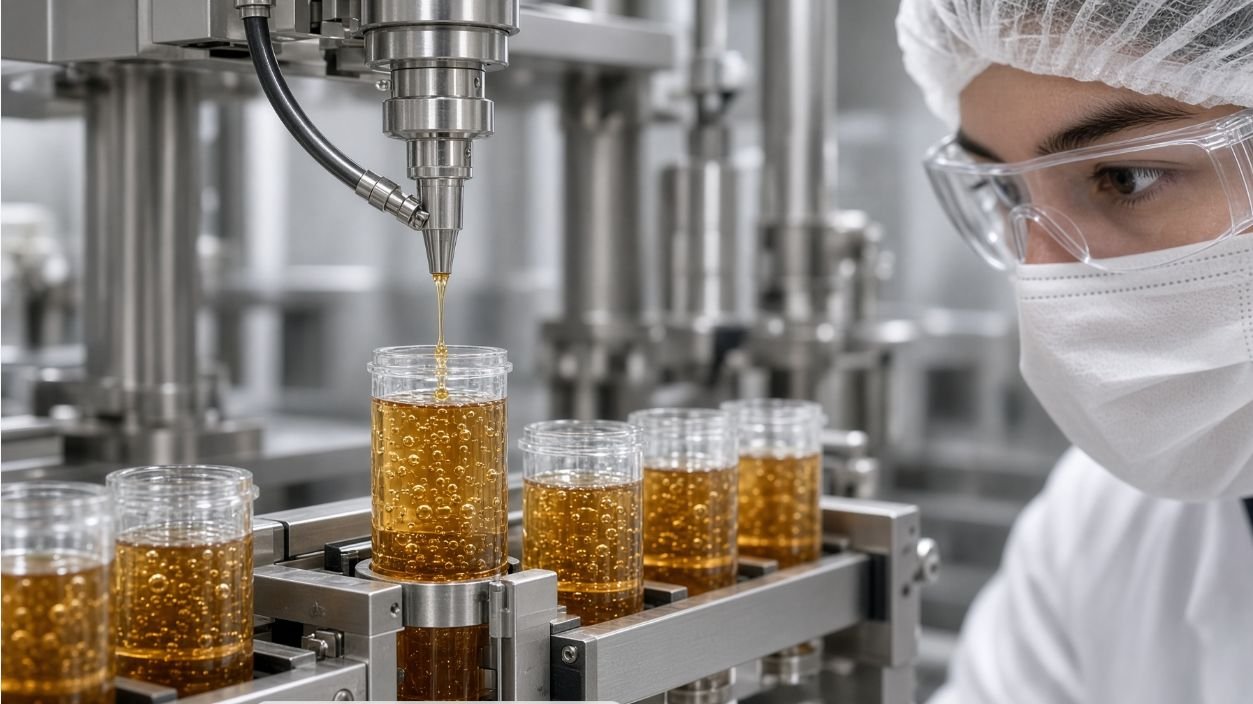
When a gel bait syringe filling line produces a barrel with a bubble in the gel, a strand hanging off the tip, or a smear of paste around the nozzle, it is tempting to treat all three as “the filling is bad” and adjust the same setting. That usually wastes time, because the three defects come from different places: air bubbles are a gas-trapping problem, stringing is a material cut-off problem, and nozzle residue is a timing and geometry problem. A bubble cannot be fixed by changing suck-back, and a stringing strand cannot be fixed by degassing the bulk. This article separates the three gel bait syringe filling problems so a line can be investigated systematically instead of by trial and error.
Separate Trapped Air from Stringing Before Touching Anything
The first step is to name the defect precisely, because the name determines which stage of the line to inspect.
Air bubbles are voids inside the gel mass. They are compressible, which is why they cause two measurable effects: a fill weight that drifts (the bubble changes how much paste actually sits in the barrel) and a piston that can “bounce” or sit proud of the gel because gas is trapped between the piston and the product. Bubbles can be large and visible or microscopic and only show up as weight variation.
Stringing (or tailing) is a strand of gel that trails from the nozzle or tip as the nozzle pulls away after dosing. It is a rheology problem: the paste is tacky or elastic enough that it stretches instead of breaking cleanly at the cut-off point. Stringing leaves a visible tail but does not by itself mean the barrel contains air.
Nozzle residue (dripping / drooling) is material left at the orifice or tip after the dose ends. It is a cut-off and timing problem—the flow is not stopped cleanly, so a bead or film remains and may transfer to the closure or the outside of the barrel.
The three can occur together—a paste that strings often also leaves residue, and a paste full of air often weighs inconsistently—but they are investigated separately. Recording which one is present, on which station, and whether it is constant or intermittent is the whole basis of the diagnostic table below.
| Symptom | Likely stage | Possible causes to check | Verification method |
| Visible bubble inside the gel mass | Feed / dosing | Air folded in during bulk transfer; hopper run low; pump cavitation; no deaeration step | Let a filled barrel stand upright and watch whether the bubble rises; weigh across cycles |
| Piston sits proud of gel / “bounce” | Piston insertion | Gas trapped between piston and gel; piston inserted too fast; wrong piston profile | Squeeze barrel gently during insertion; compare seated vs. unseated piston |
| Weight drifts across cycles | Dosing | Entrapped air changing delivered mass; cut-off variation | Weigh N consecutive fills; plot range vs. target |
| Strand trailing from tip | Cut-off / nozzle | Paste too tacky; retract speed; insufficient suck-back; worn nozzle | Vary retract and suck-back on a single sample set |
| Bead or smear at orifice | Cut-off / closure | Suck-back timing; nozzle drip; closure contacting wet tip | Film the cut-off in slow motion; inspect tip after each cycle |
This table is the working tool for the rest of the article. Each row points at a different part of the line, which is the point: a bubble diagnosis and a stringing diagnosis should never end at the same adjustment.
Inspect the Feed and Filling Stages for Entrapped Air
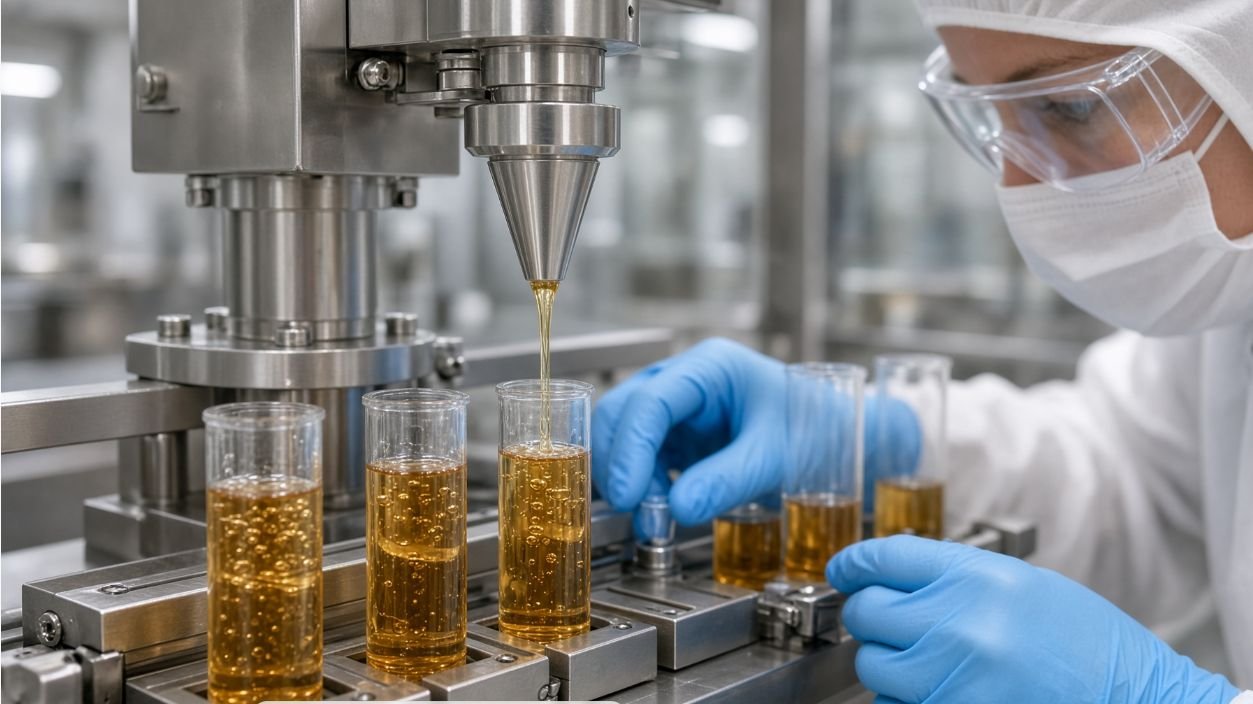
Air bubbles in gel bait syringe filling usually originate before the dosing head, in the feed path. High-viscosity pastes trap air when they are transferred from a bulk container, when the supply hopper is topped up, or when the feed level drops and the pump starts drawing a mixture of paste and air. The industrial dispensing principle is well established: entrapped air in a syringe barrel causes oozing, drooling and inconsistent deposits, and the fix is to keep air out of the fluid rather than to chase it downstream (Nordson EFD, Last reviewed: 2026-09-10).
What to inspect in the feed and filling stages:
- Bulk transfer. Does the paste get poured, pumped, or scooped into the hopper in a way that folds air in? A material that is decanted through a large drop can entrain more air than one transferred gently.
- Hopper level. Does the line run the hopper to near-empty between top-ups? A low level can starve the pump and pull air.
- Degassing. Is there any step that lets the paste release air before dosing—settling time, vacuum, or a deaeration stage? Thick pastes hold air for a long time unless the gas is actively removed.
- Fill fraction. For a barrel being filled in an open condition, overfilling leaves no head space and can push air into the product or trap it against the piston face.
None of these is a gel-bait-specific law; they are the standard reasons air enters a viscous product path. The point for a buyer is that the feed system and the degassing step are equipment decisions, not afterthoughts, and they should be discussed with the supplier before a configuration is fixed.
Check Piston Contact and Package Air Pockets
A second, distinct source of air sits at the piston interface, not in the bulk. When a piston is inserted into a filled barrel, air can be trapped between the piston face and the gel. The result is a piston that sits proud of the product or “bounces” off it, and the trapped pocket can later expand and push gel out or cause weight variation. Dispensing literature describes the common causes of piston bounce as improperly installed pistons, air already in the fluid, and running thick paste at high speed, and recommends gentle barrel squeezing during insertion, proper piston profiles, and degassing thick fluids before fill (Nordson EFD, Last reviewed: 2026-09-10).
For a gel bait line, the practical checks are:
- Piston insertion method. Is the piston pushed straight and slowly enough that air can escape past the sealing edge, or is it driven in fast against a stiff gel?
- Piston profile. Does the piston’s sealing face match the barrel interior and the paste’s behaviour, or does it cup air against the product?
- Venting. Is there a controlled vent path so the piston does not pressurise the air pocket against the gel?
- Pre-inserted vs. loose pistons. Whether the piston arrives already seated or is inserted on the line changes where this air pocket can form—and therefore where it must be inspected.
This is why the piston/plunger supply state, which is covered in the broader packaging selection discussion, is not a minor detail: it directly determines whether the line has a piston-insertion station that must be validated for air-free seating.
Tune Nozzle Cut-Off and Movement Timing for Stringing
Stringing and nozzle residue are cut-off problems, not air problems. When the dosing head retracts from a tacky, elastic gel, the paste must break cleanly at the orifice or tip. If it does not, a strand trails or a bead remains. The levers are mechanical and rheological together:
- Suck-back (reverse draw). A short reverse stroke at the end of the dose pulls paste back into the nozzle so the column is not proud of the orifice. This is a standard cut-off technique for viscous fluids; it reduces, but does not guarantee elimination of, stringing for every formulation.
- Nozzle geometry. A nozzle with the wrong orifice size or taper for the paste’s rheology strings more than a matched one.
- Retract speed and timing. How fast and when the nozzle withdraws relative to the end of the dose changes whether the paste snaps off or drags.
- Closure sequence. If the cap or tip is applied while the interface is still wet with paste, residue can transfer to the closure and show up later as smearing or leakage at the seal.
Because stringing depends on the material’s tack and thixotropy, the same cut-off settings that work for one gel bait may string badly with another. The correct sequence is to characterise the paste first—viscosity and its behaviour at filling temperature—and then match nozzle and cut-off parameters, rather than to hunt for a universal setting. This connects directly to measuring product properties before equipment selection.
Run Controlled Sample Trials to Confirm the Diagnosis
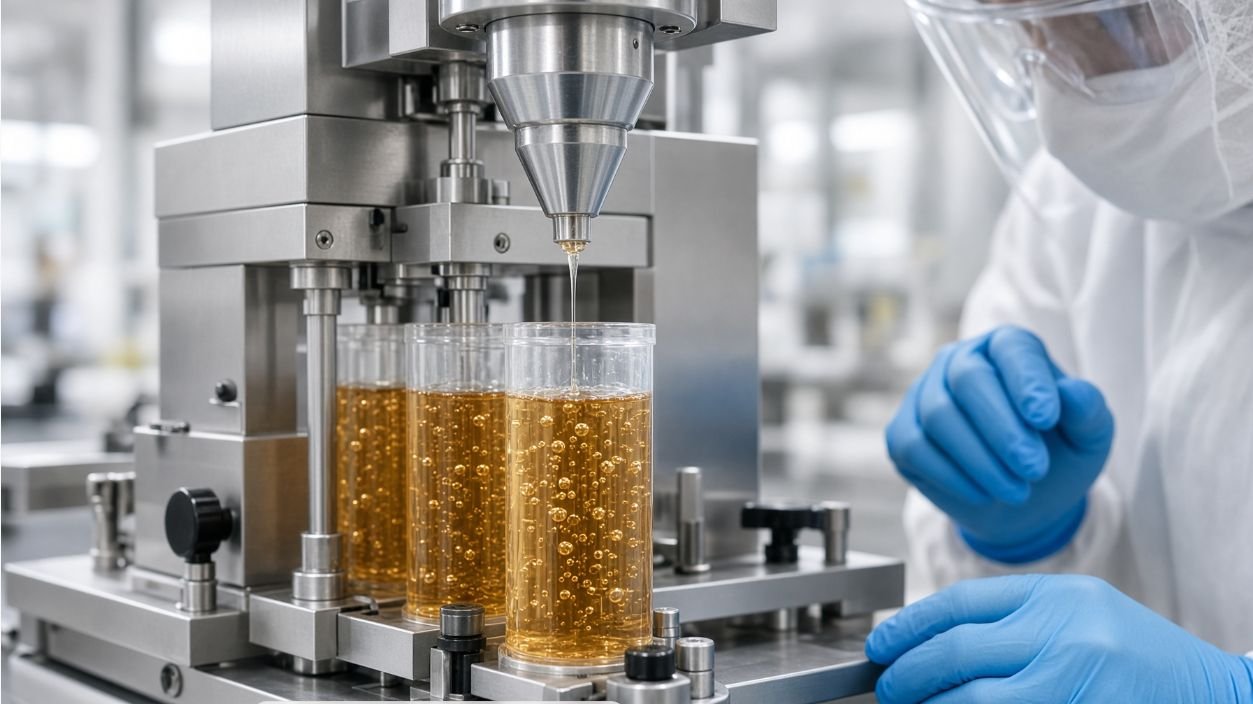
A defect that is guessed at is often “fixed” by changing several variables at once, which means nobody learns which change actually mattered. The reliable way to close a gel bait syringe filling problem is a controlled sample trial in which one variable changes at a time, using the real paste and the real barrel, piston, tip and cap.
A useful trial plan:
- Capture the baseline. Run the current configuration and record the defect on video, plus fill weights across a run of consecutive units.
- Change one factor. For a bubble problem, change only the feed condition or the degassing step. For stringing, change only suck-back or retract speed.
- Record the result. Log whether the symptom reduced, and by how much, on the same sample set and the same paste batch.
- Repeat. Move to the next variable only after the previous one is isolated.
The output of a controlled trial is evidence: which setting or station is responsible, and what the remaining acceptable level is. That evidence is also what a supplier needs to act—sending a defect video, the paste’s state, and the full component set lets the machine supplier evaluate the problem against the actual material instead of guessing from a description.
Common Risks and Mistakes
- Treating air, stringing and residue as one fault. They come from different stages; one adjustment rarely fixes all three, and “fixing” the wrong one wastes production time.
- Chasing air downstream. If air is folded in at transfer or the pump is starving, no downstream nozzle change will remove it.
- Adjusting cut-off to cure a bubble. Suck-back does not degas a paste, and degassing does not stop a tacky paste from stringing.
- Ignoring the piston interface. A piston seated against trapped gas will keep producing weight variation even after the bulk is deaerated.
- Changing several settings at once. This hides which change worked and makes the defect likely to return on the next batch.
- Using a “universal” cut-off setting across formulations. Stringing is material-specific; settings must be re-matched when the paste changes.
How to Compare Suppliers When a Defect Must Be Solved
When a filling defect is the reason a buyer is evaluating equipment, the comparison should centre on how each supplier would diagnose and demonstrate a fix, not on a generic capability list.
- Ask how they would isolate the fault. A supplier that proposes a controlled, one-variable-at-a-time trial is more credible than one that promises a single setting will solve everything.
- Ask what sample material they need. A real diagnosis requires the actual paste and package, not a stand-in.
- Ask what the trial will measure. Fill weight range, bubble presence, stringing length, and residue at the tip are the outputs to agree on.
- Ask about cut-off and degassing options. Whether the line can be configured with suck-back, a matched nozzle, and a feed/deaeration path is a configuration question, not an accessory question.
- Ask how the fix is validated. The result should be a recorded trial with the buyer’s own material, not an assertion.
How King Pack Supports This Application
King Pack Machinery (Wuxi King-Pack / Wuxi Jingpai Machinery Co., Ltd., founded 2009, with a core technical team carrying more than 20 years of industry experience) treats a gel bait syringe filling defect as an engineering investigation, not a warranty-adjacent promise. The practical way King Pack supports this application is:
- Fault isolation against the real material. Air, stringing and residue are separated and traced to the feed path, the piston interface, or the cut-off stage, using the buyer’s own paste and components.
- Sample-based configuration. The metering head, cut-off (including suck-back and nozzle geometry) and any deaeration or venting in the feed path are configured against the actual gel, not a generic viscous-fluid assumption.
- Recorded trials. Defect videos, fill-weight runs and the trial plan become part of the evaluation, so the fix is evidenced rather than asserted.
- Factory acceptance context. Once a configuration is fixed, the run conditions, measurement methods and acceptance criteria are agreed and recorded—the same discipline that governs the final acceptance test.
King Pack does not claim a no-bubble or no-stringing guarantee for every gel bait formulation. What is offered is a method: isolate the fault, test the real product, and configure the line around evidence. That is the difference between a machine that “should work” and one that is shown to work on the buyer’s own material.
Conclusion
Air bubbles, stringing and nozzle residue in gel bait syringe filling are three different problems with three different homes on the line. Naming the defect correctly, then inspecting the feed path, the piston interface, and the cut-off stage separately, turns a frustrating “the filling is bad” into a solvable diagnostic. The cure is not a single setting but a controlled trial on the real paste and package—which is exactly the evidence a supplier needs to configure the line properly.
Investigating a bubble or stringing problem on your line? Send a defect video, the paste’s state, and your complete syringe component set to discuss a controlled evaluation of your gel bait syringe filling problems.