 Skip to content

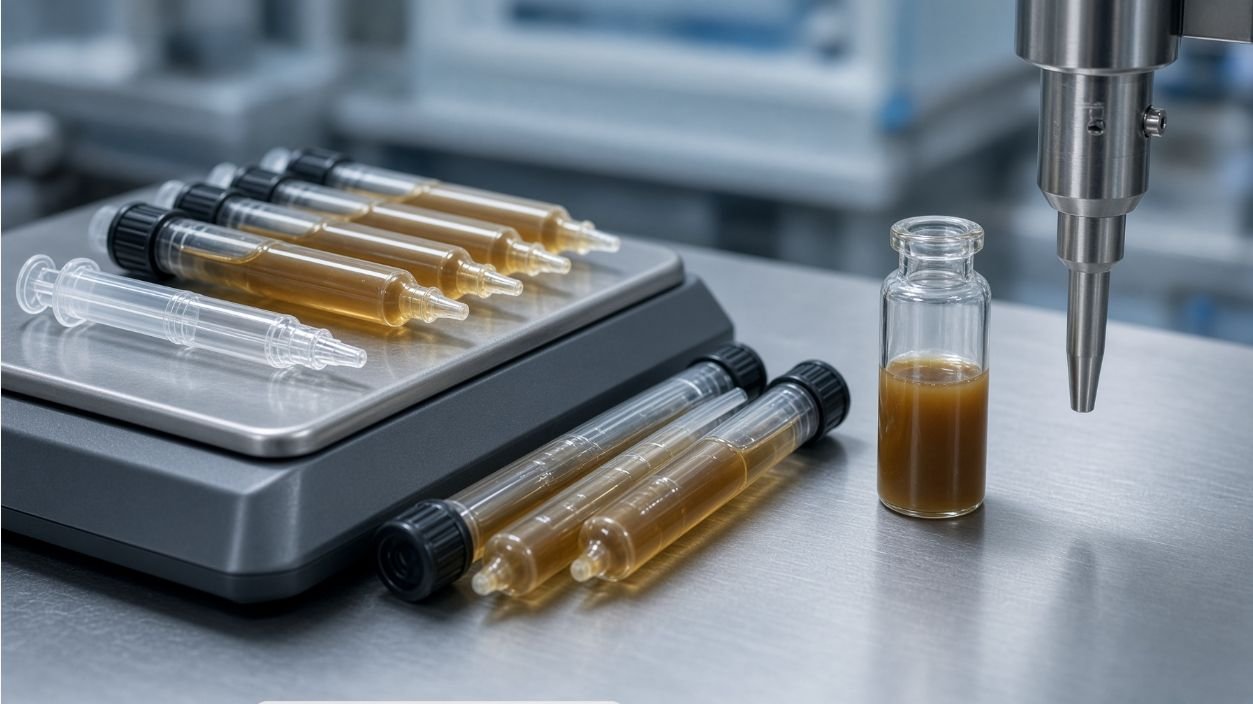
A gel bait is sold by weight—typically a mass in grams printed on the label—but a syringe filling machine doses by volume: a piston stroke, a pump displacement, a dispensed quantity. The two are only the same when density is constant and known, which for a paste is rarely a safe assumption. This is the core of gel bait net weight control: a product sold by mass, filled by a volume-based machine, must be reconciled through density, tare weight and a weighing protocol. Skipping that reconciliation is how a line that “fills accurately by volume” still produces under-fill or over-fill by weight.
Labelled Mass Is Not the Same as Syringe Capacity
The first confusion to remove is between the number on the label and the volume the barrel can hold. A commercial cockroach gel bait is commonly packaged as a 30 g syringe—a mass, not a millilitre figure (Syngenta Advion Cockroach Gel Bait, pack size “30 gr Syringe”, Last reviewed: 2026-09-10). A 30 g tube does not hold 30 mL unless the gel’s density happens to be exactly 1.0 g/mL, which is not something anyone should assume.
Three separate quantities sit behind every fill:
- Labelled mass. The net content the product is sold by, in grams. This is the legal and commercial target.
- Syringe capacity. The geometric volume the barrel can contain, in millilitres. This is a packaging property, not a fill target.
- Delivered dose. What the machine actually dispenses, expressed either as a volume (the pump setting) or a mass (what a scale reads).
A machine set to dispense “30” on a volume basis is not filling 30 g unless the density relationship has been measured and the setting calculated from it. The distinction matters because under-fill by weight can be a regulatory and customer-complaint issue, while over-fill by weight is pure product give-away—excess gel given away in every unit.
| Quantity | Unit | Where it comes from | What it is not |
| Labelled net content | g (mass) | Product specification / label | Not the barrel’s volume |
| Barrel capacity | mL (volume) | Packaging geometry | Not the fill target |
| Machine dose setting | mL or pump displacement | Equipment configuration | Not automatically equal to mass |
| Weighed fill | g (mass) | Scale reading | The only direct measure of net content |
Measure Density at the Conditions That Matter
Because mass = volume × density, the density value is the bridge between a volume-based machine and a mass-based specification. The trap is that density is not a single fixed number for a paste:
- Temperature. A gel’s density changes with temperature, and the filling temperature may differ from the storage temperature. The density must be measured at the temperature at which the product will actually be filled.
- Batch variation. Different production batches can differ slightly in density, especially if the formulation or the amount of entrained air varies.
- Entrapped air. Air in the gel lowers its effective density for the same volume, which is one reason a fill can weigh less than expected even when the volume setting is unchanged. Air control is a separate subject, but it interacts directly with weight control.
The practical requirement is to measure density with a stated method (e.g. pycnometer or calibrated weighing of a known volume) at the relevant temperature, and to confirm how much it varies between batches. Without a measured density, a buyer is asking a supplier to hit a mass target with a volume machine and no conversion factor—which is how net content disputes begin.
Separate Gross, Tare and Net Fill
Net weight control for gel bait syringe filling is a weighing exercise with three numbers, and the discipline is to keep them distinct:
- Gross weight. The filled barrel (or barrel plus closure) on the scale.
- Tare weight. The weight of the empty package and its components before fill. This includes the barrel, piston, tip and cap, and it can vary slightly between suppliers and batches.
- Net weight. Gross minus tare—the actual mass of gel delivered.
The tare value is not a constant to set once and forget. Barrel and closure weights vary within tolerance, and that variation lands directly in the net weight calculation. If tare is assumed constant but the barrel actually varies by a fraction of a gram, the “net weight” the line reports is wrong by that amount.
A repeatable weighing protocol matters more than the scale’s advertised resolution:
- Zero and verify the scale against a known reference before each session.
- Weigh the empty package (tare) for the actual lot, or record the tare from a sampled set, not from memory.
- Weigh the filled unit (gross) under stable, consistent conditions.
- Calculate net = gross − tare, in the same units, on every check.
- Record the batch, the operator, and the time, so a weight dispute can be traced to a lot and a setting.
A simple record template is the cheapest quality tool on the line:
| Field | Example entry | Purpose |
| Batch / lot | 2026-09-B12 | Trace weight to a production lot |
| Tare reference | 4.12 g (sampled avg) | Basis for net calculation |
| Target net | 30.0 g | The mass specification |
| Measured gross | 34.18 g | Raw scale reading |
| Calculated net | 30.06 g | The number that matters |
| Result | Accept / investigate | Decision against tolerance |
Build a Repeatable Weighing Protocol, Not a One-Off Check
A single weigh-in at start-up does not constitute gel bait net weight control. Weight control is a repeated measurement at agreed intervals, on a defined sample, with the results written down. The elements to fix before the line is specified or accepted:
- Sample plan. How many units per check, and how often—linked to the batch size and the risk of drift.
- Interval. Start-of-batch, after every format change, and at periodic intervals during a run, plus any time a parameter (dose, temperature, feed level) changes.
- Tolerance. The acceptable range around the target net, agreed in the units the product is sold in, and aligned with the target market’s legal requirements.
- Escalation. What happens when a check is out of range—adjust, re-check, quarantine—rather than leaving it to operator discretion.
The weighing protocol is also the evidence a buyer brings to a factory acceptance test. If net content is the acceptance criterion, then the measurement method, sample size and tolerance must be agreed before the test, not argued about during it.
Agree Acceptance Criteria Before the FAT
Net content is the one specification that cannot be left vague, because it is both a legal requirement and the basis of the buyer–supplier acceptance test. Before a factory acceptance test for a gel bait syringe filling line, both sides should agree in writing:
- The net content target and tolerance, in grams, for each format.
- The measurement method—which scale, which tare convention, which sample plan.
- The density value and its conditions, including temperature and batch, that the volume setting is based on.
- Which defects are rejects (under-fill below the legal/agreed floor, over-fill above an agreed give-away ceiling) versus rework.
- How results are recorded and signed off.
Agreeing these points in advance turns “does the machine fill accurately?” into a testable, recorded statement. Without them, “accurate” means whatever each side decides after the fact.
Common Risks and Mistakes
- Assuming 30 g equals 30 mL. Mass and volume coincide only at density 1.0 g/mL, which a paste is not guaranteed to have.
- Filling by volume and trusting the label. A volume-accurate dose is not a mass-accurate fill unless the density conversion is measured.
- Treating tare as a constant. Barrel and closure weight variation lands directly in the net weight, so tare must be sampled for the actual lot.
- Ignoring density change with temperature. A density measured cold and applied hot can shift the whole net content distribution.
- Skipping the weighing protocol until the FAT. Net content criteria must be agreed before acceptance, not discovered during it.
How to Compare Suppliers on Net Weight Control
When net content is the deciding requirement, the supplier conversation should focus on how mass and volume are reconciled, not on a headline accuracy number.
- Ask how they handle the volume-to-mass conversion. A supplier that asks for density data and its measurement conditions is taking the requirement seriously.
- Ask what they need to set the tare. The barrel, piston, tip and cap weights—and their variation—are inputs to the net weight calculation.
- Ask how fill is verified. Whether the line’s inspection step checks volume, mass (e.g. checkweighing), or both, and how the result is recorded.
- Ask what the FAT will measure. The acceptance test should state the mass target, tolerance, sample plan and method in writing.
- Ask how give-away is controlled. Over-fill is product cost; a credible supplier will discuss the over-fill ceiling, not only the under-fill floor.
How King Pack Supports This Application
King Pack Machinery (Wuxi King-Pack / Wuxi Jingpai Machinery Co., Ltd., founded 2009, with a core technical team carrying more than 20 years of industry experience) treats gel bait net weight control as a measurement discipline rather than a single machine setting. The practical way King Pack supports this application is:
- Volume-to-mass reconciliation. The dosing configuration is set against a measured density at the actual filling conditions, so a volume-based machine is steered toward a mass target rather than left to assume 1 g = 1 mL.
- Tare and gross handling. The weighing approach accounts for barrel and closure tare variation, so net content is calculated, not assumed.
- Agreed acceptance criteria. The net content target, tolerance, measurement method and sample plan are fixed and written down before the acceptance test.
- Inspection that supports the check. The line’s inspection step can be configured around the net content requirement, so the weighing protocol is backed by the equipment rather than left entirely to manual checks.
King Pack does not publish a fixed mass-accuracy figure or apply a veterinary/prefilled-syringe accuracy claim to gel bait. The commitment is to define the target, the tolerance, and the measurement method with the buyer, and to configure and test the line against those agreed numbers.
Conclusion
Grams and millilitres are different controls, and a gel bait sold by weight cannot be reliably filled by a volume-only setting without a measured density, a careful tare, and a weighing protocol. A buyer who pins down the labelled mass, the density at filling conditions, the tare weight, and the acceptance criteria before the FAT turns net content from a vague “accuracy” promise into a recorded, testable result.
Defining net content for your gel bait line? Send your target gram weight, density data and current inspection method to discuss how your gel bait net weight control will be specified and verified.
