
A bottom-up filling machine lowers the filling nozzle into the container and raises it as the liquid level increases. This shortens the free-fall distance and can reduce turbulence, air entrainment, foam and splashing in shampoos, detergents, hand soaps and other foaming liquids. It is also called a diving-nozzle filler. For a complete system, explore our filling and capping line solutions.
When Bottom-Up Filling Helps
| Observed problem | How a diving nozzle may help | What else to check |
|---|---|---|
| Foam rises before the target dose is reached | Keeps the liquid outlet close to or below the rising surface | Upstream aeration, fill rate and product temperature |
| Product splashes onto the bottle neck | Reduces drop height and controls the filling profile | Nozzle diameter, bottle opening and centering |
| Viscous product leaves strings or drips | Coordinates nozzle withdrawal with shut-off or suck-back | Nozzle tip, valve timing and product rheology |
| Filling must slow near the top | Allows a staged fast/slow fill profile | Container geometry, target headspace and control tuning |
| Foam remains after filling | May reduce newly entrained air | Mixing, recirculation and deaeration before filling |
Bottom-up motion is not a universal cure. If air is already trapped in the product, or if aggressive recirculation creates foam in the supply tank, changing nozzle movement alone may not solve the problem. Product and container trials should identify where the air enters the process.
Why Foamy Liquids Overflow During Filling
Foam forms when air is introduced and stabilized by the formulation. Surfactants in shampoos and detergents can hold bubbles for longer than water. Free-fall from a high nozzle position, excessive velocity, sharp flow changes, pump pulsation or aerated product from an upstream mixer can all increase the amount of air in the bottle.
- Drop height: a liquid stream falling to the bottle base creates impact and turbulence.
- Filling velocity: a rate that is stable at the beginning may create foam as the bottle narrows near the shoulder.
- Product rheology: viscosity and surfactant level influence how quickly bubbles collapse.
- Temperature: product temperature can change viscosity and foam behavior.
- Upstream handling: mixing, transfer pumping and tank return lines may introduce air before the filler.
How a Diving-Nozzle Filling Cycle Works
- The container is positioned and confirmed beneath the nozzle.
- The nozzle descends to a programmed starting height while avoiding contact with the container.
- Filling begins at a controlled rate near the base of the bottle.
- The nozzle rises according to time, volume or a programmed motion profile as the liquid level increases.
- The filling rate may slow near the shoulder or target level.
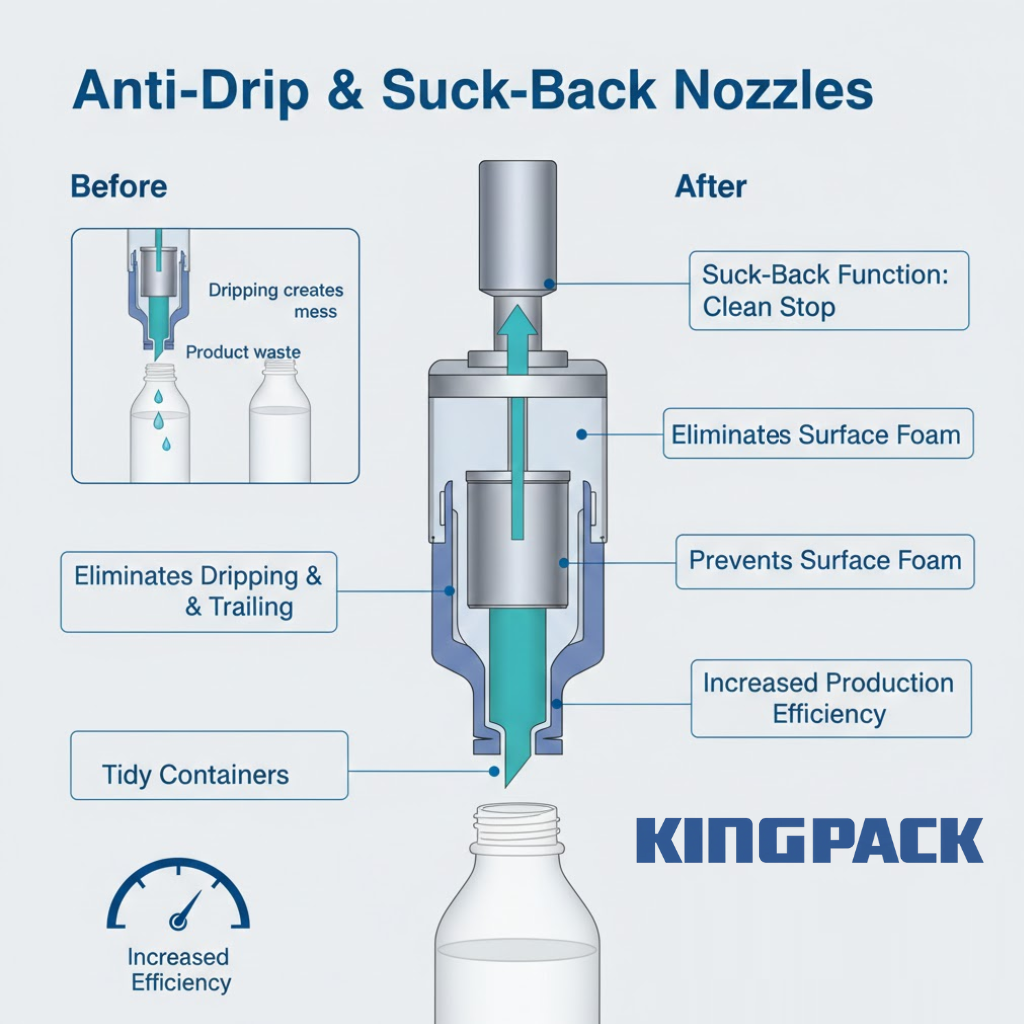
- The valve closes, and an appropriate cut-off or suck-back action limits tailing and drips.
- The nozzle withdraws fully before the bottle moves to capping.
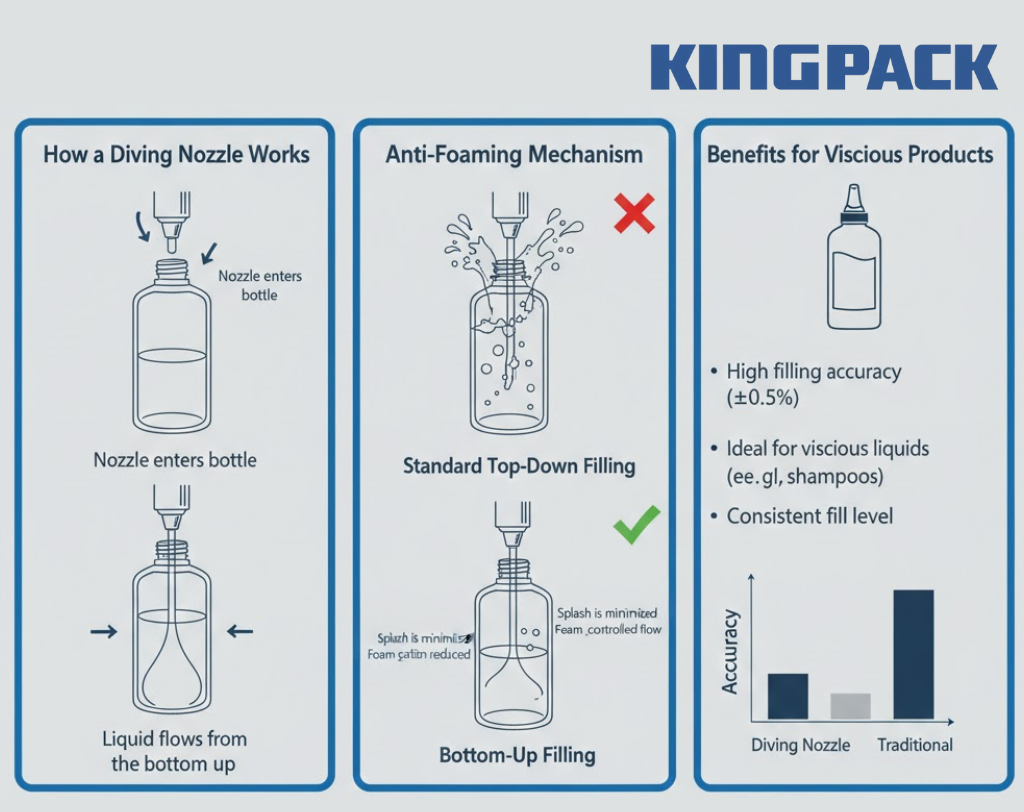
The rise profile must be tuned to the bottle shape and product behavior. If the nozzle rises too quickly, free-fall and foaming return. If it rises too slowly, the nozzle may be submerged too deeply, increase back pressure or carry product on its exterior.
Bottom-Up vs Top Filling vs Overflow Filling
| Method | Typical strength | Important limitation |
|---|---|---|
| Fixed top filling | Simple arrangement for products that do not foam or splash excessively | Long drop height can create turbulence in some products |
| Bottom-up or diving-nozzle filling | Controls drop height and supports staged filling profiles | Requires coordinated nozzle motion, container centering and clearance |
| Overflow filling | Produces a consistent visible level in suitable rigid containers | Recirculation and return flow can be unsuitable for some foamy or sensitive products |
The machine type should follow the acceptance criteria. If net content is the priority, define a gravimetric or volumetric verification method. If shelf appearance is the priority, visible level and foam-settling time also matter. Some lines combine controlled diving motion with piston, pump or flowmeter dosing.
Nozzle, Valve and Motion Design
Nozzle diameter and shape
A larger product path can reduce velocity for a given flow rate, but it must fit through the bottle opening with sufficient clearance. Nozzle geometry should also avoid trapping product and support cleaning. The smallest bottle neck often sets the design limit for a multi-format line.
Shut-off and suck-back
Positive shut-off nozzles, string-cutting features or controlled suck-back can reduce tailing, depending on the product. Excessive suck-back may pull air into the product path or make the next dose unstable, so it should be established during trials rather than treated as a fixed universal setting.
Servo motion and fill profiles
A servo-driven lift can store position and speed recipes for different containers. Useful parameters include starting height, fast-fill range, transition point, slow-fill rate, final height and withdrawal delay. Recipe control improves repeatability, but each product and bottle combination still requires validation.
Upstream Mixing, Transfer and Deaeration
A filler cannot remove every bubble created upstream. Check whether the agitator pulls a vortex, whether a return line discharges above the liquid surface, and whether the transfer pump introduces excessive shear or pulsation. Adequate hold time or vacuum deaeration may help some formulas, but must be evaluated against product stability and production requirements.
For products prepared under vacuum, coordinate the mixing vessel and filler rather than optimizing them separately. See how vacuum emulsifying and deaeration systems work.
Accuracy, Foam and Fill Verification
Foam can make visual level checks misleading. Define whether the quality requirement is net weight, delivered volume, settled liquid level or a combination. The test plan should state the product temperature, settling time, sample size and whether results cover start-up, steady production and end-of-batch conditions.
- Measure every filling head separately.
- Record underfill, overfill, overflow, neck contamination and dripping as separate defects.
- Test the smallest bottle neck and the most foam-prone formulation.
- Confirm performance after a normal stop and restart.
- Evaluate capping and labeling after filling, not only the filler in isolation.
Applications for Bottom-Up Filling
Potential applications include pet shampoo, human shampoo, shower gel, liquid hand soap, laundry detergent, dishwashing liquid and other products that foam or string during filling. Suitability depends on the real formulation, container and required output. Solvent-based, hazardous or highly reactive products need a separate materials and safety assessment.
Information to Include in Your RFQ
- Product samples, viscosity range, density, temperature and foaming behavior
- Smallest and largest bottles, neck openings and physical samples
- Fill range, required net-content tolerance and visible-level requirement
- Target accepted output for each bottle and product
- Number of product and format changes per shift or week
- Cleaning method, utilities and available line space
- Capping, sealing, labeling, coding and inspection requirements
Factory Acceptance Test Checklist
Run the most foam-prone product in the most difficult bottle, not only an easy reference liquid. Record sustained accepted output, fill results by head, foam height, settling time, overflow, drips, bottle-neck contamination, restart behavior and changeover time. Confirm that nozzle motion remains clear of the bottle and that filled containers can be capped and labeled without contamination.
Bottom-Up Filling Machine FAQ
Does bottom-up filling eliminate all foam?
No. It can reduce air entrainment caused by drop height and turbulence, but foam may also come from mixing, transfer, recirculation or the formulation itself.
Can a diving nozzle fill viscous products?
Often yes, when the dosing system, product path, nozzle and motion profile are designed for the viscosity. Thick products also require effective cut-off and cleaning access.
Is an overflow filler the same as a bottom-up filler?
No. Overflow filling controls a visible fill level through a return path. Bottom-up describes nozzle movement and may be combined with different dosing technologies.
How fast can a bottom-up filling line run?
Speed depends on dose, foam behavior, nozzle count, motion distance, container handling and downstream equipment. Ask for sustained accepted output using the real product and container.
Plan a Foamy-Liquid Filling Line
KING PACK can configure product supply, diving-nozzle filling, capping and downstream packaging around your formulation and bottles. Explore our packaging solutions, review the industries we support, or send your product and container details for a technical proposal.