
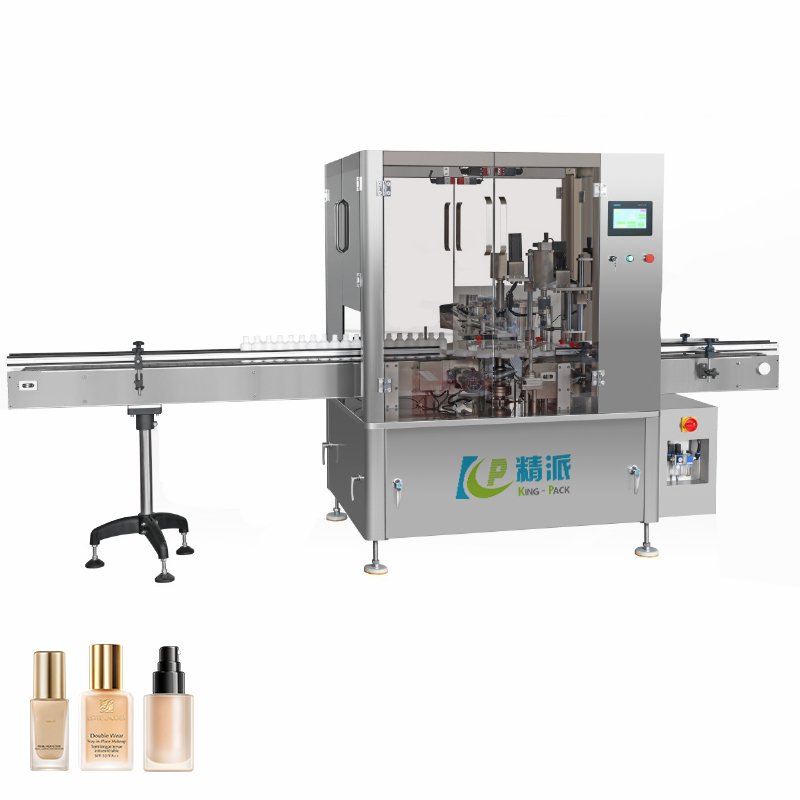
Market forecasts vary by source and definition. The equipment decision should be based on the customer’s formulas, formats, batch sizes, hygiene program and target output rather than a market estimate.
This guide explains common lipstick-filling workflows and selection factors. Temperature, speed, fill tolerance and hygiene features are configuration- and formula-dependent and should be verified with representative trials.
What is a Lipstick Filling Machine?
Definition and Purpose
A lipstick filling machine can melt, transfer, fill, mold or cap when those modules are included in the selected configuration. Confirm the process boundary and format before treating it as a complete lipstick-making line.
Heating, transfer, cooling and capping requirements depend on the formula, container, mold and target process. Temperature control should be established from the product’s validated process.
Quality, contamination control and output depend on the equipment, procedures, operators and quality system. Automation can support repeatability but does not by itself guarantee cosmetic compliance.
Recommended Reading: Emulsifying Mixer Machine for Cosmetics Production – King Pack Machinery
Importance for Cosmetic Factories and Brands
Automation may improve repeatability and reduce manual handling for commercial production. The required level depends on batch size, staffing, format and quality controls.
Scalability, labor and format flexibility should be calculated from the customer’s production plan rather than assumed from the machine category.
Quality consistency builds brand reputation while reducing waste and rework costs associated with manual filling variations.
How Do Lipstick Filling Machines Work? Step-by-Step Workflow of a Lipstick Filling Line
Step 1: Melting Process
The melting temperature must be established from the formula, waxes, pigments and active ingredients. The illustrative 65–85°C range is not universal.
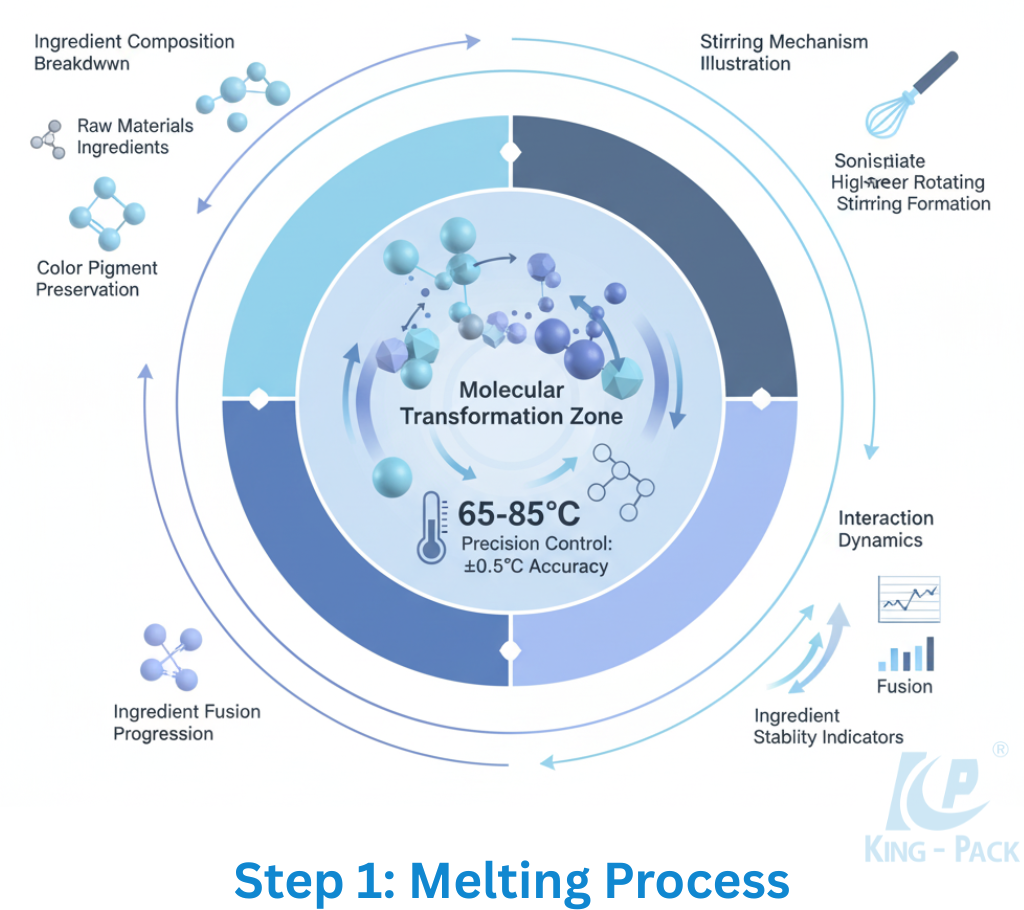
Agitation and temperature control should maintain the required homogeneity without degrading heat-sensitive ingredients. Confirm the sensors, mixing and acceptance criteria for the selected formula.
King Pack can discuss heating and mixing options; actual temperature stability and formula integrity must be verified in trials.
Step 2: Filling Operations
Filling speed depends on number of nozzles, formula, mold, container and configuration. Confirm the tested rate rather than assuming 60 pieces per minute.
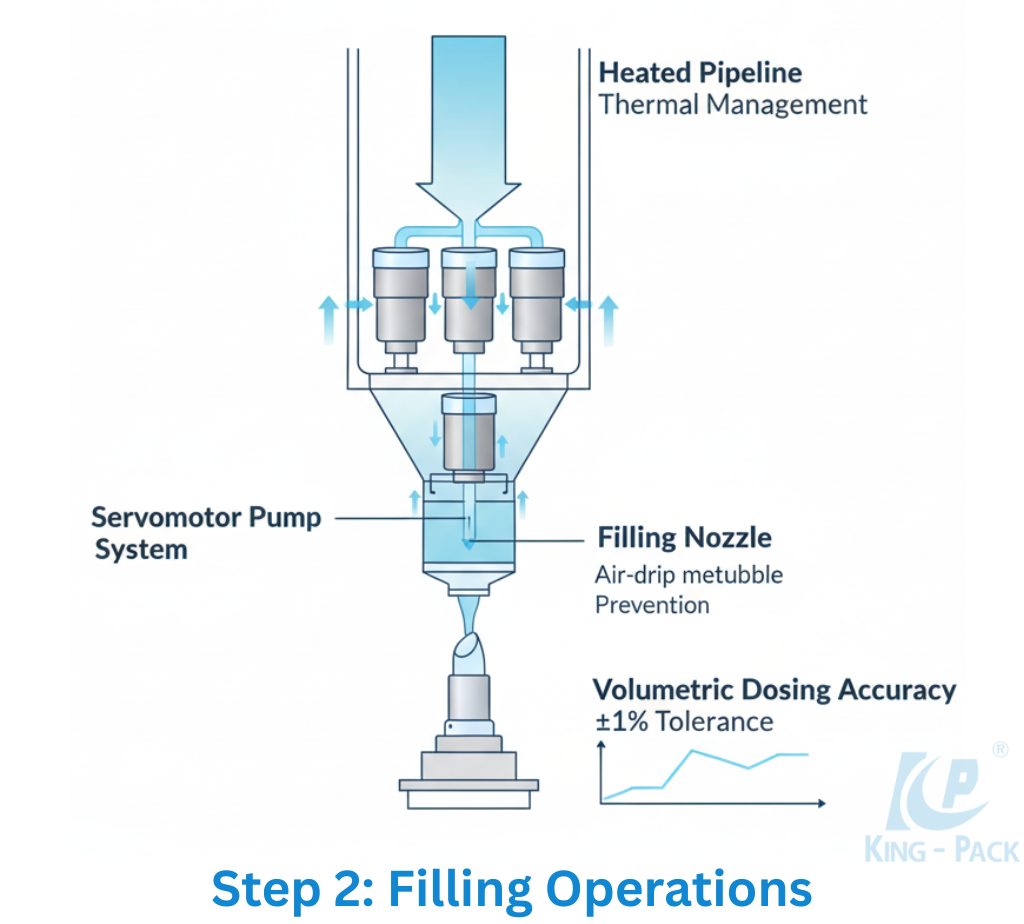
Fill tolerance depends on dosing method, calibration, formula temperature, nozzle and measurement method. Confirm the selected specification instead of assuming ±1%.
Recommended Reading: The Importance of Tube Filling Machine and Tube Sealing – King Pack Machinery
Step 3: Cooling and Solidification
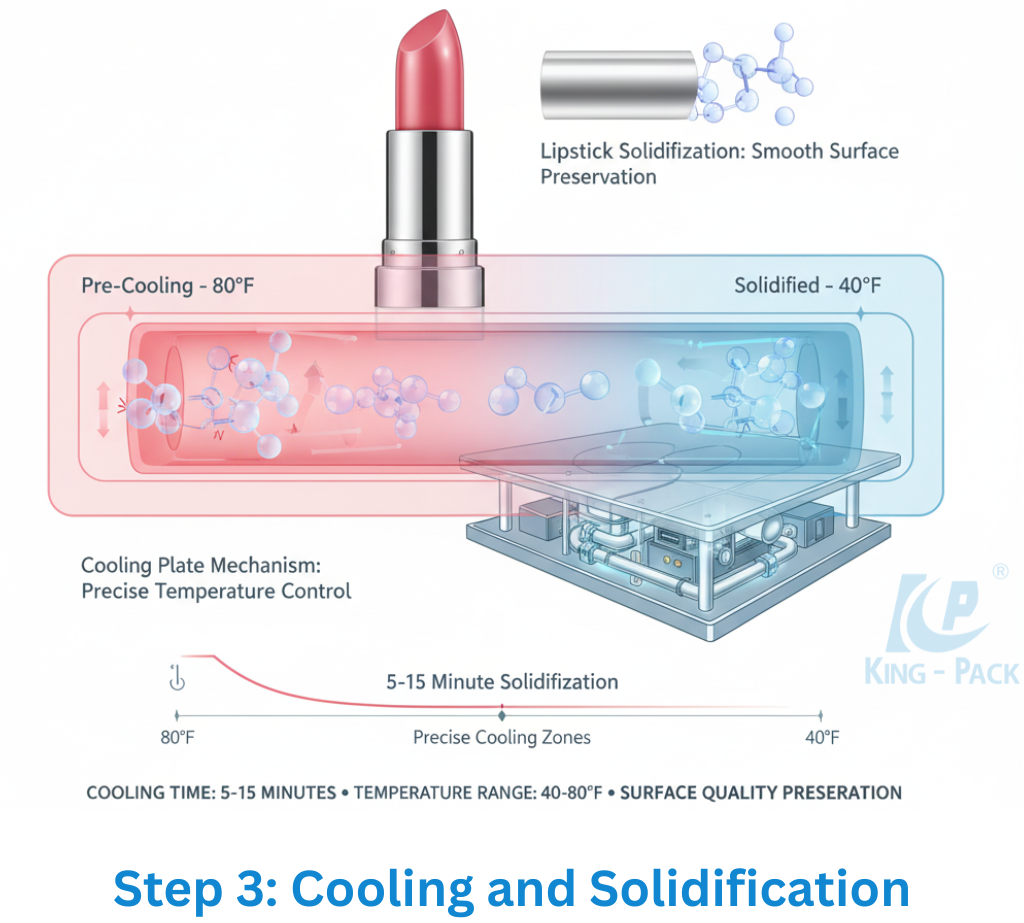
Cooling profile should be selected from formula, mold, geometry and surface requirements. Validate cracking, sink marks and finish on representative product.
Cooling time is formula- and equipment-specific; the 5–15 minute range is illustrative only.
Step 4: Capping and Finishing
Capping and torque depend on the closure, container and machine. Verify alignment, cap damage and seal requirements during trials.
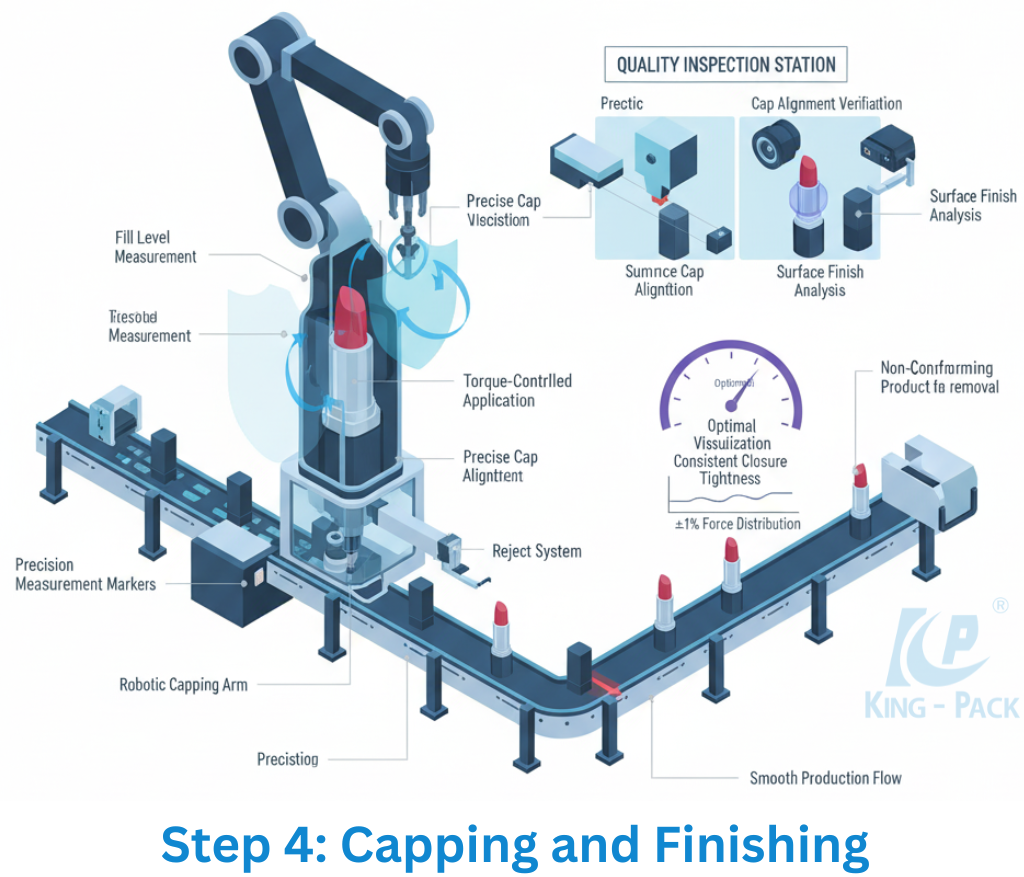
Inspection and reject systems are configuration options. Their coverage, false-reject rate and line response must be validated.
Recommended Reading: Tube Filling Machines: Uses, Types, and Benefits Across Industries – King Pack Machinery
Types of Lipstick Filling Machines
Manual, Semi-Automatic, and Fully Automatic
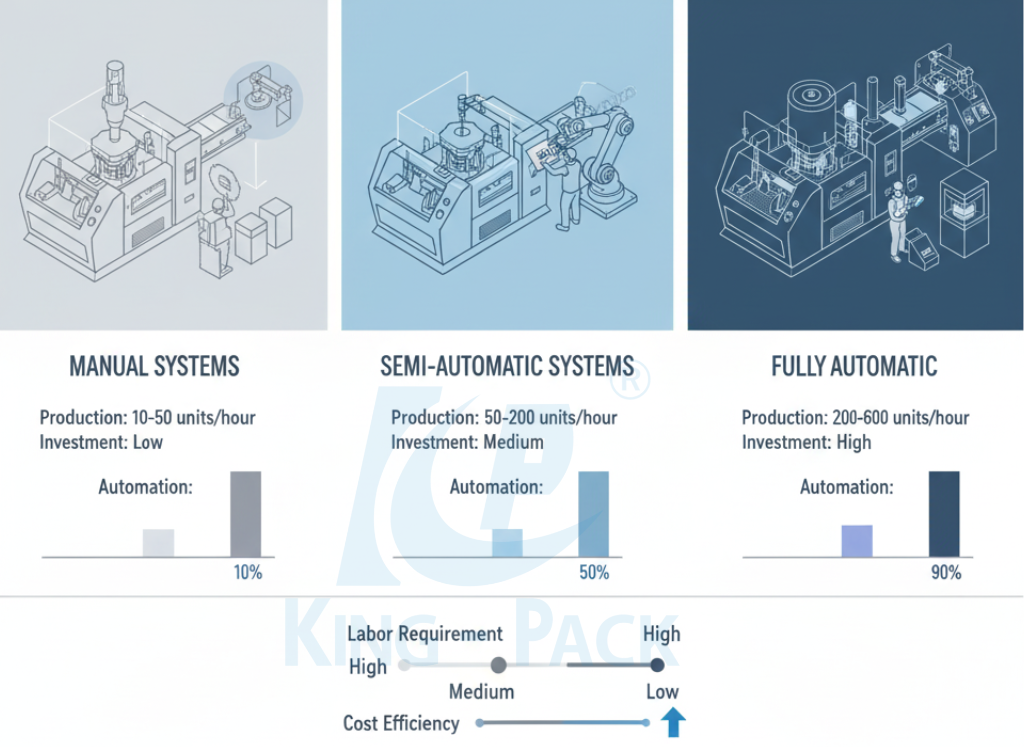
Automation level should be selected from batch size, staffing, hygiene, format and investment. No category guarantees a particular speed or contamination reduction.
- Manual Systems: Basic heating and filling equipment requiring complete operator control for all functions. These systems suit research and development or very small-scale production with limited budgets.
- Semi-Automatic Systems: Combine automated filling with manual material handling and mold operations. They offer a balance between cost and efficiency for medium-scale operations.
- Fully automatic lines may combine handling, filling, cooling and packaging modules. Actual staffing, speed, downtime and quality depend on the selected configuration.
| Machine Type | Production Capacity | Operator Requirements | Initial Investment | Best For |
| Manual Systems | Illustrative capacity range only; confirm the selected machine and batch requirements. | Full operator control | Lowest | R&D labs, start-ups, very small batches |
| Semi-Automatic | Illustrative operator range only; confirm the workflow and quality tasks. | 1–2 operators | Moderate | Small to medium-scale production |
| Fully Automatic | Illustrative capacity range only; confirm through FAT and production trials. | Staffing depends on feeding, inspection, material replenishment, cleaning and quality release. | Capital cost varies with speed, modules, validation and site integration; obtain a project-specific quotation. | Select the automation level from the customer’s output, format and quality plan. |
Tube vs Bullet Lipstick Filling Machines
Tube Filling Machines: Designed for filling lipstick directly into retractable tubes with integrated mechanisms. These machines handle the complete assembly process, including bullet formation and tube integration.
Tube and bullet systems serve different package workflows. Confirm the chosen format, mold, assembly and downstream equipment.
The choice depends on product format requirements and downstream assembly capabilities within the production facility.
Lipstick Filling Machine Construction and Components
Melting Tank: Thermal Precision Engineering
Heating range, sensor accuracy and vessel capacity are model- and formula-specific. Confirm the selected specification and calibration method.
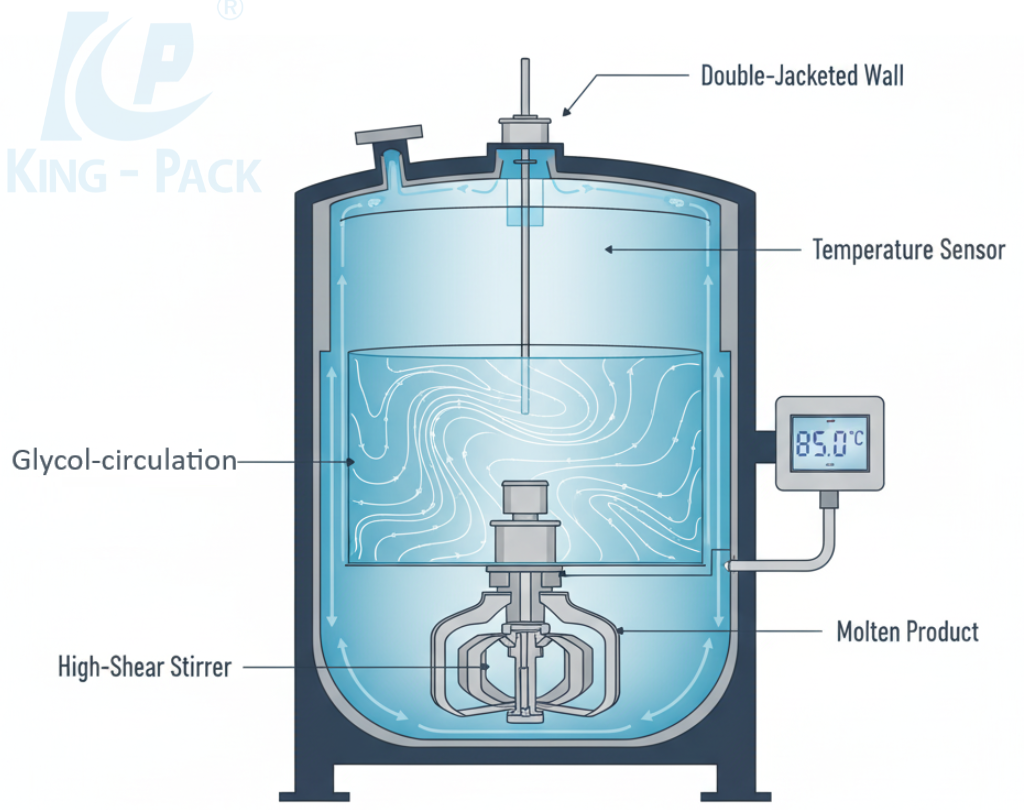
Jacketed heating, PLC profiles and capacity should be specified from the formula, batch size and site utilities.
Recommended Reading: Top 10 Tube Filling Machine Manufacturers Today – Global Leaders in Tube Packaging Technology – King Pack Machinery
Filling Nozzle: Volumetric Precision Technology
Nozzle dosing repeatability depends on the formula, temperature, pump, calibration and test method. Do not assume 0.1 ml accuracy universally.
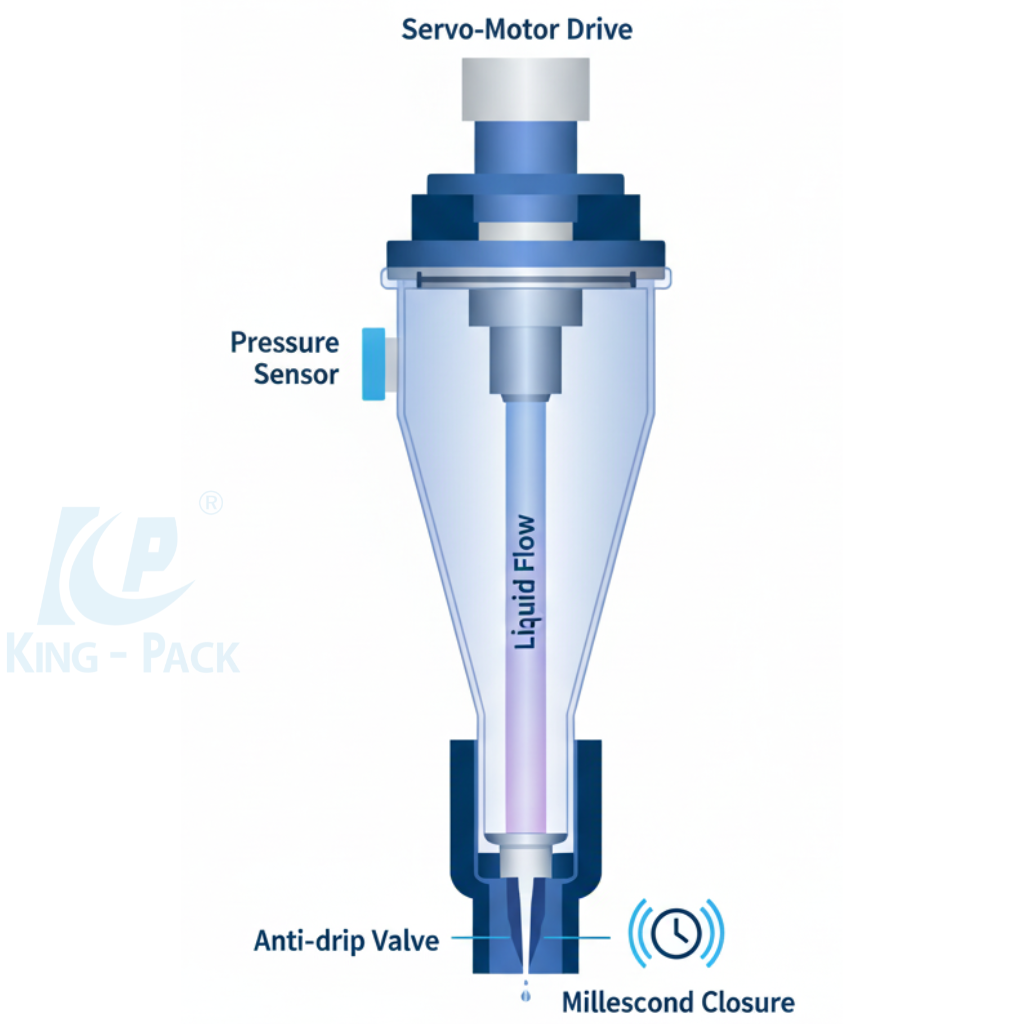
Nozzle manifolds are temperature-controlled to prevent clogging, and vibration dampening reduces splatter for smooth finishes. Options include pneumatic, servo, and hybrid systems.
Mold System: Rapid Configuration Flexibility
Mold-change time depends on tooling, format, cleaning and operator procedure; validate the selected process rather than assuming 30 minutes.
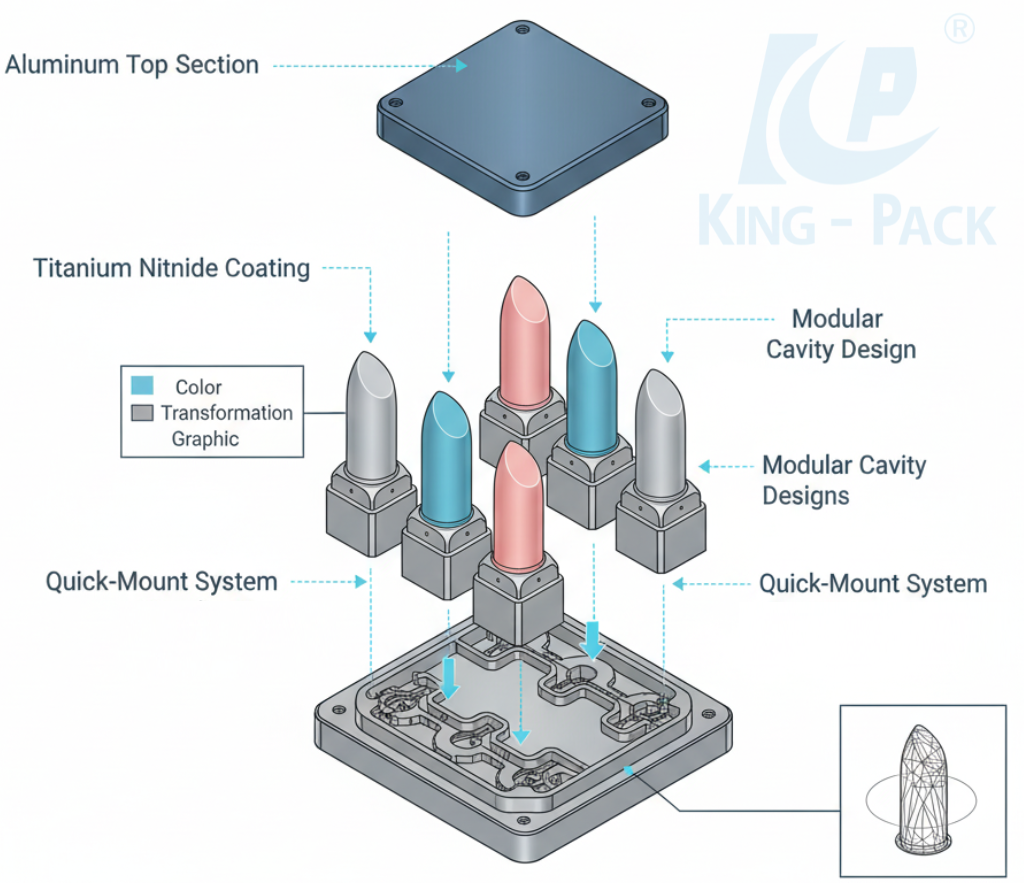
Cooling channels and temperature-responsive alloys regulate solidification. Surface coatings like titanium nitride improve release while quick-mount systems speed up configuration changes.
Cooling Plate: Thermal Gradient Management
Cooling-plate temperature and gradient depend on formula, mold and refrigeration system. Confirm the selected operating range.
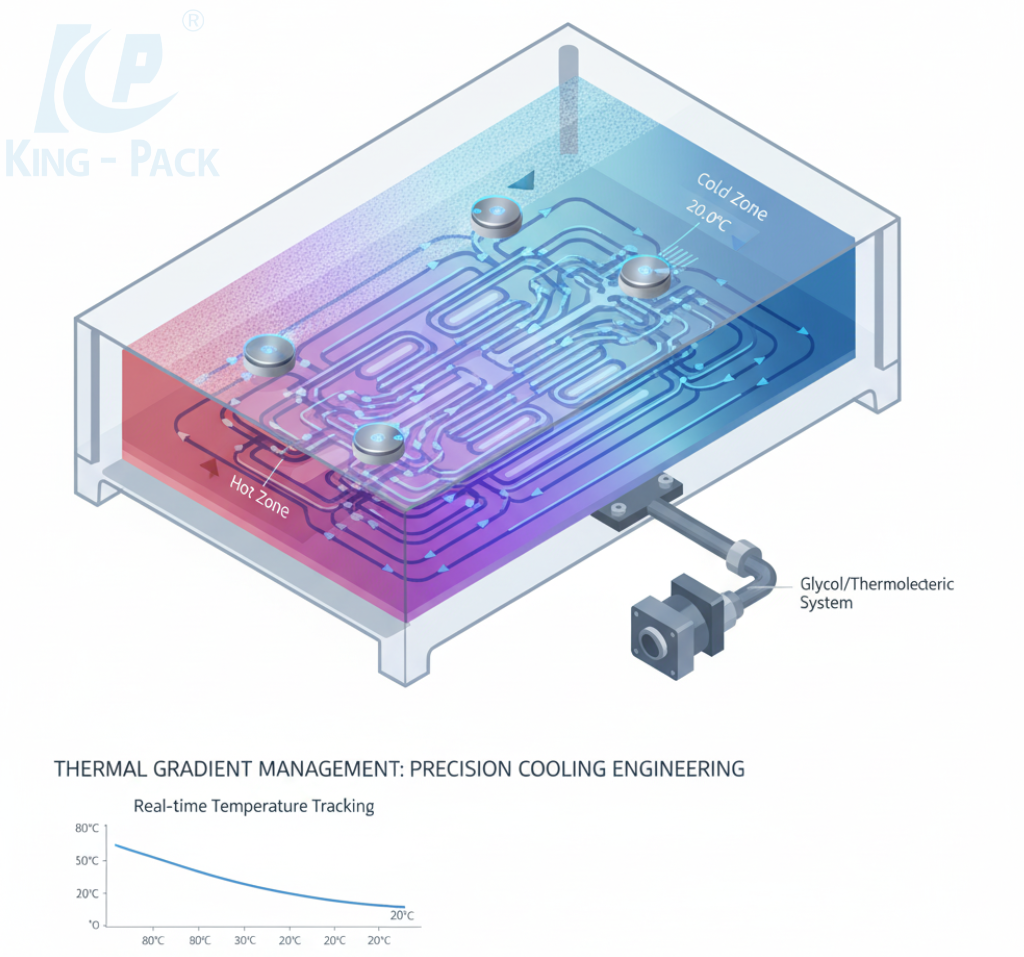
Micro-textured stainless surfaces enhance heat transfer and reduce defects. Integrated sensors track temperature and solidification in real time, optimizing energy use with adaptive cooling zones.
Control Panel: Intelligent Production Management
Touchscreen HMI panels manage recipes, production tracking, and diagnostics. Secure access levels protect operations while data logging supports quality documentation.
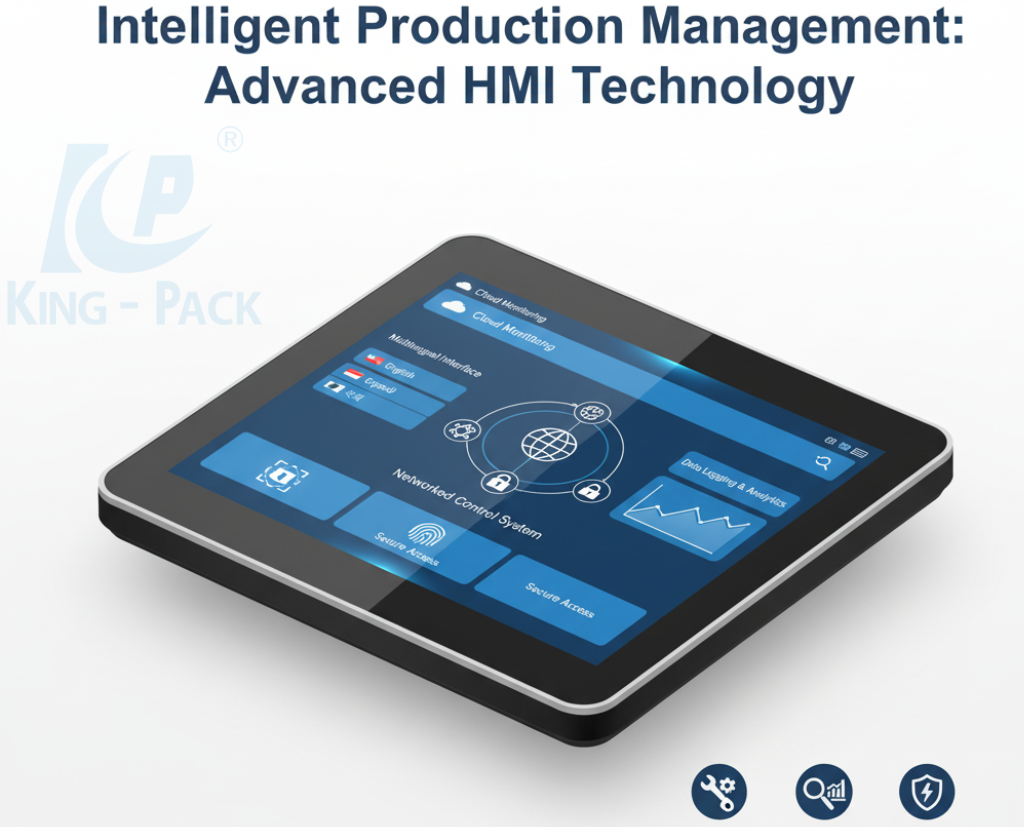
Cloud monitoring, networking and predictive maintenance are optional scope items; confirm cybersecurity, data ownership and validation requirements.
Optional Features: Production Enhancement Technologies
Modern lipstick filling lines can be upgraded with optional systems that boost efficiency and product quality. These technologies streamline finishing processes, reduce manual handling, and maintain consistency across large-scale production runs. By integrating modular add-ons, manufacturers can scale operations without replacing core machinery.
- Labeler speed and data functions depend on the selected model, container and material. Confirm actual rates and coding requirements.
- Automated Capping – Torque-controlled servo systems apply closures with programmable tightness and automatically detect sealing irregularities. Multi-head configurations allow smooth handling of different cap designs.
- Enhanced Cooling – Multi-stage refrigeration systems use programmable thermal gradients to accelerate solidification while protecting surface quality. Energy-efficient modular designs integrate easily into existing production lines.
Materials: Advanced Hygiene Engineering
Contact-material grade, finish and sterilization or cleaning resistance should be specified from the cosmetic product and quality plan. 316L and Ra ≤0.4 µm are not universal requirements.
Seal materials and temperature range must be matched to product, cleaning chemistry and equipment. Antimicrobial additives are not a substitute for sanitation controls.
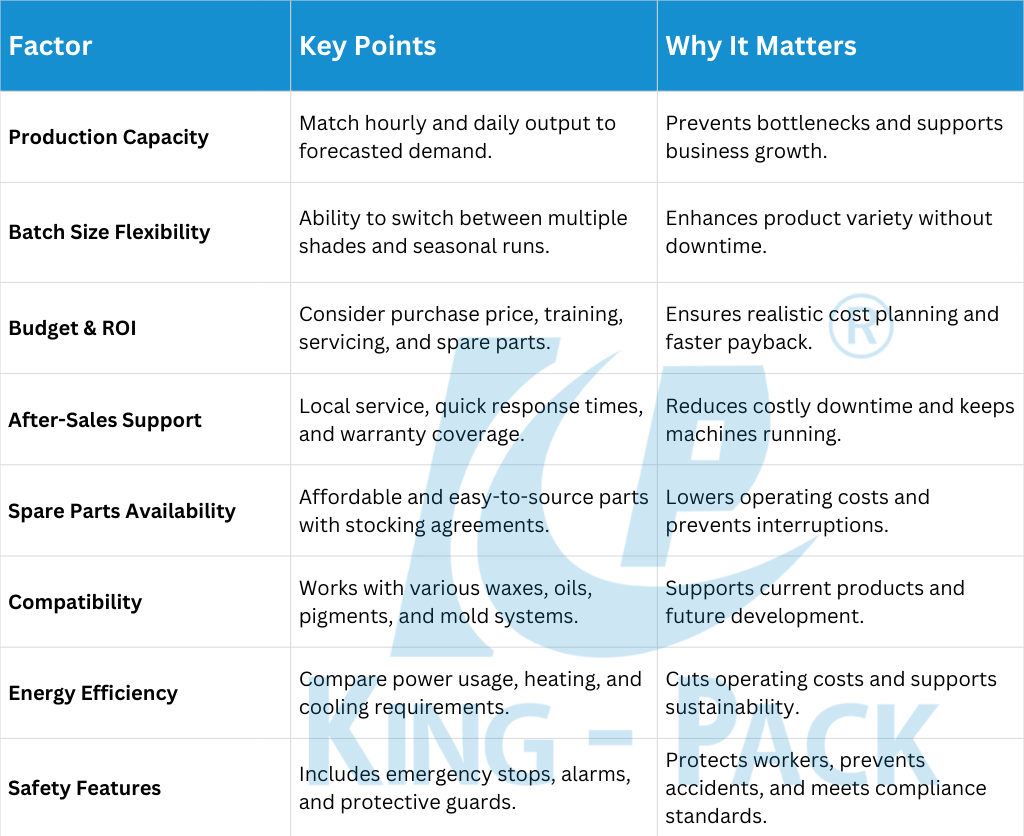
What to Consider Before Buying a Lipstick Filling Machine
Assess batch size, format range, seasonality, staffing, changeover and validation before selecting automation. Servo or vision features are configuration options.
Build ROI from capital, installation, training, labor, waste, downtime, maintenance and verified output data. Do not assume a shortened payback period.
Confirm service coverage, spare parts, tooling, training and changeover procedure in the quotation. Energy and safety benefits are configuration-specific.
Maintenance and Troubleshooting Tips
Regular Cleaning and Sanitization of Tanks and Nozzles
Cleaning procedures and agents should be defined from the formula, contact materials and cosmetic quality system. Daily frequency and solvent choice must be confirmed by the site procedure.
Daily Cleaning Checklist:
- Clean melting tanks and stirring mechanisms
- Sanitize filling nozzles and product pathways
- Inspect cooling plates for residue buildup
- Check temperature sensor accuracy
- Document cleaning procedures and any issues
Nozzle and component cleaning should follow the manufacturer’s instructions and the customer’s material-compatibility and hygiene plan.
Cooling System and Motor Maintenance
Cooling system upkeep includes checking heat-conducting oil levels, cleaning condensers, and verifying cooling process parameters. Proper operation is essential for optimizing production cycles and ensuring high-quality output.
Motor maintenance follows manufacturer specifications, including lubrication schedules, bearing inspections, and checking copper motor connections. Preventive maintenance minimizes unexpected downtime and keeps the production system running efficiently.
Temperature calibration should use traceable instruments and the customer’s approved quality procedure; the interval depends on risk and process.
Conclusion
A suitable lipstick line may support repeatable heating, filling, molding and finishing when configured and validated for the customer’s formula and formats.
Modular features and future scaling depend on the selected equipment, tooling, utilities and maintenance plan. Verify them against the project scope.
Share the formula, format, batch size, target output, heating/cooling requirements and quality documentation needs for a project-specific review and quotation.