 Skip to content

A cream tube filling machine doses creams, lotions, ointments, gels or pastes into preformed tubes and then seals, codes and discharges each pack. Selecting the right machine requires more than choosing a headline speed: the product’s viscosity and air sensitivity, tube material, seal method, fill range, changeover frequency and cleaning plan all affect the final configuration.
For a commercial system, review KING PACK’s tube filling and sealing machine range. The guide below explains which information to prepare before requesting a proposal.
Cream Tube Filling Machine Selection at a Glance
| Requirement | Typical starting point | What to verify |
|---|---|---|
| Laboratory trials or very small batches | Manual or benchtop piston filler; separate sealer | Operator repeatability, cleaning, tube support and seal consistency |
| Frequent product or format changes | Semi-automatic filling and sealing | Change parts, recipe control, product loss and operator steps |
| Continuous commercial production | Automatic rotary tube filler/sealer | Guaranteed output for the actual fill volume, tube and seal process |
| Plastic or laminated tubes | Hot-air or validated ultrasonic sealing | Tube laminate, seal window, cooling, trim and code quality |
| Aluminum tubes | Folding/crimping with batch coding | Fold pattern, internal lacquer, crease control and leak integrity |
| Thick or aerated cream | Servo piston or suitable positive-displacement dosing with controlled feed | Hopper pressure, deaeration, cut-off, nozzle geometry and temperature |
These are engineering starting points rather than universal rules. Final selection should follow trials with representative bulk product, tubes and closures.
What Does a Cream Tube Filling and Sealing Machine Do?
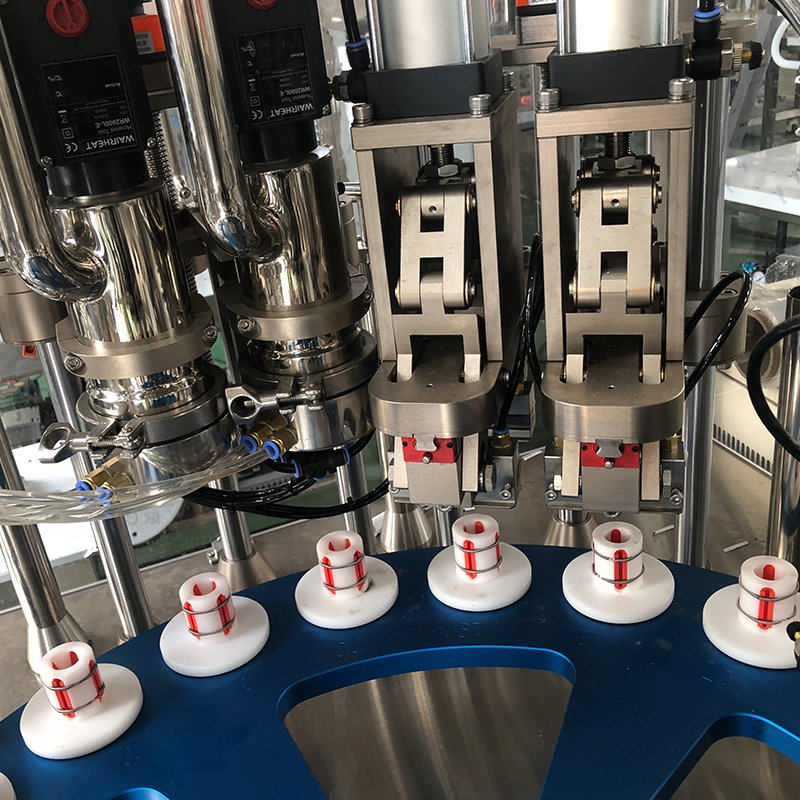
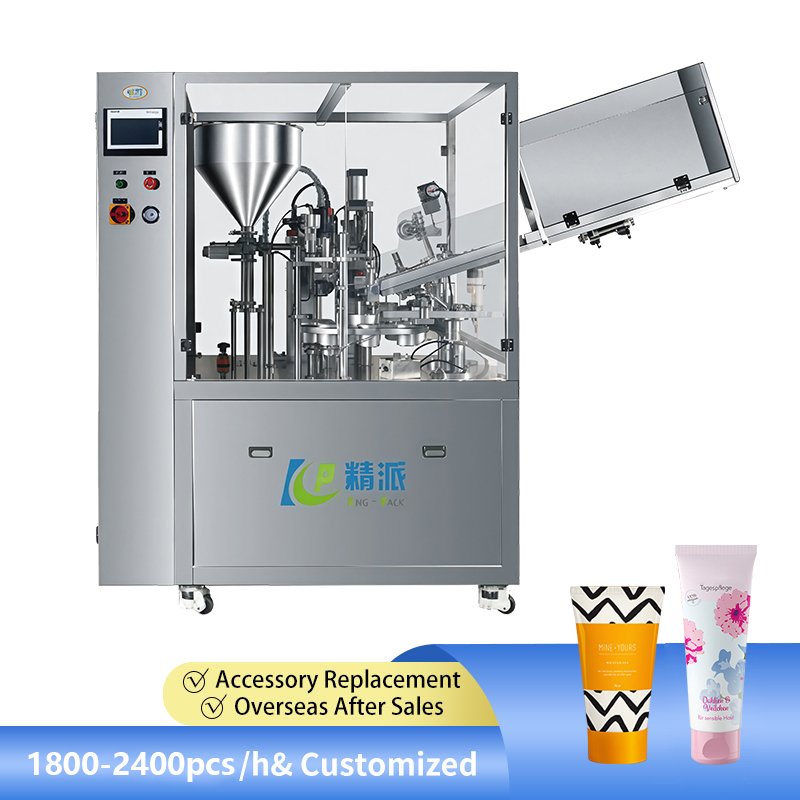
In an automatic line, empty tubes are loaded into holders, oriented by a print-mark or registration sensor, filled from the open tail, sealed or folded, coded, trimmed and discharged. Optional modules can inspect fill weight, tube presence, orientation, seal quality or printed codes. Upstream product preparation and transfer must be designed together with the filler so the cream reaches the nozzle at a stable condition.
Products Commonly Filled into Tubes
- Cosmetics and personal care: face cream, hand cream, sunscreen, cleanser, hair treatment, shaving cream and gel.
- Pharmaceutical and veterinary products: non-sterile ointments, topical creams and gels, subject to the product’s regulatory and contamination-control requirements.
- Oral care: toothpaste and specialist dental gels.
- Food and consumer products: sauces, pastes, adhesives, pigments and other compatible semi-solids.
A machine suitable for a smooth cosmetic lotion may not handle an abrasive toothpaste, stringy gel or paste containing particles. Provide viscosity over the real temperature range, density, particle size, product abrasiveness, sensitivity to shear and air, and required hygiene level.
Manual, Semi-Automatic or Fully Automatic?
Manual and Benchtop Tube Filling Machines
A manual cream filling machine is useful for formulation trials, sample production and very small campaigns. An operator positions the tube and initiates or performs dosing; sealing may be a separate operation. The purchase price is lower, but output and consistency depend heavily on the operator. Confirm that product-contact parts can be cleaned, the tube is supported during filling and the separate sealing method matches the tube material.
Semi-Automatic Cream Tube Fillers
Semi-automatic machines normally automate metering and one or more sealing steps while operators load or unload tubes. They can suit growing brands with moderate batches and frequent changeovers. Compare labor per shift, ergonomic reach, guarding, start-up waste and the number of manual transfers—not only the filling cycle time.
Fully Automatic Tube Filling and Sealing Machines
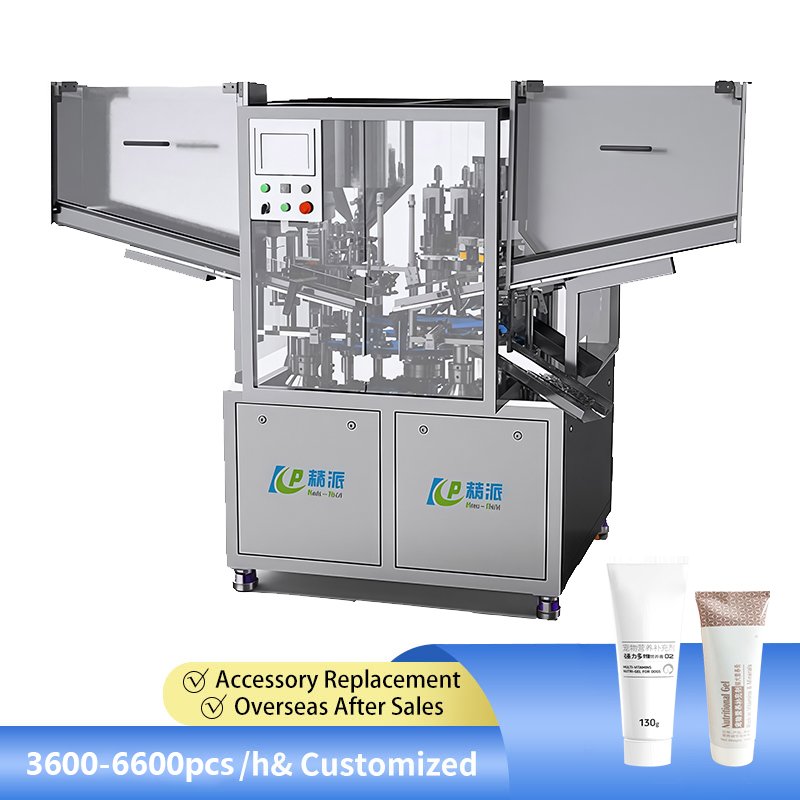
Automatic machines coordinate tube feeding, orientation, filling, sealing, coding, trimming and discharge. They are appropriate when stable commercial output and lower manual handling justify the additional investment. Automatic does not mean operator-free: replenishment, cleaning, format changes, sampling, line clearance and fault recovery still require trained personnel.
How Cream Dosing Works
Most cream tube machines use a piston or another positive-displacement system because semi-solids need controlled displacement and a clean cut-off. A servo piston can provide recipe-based stroke control; rotary-lobe, progressive-cavity or other pump systems may be considered for particular rheology and line layouts. Gravity alone is usually not a suitable primary metering principle for thick cream.
| System | Useful for | Critical checks |
|---|---|---|
| Servo piston | Repeatable doses across common cream and gel viscosities | Cylinder size, seals, temperature, fill range and disassembly |
| Positive-displacement pump | Continuous feed, difficult transfer paths or recipe flexibility | Slip, shear, pressure, pulsation, cleanout and hold-up volume |
| Pressurized or heated hopper | Products that need stable feed pressure or temperature | Air entrainment, residence time, temperature uniformity and level control |
| Vacuum/deaeration support | Products prone to trapped air or voids | Whether it is used for product preparation, filling assistance or both |
The nozzle should enter far enough to keep the tube wall and sealing zone clean. Shut-off, suck-back or diving motion can reduce strings and drips. For aerated products, the complete route from mixing vessel to hopper and nozzle must be evaluated; improving only the filler may not remove bubbles already present in the bulk.
Tube Material Determines the Sealing Method
Plastic and Laminated Tubes
Hot-air sealing heats the inside of the open tail, after which jaws compress and cool the material. Ultrasonic sealing uses vibration and pressure at the seal interface and can be useful where a validated process window supports the selected laminate. Neither method should be chosen solely by machine speed: wall construction, barrier layer, printing, tail contamination and required seal appearance all matter.
Aluminum Tubes
Aluminum tubes are closed mechanically by folding and crimping rather than by hot-air welding. Common projects specify a double, triple or saddle fold, plus batch coding in the tail. Confirm the tube’s internal lacquer, wall thickness, nozzle clearance and fold geometry using production-quality samples.
For a more detailed material comparison, see aluminum tubes versus plastic and laminated tubes.
Key Stations and Control Points
- Tube loading and holders: confirm tube diameter, length, stiffness and holder change parts.
- Orientation: print-mark detection aligns artwork and the final seal. Test all print colors and surface finishes.
- Product feed: hopper level, pressure, agitation and temperature should remain inside a validated range.
- Filling: no-tube-no-fill logic, nozzle position and cut-off protect the tube wall and sealing zone.
- Sealing or folding: temperature, pressure, time, cooling or fold setup must match the tube construction.
- Coding and trimming: verify legibility, correct batch data and the finished tail dimensions.
- Inspection and rejection: define rules for missing tubes, orientation errors, fill-weight failures, poor seals and unreadable codes.
Hygiene, Cleaning and Changeover
The hygiene design must fit the product classification. Cosmetic, food and pharmaceutical creams do not share one universal requirement. Review product-contact materials, surface finish where specified, drainability, seals, tool-free removal, cleaning chemicals and the acceptable residual level after changeover.
For cosmetic operations, the U.S. FDA’s official cosmetic GMP inspection checklist highlights clean, well-maintained processing and filling equipment, controlled materials, written procedures and production records. Requirements vary by market and product category; a topical drug can have different obligations from a cosmetic cream.
During a product change, account for the hopper, hoses, pump, cylinder, valves and nozzle—not only the visible filling tip. Measure cleaning time, product recovered, flush volume and the first acceptable tube after restart.
How to Specify Output and Accuracy
Do not compare machines using an isolated “tubes per minute” figure. Ask for guaranteed output with the actual tube diameter and length, fill weight, cream properties, seal method, coding requirement and inspection level. A large dose or long sealing/cooling window can reduce the achievable rate.
Likewise, accuracy should be tied to a product, dose, sampling method and acceptance criterion. Check start-up, normal production and end-of-batch performance. Gravimetric checks can be integrated or performed offline depending on the quality plan.
What to Include in Your RFQ and FAT
- Product list with viscosity, density, temperature, particles, abrasiveness and air sensitivity.
- Tube drawings and samples for every material, diameter, length, print mark and cap style.
- Fill-volume range, target accuracy and allowable product giveaway.
- Required output by format, batch size, shifts and planned changeover frequency.
- Seal appearance, fold pattern, tail code and leak-test requirements.
- Cleaning method, contact-material requirements and line-clearance procedure.
- Electrical standard, utilities, room layout, extraction and downstream interfaces.
- Documentation, recipes, data records, FAT/SAT, training, spares and service expectations.
The FAT should use production-quality tubes and the actual cream when practical, or a documented surrogate that reproduces the relevant viscosity, stringing, aeration and sealing-zone contamination. Run each format long enough to assess fill variation, orientation, seal integrity, code quality, rejects, stoppages and restart behavior.
Frequently Asked Questions
Can one machine fill creams, gels and ointments?
Often yes, but the product range must fit the dosing system, seals, nozzle and cleaning method. Confirm the highest and lowest viscosity at the real filling temperature and test products that foam, string or contain particles.
Can a cream tube filler handle plastic, laminate and aluminum tubes?
A platform may support all three, but it needs different sealing or folding stations and format parts. Plastic and laminated tubes are generally heat- or ultrasonically sealed; aluminum tubes are mechanically folded and crimped.
Is a manual tube filling machine suitable for production?
It can suit laboratory work, samples and very small batches. For routine commercial production, include operator time, separate sealing, inspection, cleaning and consistency when comparing its real cost with semi-automatic equipment.
What causes weak or leaking tube seals?
Possible causes include an unsuitable sealing process, incorrect temperature/pressure/time, contaminated tube tails, inconsistent tube material, poor cooling, worn tooling or incorrect alignment. Seal testing should use the final production tube and product.
Plan Your Cream Tube Filling Line
Start with the product and tube samples, then define the dosing, sealing, inspection and changeover requirements as one system. Explore KING PACK’s automatic tube filling machines, review our industry solutions, or send your cream and tube specifications for a line recommendation and FAT plan.
