 Skip to content

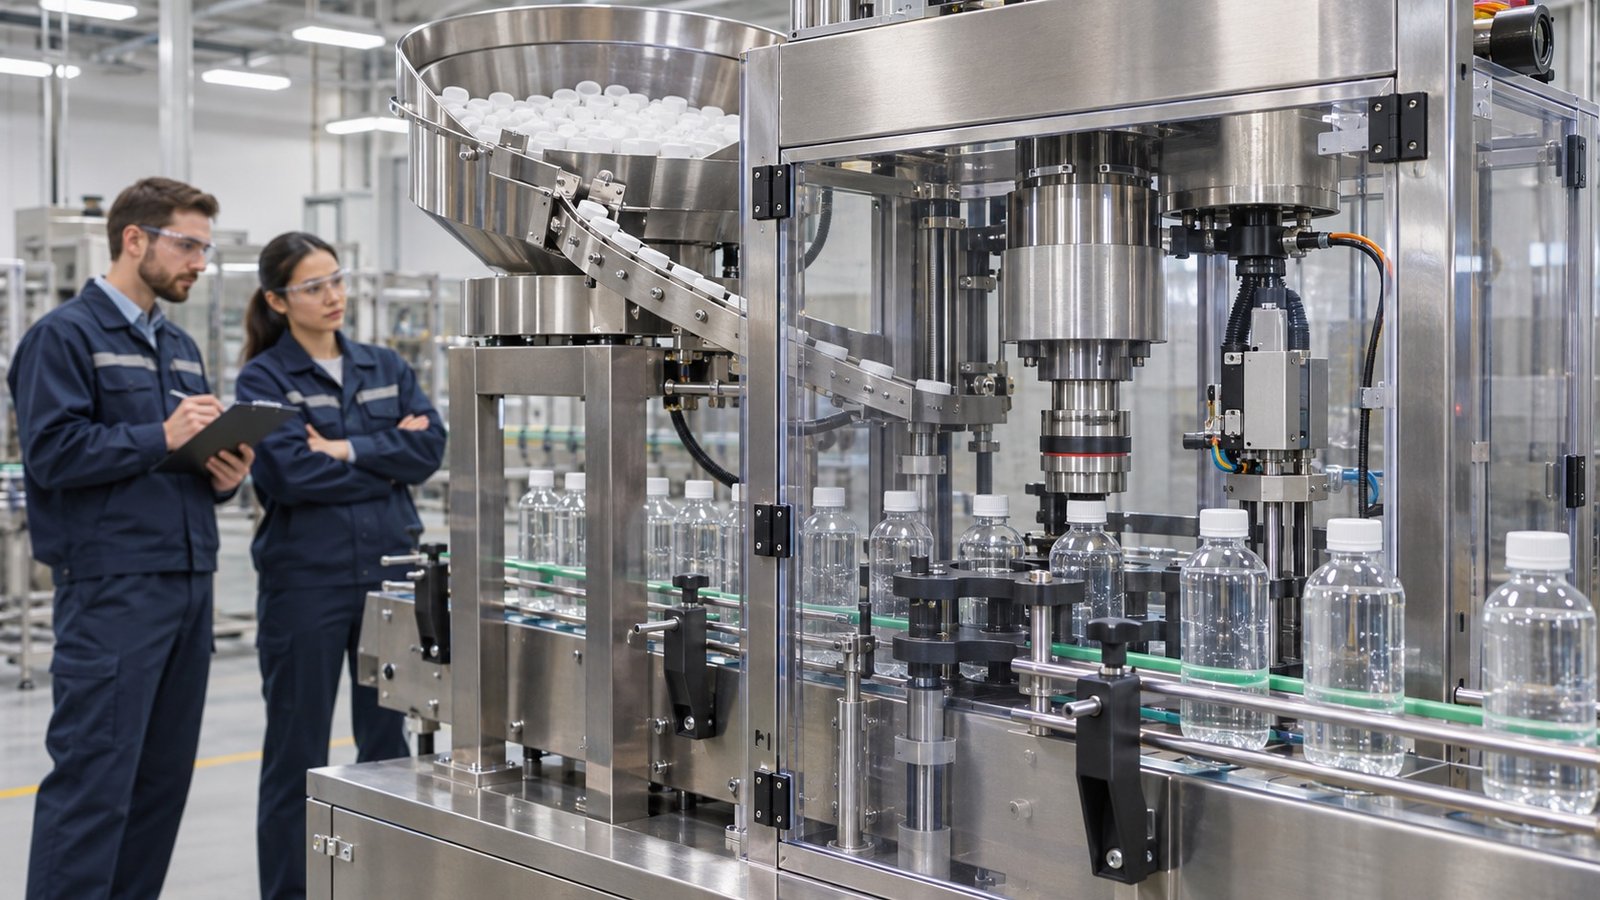
Bottle capping machines close filled containers with a controlled, repeatable operation. The correct choice depends on the cap and bottle geometry, closure torque or application force, product behaviour, changeover frequency, and the way the capper receives and transfers bottles. A useful project brief compares chuck capping, spindle capping, snap capping, press-on operations and specialised closure systems against the actual package rather than a generic speed claim.
Answer first: what should a buyer compare?
Compare the closure type, cap presentation, bottle stability, torque-control method, format range, inspection logic, utilities, and upstream/downstream interfaces. Ask the supplier to state which bottle, cap, line speed definition, and test conditions support the proposal. A capper that works on one neck finish may need different tooling and settings for another.
| Decision area | What to define | Evidence to request |
|---|---|---|
| Closure | Cap type, thread, liner, tamper band and application motion | Cap and bottle drawings, samples and closure instructions |
| Quality | Torque window, presence check, cap height and cross-thread criteria | Inspection method and agreed test record |
| Changeover | Format range, tooling and adjustment method | Change-part list and setup checklist |
| Integration | Conveyor height, pitch, signals and reject handling | Layout, interface list and sequence description |
Common bottle capping machine types
Spindle cappers
Spindle cappers use rotating wheels or belts to drive a cap onto the bottle. They are often considered when the cap format and bottle presentation support continuous handling. The proposal should explain cap feeding, bottle guide control, spindle adjustment, torque setting and how different cap diameters are managed. Do not assume one adjustment suits every closure.
Chuck cappers
A chuck capper applies the cap from above with a chuck that matches the closure. This approach can be useful when controlled vertical application and a defined torque are important. Buyers should confirm how bottles are located, how caps are picked and how the chuck is changed for different formats.
Snap and press-on cappers
Snap or press-on closures need the correct downward force, bottle support and cap alignment. The closing action should be verified with actual cap tolerances because excessive force can damage the package while insufficient force can leave the closure incompletely seated.
Specialised closure stations
Some packages use pumps, trigger closures, droppers or other components that combine insertion and tightening. These systems require a detailed component sequence and may include orientation, presence detection and separate torque or seating checks.
Torque control is a package requirement
Torque is not just a number on a machine setting. The practical window depends on the cap, liner, thread, bottle neck, product contamination, temperature, material and the buyer’s opening and sealing requirements. Define how torque will be measured, where the test is taken, how often samples are checked, and what happens to packs outside the agreed range.
During factory testing, use representative bottles and caps when possible. Record the closure revision, machine settings, test sequence, observed torque results if measured, cap presence, bottle stability and any open points. A FAT record should not imply site acceptance if the downstream conveyor, product residue or local utility condition has not been tested.
Cap feeding and bottle presentation
A capper can only control torque when the cap reaches the application point in a consistent orientation. The cap feeder, chute, elevator or bowl should be matched to the closure geometry. Discuss cap bulk properties, liner behaviour, tamper-band clearance and the risk of upside-down or nested caps. The bottle infeed should provide stable pitch and prevent bottles from rotating or leaning before the closure is applied.
Common interface problems include a bottle arriving before the cap is ready, a cap chute that creates back pressure, insufficient accumulation before the capper, or a discharge conveyor that pulls a newly capped bottle sideways. Include sensors and signal ownership in the line layout rather than treating them as minor details.
Changeover and cleaning considerations
Changeover should be described as a sequence of tasks: stop and isolate the machine, remove or release format parts, install the new bottle guides and cap tooling, adjust the application station, verify sensor positions, run trial containers, and record the approved settings. If a line handles different products, the cleaning or wipe-down method should address cap contact parts, guides and areas where product may accumulate.
- List every format-dependent guide, chuck, spindle setting or cap chute part.
- Identify which adjustments are scale-marked, recipe-controlled or manually verified.
- Define how the operator confirms correct cap and bottle matching before restart.
- Include a first-off inspection for cap presence, seating, height and torque where applicable.
Line integration checklist
| Checkpoint | Question to close before order |
|---|---|
| Upstream filler | Are bottles stable, correctly spaced and free of product on the neck? |
| Cap supply | How are caps orientated, replenished and protected from damage? |
| Inspection | How are missing, tilted, loose or wrong caps detected and rejected? |
| Downstream transfer | Does the discharge preserve cap seating and connect to labelling or packing? |
| Documentation | Are settings, drawings, parts and test records included in handover? |
Factory acceptance and shipment preparation
Agree the FAT scope before testing starts. It should identify the equipment configuration, bottle and cap formats, sequence, safety checks, inspection points, documents and open-point process. Shipment inspection should verify that format parts, guards, sensors, manuals and spare items are labelled against the packing list. Before installation, prepare the conveyor elevation, electrical supply, compressed air if required, operator access, lifting route and connection points.
Frequently asked questions
How do I choose between spindle and chuck capping?
Start with the closure geometry, bottle stability, torque requirement, format mix and desired application motion. The supplier should confirm the choice through component trials rather than selecting solely from a catalogue description.
Is capping speed the same as finished-line output?
No. Practical output can be limited by cap feeding, bottle accumulation, inspection, changeover and downstream equipment. Ask how the supplier defines the quoted rate.
Why are torque tests important?
They provide evidence that the closure is being applied within the buyer’s defined window. The method, sampling plan and package conditions should be agreed rather than assumed.
What should be included in a capper RFQ?
Provide bottle and cap drawings, samples, format range, closure requirements, line interfaces, utilities, inspection needs, cleaning expectations and the intended acceptance-test scope.
Conclusion
A bottle capping machine should be selected as part of the complete filling and packaging sequence. Clear package data, controlled torque, reliable cap presentation, documented changeover and a practical FAT plan give the project team stronger evidence than a headline machine speed.
King Pack Machinery can review your bottle, cap, filling-line layout and inspection requirements to prepare a configuration-specific discussion. Request a technical quotation or contact the engineering team with your package details.
