 Skip to content

Choosing among filling machine exporters is less about finding the lowest quoted price and more about proving that a proposed system can be manufactured, tested, shipped, installed, and supported for the buyer’s actual product and package. A credible exporter should be able to translate a written product brief into a defined supply scope, an acceptance-test plan, a documentation package, and a practical handover path.
That distinction matters because a filling machine is rarely an isolated purchase. It must work with the product’s viscosity and foaming behaviour, the container and closure, the available utilities, the operator routine, and the downstream transfer or packaging step. This guide gives procurement, engineering, and QA teams a repeatable way to compare international suppliers without relying on broad claims or an online ranking.
Start with a comparable RFQ, not a supplier shortlist
The most reliable comparison starts before quotations arrive. If each exporter receives a different verbal description, the resulting offers will not be comparable. One supplier may quote filling only, another may include a capper, and a third may assume the buyer will provide product transfer, conveyors, controls, or change parts. A lower number can therefore indicate a smaller scope rather than a better commercial proposition.
Build one RFQ pack and issue the same revision to every bidder. Include the product description, viscosity range if known, tendency to foam or string, fill-volume range, container drawing or samples, closure details, required output definition, utilities, cleaning expectations, available floor layout, and interfaces to upstream or downstream equipment. State whether the intended rate refers to filling heads, capped containers, inspected containers, or saleable output after a defined quality step.
| RFQ input | Why it changes the proposal | What the buyer should provide |
|---|---|---|
| Product behaviour | Influences filling principle, hopper design, nozzles, product path and cleaning approach. | Product data, samples where appropriate, temperature and handling notes. |
| Container and closure | Drives bottle handling, guides, cap feeder, capping head and change-part requirements. | Drawings, tolerances and representative components. |
| Output definition | Prevents one bidder quoting a station rate while another quotes complete-line output. | Measurement point, format mix and operating schedule. |
| Site interfaces | Clarifies responsibility for product feed, utilities, conveyors, inspection and packaging. | Layout, utility information and existing-equipment details. |
Evaluate the technical proposal before the commercial total
A serious proposal should describe the machine configuration, not simply list an attractive headline speed. Check whether it identifies the filling method, wetted materials where relevant, nozzle arrangement, product-transfer assumption, container locating method, closure-handling method, guarding, changeover scope, and any included conveying or inspection interfaces. Where an item is outside supply, it should be stated clearly.
Ask each exporter to state the operating conditions behind any proposed rate. The relevant question is not “How fast can it run?” but “What product, container, closure, sequence and acceptance point does this rate represent?” A stable rate for one format cannot automatically be applied to every SKU. Product rheology, fill level, cap geometry, component tolerances, and downstream dwell time can change the practical result.
Use a comparison sheet that separates confirmed configuration from assumptions. An honest supplier can identify where testing, component trials, or customer data are still needed. That is more useful than a proposal that silently treats open questions as settled.
Use factory testing as evidence, not as a ceremonial visit
A factory acceptance test (FAT) is most useful when its protocol is agreed before the machine is built or before the visit is arranged. It should identify the supplied scope, representatives attending, product or test-medium conditions, package format, operating sequence, safety checks, documents to review, observation method, and the handling of open points. It should also distinguish what can be tested at the factory from what depends on installation conditions at the buyer’s site.
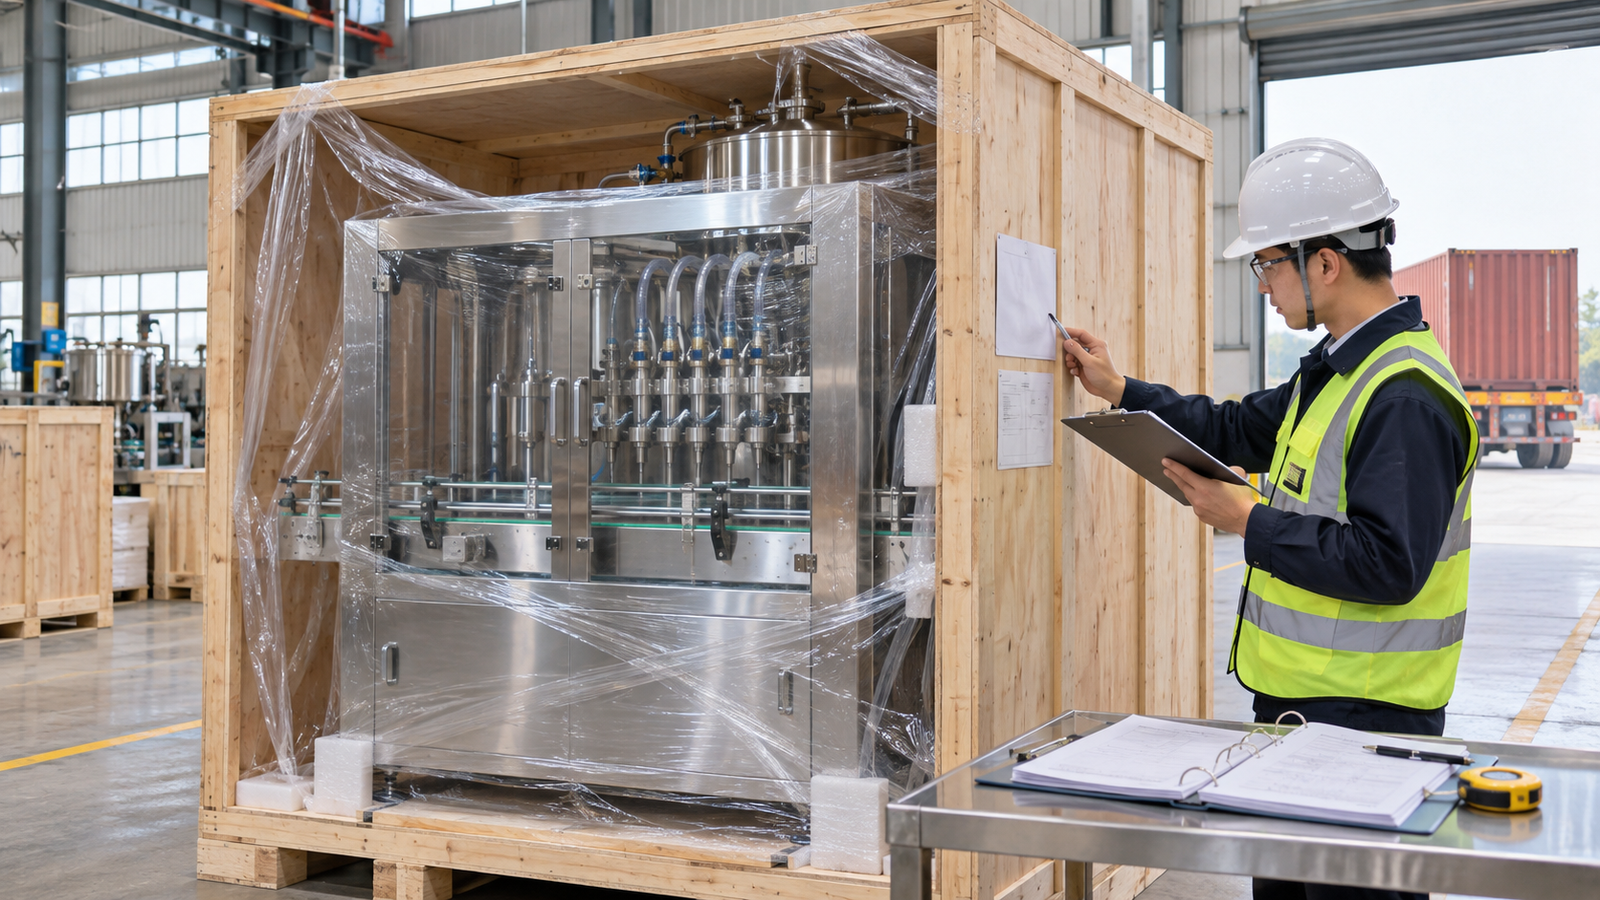
For an exporter comparison, request the proposed FAT outline with the quotation or technical clarification. It does not need to promise a result before product and format details are verified. It should, however, show how the supplier plans to demonstrate the defined equipment scope. A useful FAT record can include the test configuration, observed sequence, change-part identification, safety observations, outstanding actions, and the parties responsible for closing them.
King Pack Machinery can support application-specific factory acceptance testing for the agreed equipment scope. Buyers should still define their own acceptance criteria and provide representative product or components when the project requires them. Read more about a filling machine factory acceptance test when building the inspection plan.
Compare documentation, training, and handover
Equipment availability after shipment depends partly on what the buyer receives before commissioning. Ask each exporter for a document list rather than accepting a generic statement that “manuals are included.” For the defined project, the list may include operating instructions, electrical and pneumatic drawings where applicable, component lists, recommended spare parts, change-part identification, utility requirements, and FAT records. The exact documents should match the agreed supply and the buyer’s quality system.
Training should be discussed in terms of tasks, not merely hours. Operators may need to understand start-up, normal running, changeovers, cleaning steps, alarms, and safe stop procedures. Maintenance personnel may require information about inspection points, wear items, lubrication where relevant, basic fault isolation, and how to request technical support. For regulated or high-value products, QA may also need a defined handover of agreed test evidence.
Inspect shipment preparation and project communication
Export performance is not just a logistics matter. The buyer needs clear packing information, package dimensions and weights when available, documentation timing, shipping responsibility, and an escalation path if a shipment, document, or component issue arises. Ask what will be checked before dispatch and what evidence can be shared. This could include packing photographs, a packing list, component labeling, and a list of outstanding actions. The acceptable evidence should be agreed in the purchase order, not improvised after the machine is ready to leave.
Project communication is equally important. During technical clarification, look for version control: does the supplier identify drawing revisions, assumptions, approved samples, and changes to scope? A supplier who records decisions makes it easier to prevent disagreement between the original quotation, the accepted layout, and the supplied machine.
A practical exporter evaluation matrix
| Evaluation area | Evidence to request | Warning sign |
|---|---|---|
| Application fit | Written configuration linked to product, pack and scope. | Generic description with no assumptions stated. |
| Test approach | Draft FAT protocol, responsibilities and planned records. | Test mentioned without defined product, format or criteria. |
| Engineering control | Layout, interface list, revision history and change-part scope. | Unclear ownership of conveyors, utilities or controls. |
| Handover | Document list, training scope and spare-parts recommendation. | “Full support” with no deliverable list. |
| Export readiness | Packing plan, shipment communication and document timing. | No clarity on pre-dispatch inspection or responsibilities. |
| After-sales process | Named support channel, fault-information requirements and parts process. | Commitments limited to marketing language. |
Questions to ask during a supplier review
- Which exact product and package assumptions define the proposed configuration?
- Which equipment, change parts, conveyors, controls, and interfaces are included or excluded?
- What test sequence can be performed at FAT, and what requires site commissioning?
- What documents will be supplied, in which language, and at what project stage?
- What inputs must the buyer provide before design freeze, testing, shipment, and installation?
- How are design changes documented and approved?
- What information is needed to obtain remote technical support after handover?
Check execution capability before placing the order
A quotation can look complete while the execution process remains unclear. During a supplier review, ask how the project moves from approved scope to design, fabrication, assembly, testing, packing, and handover. The aim is not to prescribe the exporter’s internal workflow; it is to find the control points that protect the buyer’s approved product and package requirements. Useful questions include when the layout is frozen, how component samples are confirmed, who releases design changes, and when the buyer receives the final utility and installation information.
A practical project plan should separate design inputs from buyer approvals. For example, a bottle drawing, closure sample, product characteristics, electrical supply, and site layout may each be needed at different stages. If a supplier needs an input before it can select a nozzle or fabricate a change part, that dependency should be recorded. This helps the procurement team see whether the promised delivery timing depends on customer decisions that have not yet been made.
Review change control and interface ownership
Changes after purchase order are normal in engineered equipment projects, especially when a new container or closure sample reveals a tolerance issue. The important point is that a change is visible. Ask the exporter to confirm how it records revised drawings, specification notes, added change parts, price implications, and delivery effects. A written change record is useful to both parties because it distinguishes an agreed modification from an informal request made during a call or messaging exchange.
Interface ownership deserves the same attention. A filler, capper, labeller, inspection station, or cartoner can each be reliable on its own yet still create a bottleneck at the transfer point. In the RFQ, identify which party supplies each conveyor, sensor, guard, control signal, and product-transfer connection. Where an existing line is involved, request photographs, dimensions, and interface details early. This is particularly important for export projects, where an omitted adapter or utility fitting can delay a site installation even when the main machine has arrived on time.
Assess component traceability and service practicality
Buyers do not need to dictate every brand of component, but they should understand the service model behind the proposed configuration. Ask which components are application-critical, how their part numbers are identified in the documentation, and what information will be needed if a replacement is required. The answer should be connected to the supplied machine rather than a generic assurance that spare parts are available.
During a factory review or FAT, it is reasonable to inspect whether key items can be matched to the agreed configuration: nozzles and product-contact parts, change parts, sensors, drive or pneumatic assemblies where relevant, safety guarding, and the machine identification plate. This does not replace a formal quality audit, and it should not be treated as proof of regulatory compliance. It is simply a practical check that the equipment being reviewed is the equipment that was specified.
The service discussion should also cover the information flow after commissioning. A support team can work more efficiently when it receives the machine serial reference, photographs or video of the issue, current settings, alarm wording, and a clear description of the product and format in use. Buyers should establish the contact channel and expected documentation route before shipment; this is more actionable than relying on a promise of lifetime support without a defined process.
Make the commercial comparison transparent
The final comparison should be made on an aligned commercial basis. Separate the equipment price from packing, freight terms, site services, optional tooling, spare parts, third-party inspection, taxes or duties where applicable, and any installation work that is not included. Each bidder should identify its Incoterms basis and the point at which responsibility changes hands. If a proposal contains allowances, list them separately rather than treating them as fixed scope.
A simple internal scorecard can help cross-functional teams compare evidence without pretending that every criterion has the same weight. Engineering may place greater emphasis on application fit and interface clarity; QA may prioritise records and test protocol; logistics may need packing dimensions and document timing; purchasing may review payment and commercial exclusions. The scorecard is not a substitute for technical judgment. It is a way to record why a chosen supplier met the project requirements and which open points must be closed before an order is released.
Final pre-order checklist
- The approved RFQ revision, quotation revision, and layout refer to the same product and package scope.
- Included equipment, exclusions, interfaces, and change parts are listed in writing.
- FAT conditions, evidence, attendees, and open-point process are understood.
- Required documents, training tasks, packing evidence, and shipment responsibilities are included in the project plan.
- Any site-dependent commissioning or acceptance activity is distinguished from factory testing.
- Commercial terms are compared on the same delivery, packing, optional-scope, and service basis.
Frequently asked questions
How do I compare filling machine exporters fairly?
Issue the same written RFQ to every supplier, then compare defined scope, assumptions, test plan, documentation, shipment preparation, and support process before comparing the commercial total.
What should be included in a filling machine FAT?
The FAT should define the supplied configuration, test materials or conditions, package format, operating sequence, observations, records, open points, and what must be verified later at the installation site.
Is a quoted speed enough to compare suppliers?
No. Ask which product, container, closure, sequence, and measurement point support the quoted rate. A station speed is not automatically complete-line or accepted-output capacity.
What documentation should an exporter provide?
The required set depends on the project, but buyers commonly request operating information, relevant drawings, component and spare-parts lists, utility requirements, and agreed test records. Define the list in the order.
How should shipment inspection be handled?
Agree the packing checks, evidence, labels, packing-list information, documentation timing, and responsibility before dispatch. Record any open actions rather than relying on informal messages.
Conclusion: choose evidence and clarity over broad claims
The right filling machine exporter is the supplier that can make scope, assumptions, testing, handover, and responsibilities visible. That process gives a buyer a practical way to compare proposals, expose gaps before purchase order, and prepare installation with fewer late surprises. It also creates a common record for engineering, procurement, QA, and operations.
King Pack Machinery can review your product, container, closure, target output, and line interfaces to prepare a configuration-specific proposal and FAT discussion. Request a technical quotation with your package and process details, or contact the engineering team to discuss your project requirements.
