
Last reviewed: September 18, 2026.
Container closure integrity (CCI) belongs to the complete filled package, not to a single capper setting or a camera result. A vial can have a centered stopper and still fail an appropriate integrity test; a syringe plunger may look seated while a damaged barrel or seal creates a leak path. Equipment nevertheless matters: it must deliver the selected components consistently, hold an established closing process window, recognize meaningful faults and preserve the records needed to investigate them.
This page covers the equipment side of that decision across vials, prefilled syringes and ophthalmic dropper bottles. It is a cross-format quality-control article, not a replacement for the KING PACK vial-line overview or a specification for any one package's test method. The drug manufacturer must establish package-specific CCI acceptance criteria and validate its chosen method.
Quick answer: Define the package and its critical seal interfaces first. Then map each interface to machine variables such as component orientation, insertion depth, seating force or position, crimp profile, cap torque and stop/restart state. Challenge the process with actual components across justified operating limits, record rejects and trends, and connect sampled packages to a validated CCI method. An equipment sensor can verify its measured feature; it cannot by itself prove microbial-barrier integrity or shelf-life performance.
Define CCI and the Equipment Boundary
Direct answer: CCI is the demonstrated ability of the entire container and closure system to maintain the protection required for the product; equipment controls protect the process that creates that system.
The relevant boundary may include a vial, elastomeric stopper and overseal; a syringe barrel, plunger and tip closure; or an eye-drop bottle, fitment and cap. Product formulation, materials, storage, distribution and use can affect the package. A closing line controls only the formation and handling steps assigned to it. Define whether the intended product is sterile, preservative-free, multidose or nonsterile before choosing tests and alarms.
FDA guidance on container-and-closure integrity testing makes the test method and acceptance criteria package-specific. EU GMP Annex 1 likewise addresses integrity in the sterile-product control strategy. Neither source grants a generic leak-rate limit for every vial, syringe and ophthalmic bottle. Avoid writing a machine URS that promises 'CCI compliant' without naming the package, method and owner of the validation conclusion.
Separate four evidence layers: incoming components, controlled assembly conditions, in-process observations, and validated package testing. If the closing station measures stopper height, for example, its record may show placement was within an approved band. It does not show whether a microscopic path remains at the glass-rubber interface. Connect evidence layers without treating them as interchangeable.
| Evidence layer | What it can establish | What it does not establish |
|---|---|---|
| Incoming components | Specified dimensions, identity and condition | Integrity after filling and closing |
| Equipment parameters | The intended assembly window was applied | Microbial barrier of each package |
| In-line inspection | Visible or measurable faults were rejected | Absence of every leak path |
| Validated CCI test | Performance of sampled package under a defined method | Every untested unit without a justified strategy |
Map the Seal Interfaces Before Selecting Sensors
Direct answer: A useful CCI control plan starts with the physical interfaces that could create a path through the package.
Draw each component in section and identify contact surfaces. For a vial, review stopper flange, vial finish and crimped overseal. For a syringe, include the plunger-barrel interface, tip cap or needle shield and any luer connection. For an eye-drop bottle, include the insert or plug, neck finish, screw-cap liner or tamper element as designed. Record which interfaces are established by machine action and which arrive preassembled.
Bring dimensions and tolerances into a component matrix. Check that feed, guides, tooling and sensors accommodate real lot variation rather than only a nominal drawing. Include surface condition, particles, deformation and missing components as separate risks. An acceptance drawing may define component conformity, but assembled-package performance still needs evaluation with the product and process.
The matrix should name a responsible party for every interface: component supplier, filler, stoppering module, crimper, capper, inspection system or manufacturer. It should also identify an observation, an alarm or reject decision, and the package test that verifies the control strategy. A blank responsibility cell is a procurement issue, not a detail to resolve after FAT.
Identify Critical Machine Variables Without Inventing Limits
Direct answer: Control the variables that affect assembly, but establish their limits through product- and package-specific development rather than a generic machine brochure.
Potential inputs include component presentation, pick-up position, insertion force or motion, final seating height, cap placement, applied torque, crimp-tool geometry, conveyor stability and container support. Also record speed, change parts, recipe, container lot, closure lot and reject timing where they explain variation. The critical subset depends on the actual closure design and failure modes.
Choose sensors by what they truly measure. A vision system may detect a missing cap or tilted stopper. A displacement probe may show insertion position. A torque sensor may show the applied action, not retained closure force. A pressure-decay or other integrity method requires its own suitability and validation. Sensor resolution, repeatability and decision thresholds must be challenged with known good and intentionally defective assemblies.
Set a response for missing data as well as failed readings. Stop, segregate and reconcile affected units if a sensor fails, rejects back up, a recipe changes unexpectedly or an intervention occurs. Record the first potentially affected unit and the point at which good production resumes. An alarm without a defined unit-disposition rule leaves an avoidable gap in the batch record.
| Potential variable | Equipment observation | Required development question |
|---|---|---|
| Stopper or plug position | Height, orientation or force trace | Which deviations correlate with tested package failures? |
| Crimp or cap application | Profile, torque or motion trace | Which range fits the actual components? |
| Transport and support | Jam, tilt or impact record | Can handling damage a sealed package? |
| Reject action | Confirmed removal and count | Where do suspect units go after a fault? |
Control Vial Stoppering and Crimping
Direct answer: Vial CCI depends on a properly matched vial-stop-per-seal system and a reproducible stoppering and crimping process.
At the stopper feeder, check identity, orientation, damage and particulate condition. At placement, verify that each vial is present and supported, the stopper is correctly picked, and the insertion method does not fold or cut elastomer. Partial stoppering can be intentional for a lyophilization process, but final seating after the approved cycle needs its own controlled state and inspection.
At crimping, evaluate cap placement, skirt formation, tool condition, container support and damage to glass or finish. A visually neat cap does not independently establish integrity, and aggressive crimping may damage the system. Trials should include the intended vial and stopper lots, extremes of component tolerance and the approved operating states. The wider vial-line architecture provides context, while this section owns the process-control decision.
Ask for raw machine traces or measured results where available, not just an 'accepted' lamp. A fault challenge should show how absent, high, low, cocked and damaged closures are detected or addressed, how suspect units are segregated, and what happens after a stop or component replenishment. Include glass breakage and particle response in the line procedure.
Control Syringe Stoppering and Tip Closure
Direct answer: A syringe needs control of both the moving plunger seal and the distal tip closure; one station cannot stand in for the other.
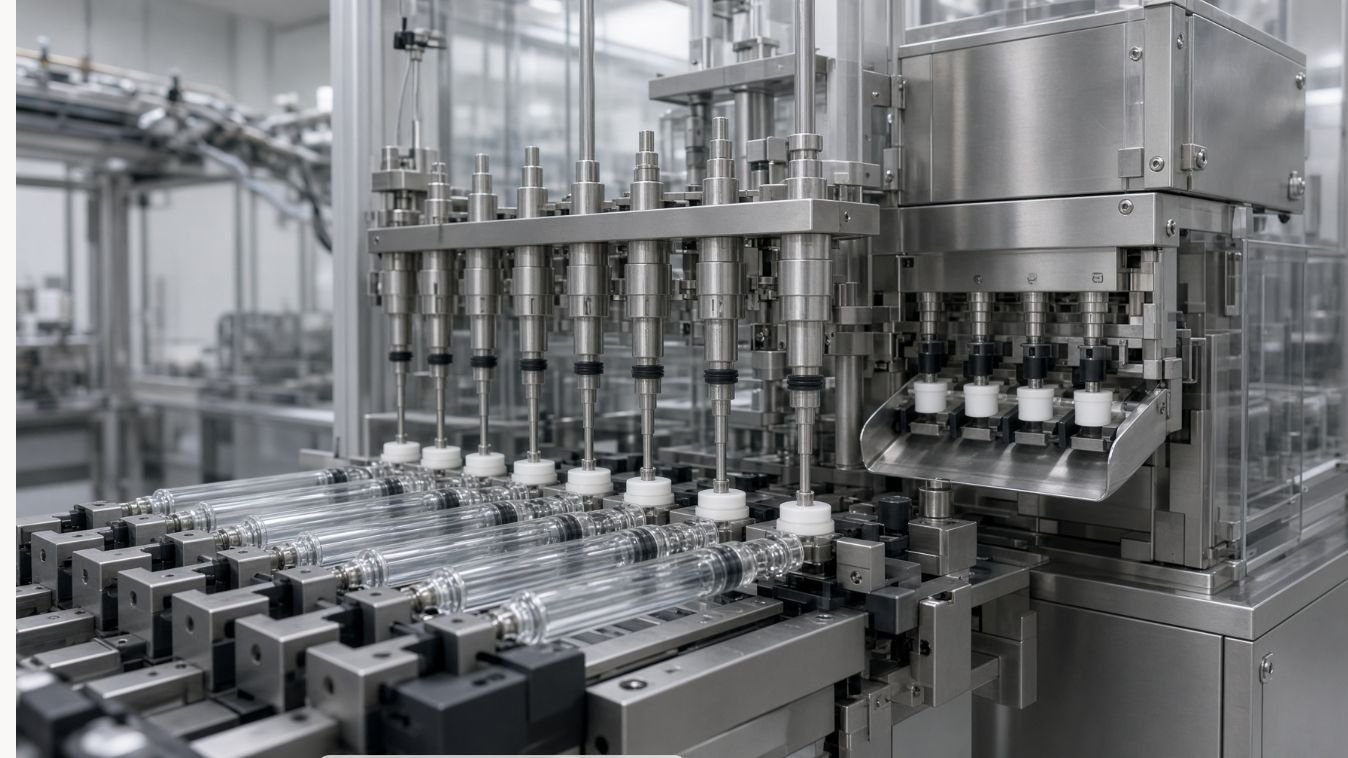
For plunger insertion, map vacuum or mechanical stoppering method, insertion depth, speed, barrel support, trapped air and possible elastomer damage. Product fill level and headspace can affect the insertion operation. Inspect barrel chips or cracks, wrong components and out-of-position plungers. Determine whether the intended container is a glass or polymer syringe and whether its vendor supplies parts preassembled.
For a tip cap, needle shield or luer closure, confirm the correct part, placement, fit and protection of the sterile fluid path where applicable. Use the actual packaging supplier's drawings and approved test method; do not infer integrity from nominal applied torque or insertion depth alone. The existing KING PACK aseptic syringe guide addresses the wider application; this article owns the controllable sealing steps.
Challenge opening and closing states: first unit after a magazine refill, last unit before a jam, restart after a stop, low product level, and all agreed speed limits. Identify whether the machine can trace an individual suspect nest or carrier to its test sample and batch record. If it cannot, define a conservative segregation window rather than assuming all units outside a visible fault are unaffected.
Control Eye-Drop Plugs, Nozzles and Caps
Direct answer: Eye-drop packaging requires closure controls matched to its dispensing design and intended use, not vial or syringe settings copied across formats.
Map whether the bottle has a separate plug, dropper insert, nozzle, cap liner or tamper band. Check neck finish, insert seating, cap thread engagement and cap application under real bottle stiffness and fill conditions. Bottle squeeze behavior, formulation and use pattern may affect package suitability; these issues need product-specific testing beyond the capper itself.
Detect missing or tilted inserts, cross-threading, incomplete caps and damage from excessive application. Define the handoff from filling to insertion so open containers are not stranded during a stoppage. For sterile ophthalmic products, align the closure sequence with the approved aseptic process. For multidose packs, consider the intended opening and recapping behavior; the single-use eye-drop vial discussion illustrates why in-use behavior must not be confused with factory seal formation.
A simple cap-height image may catch gross errors but cannot assess every seal path. Establish a component-specific challenge set and compare in-line detection with the package's validated CCI or functional method. Keep claims narrow: a tested capper setting supports process control; it is not a universal proof of shelf-life or in-use integrity.
Build Inspection, Alarm and Reject Logic
Direct answer: An inspection system is valuable only when its detection limits and reject path are understood and challenged.
List each defect the line is expected to find: missing component, wrong orientation, high or low placement, incomplete crimp, cap misalignment, cracked container, spill or handling damage. For every defect, state the inspection technology, challenge piece, detection criterion and action. Classify what the machine cannot detect so off-line sampling and investigation cover the residual risk.
At FAT, demonstrate alarm generation, machine stop, reject confirmation, full reject-bin handling, counting, blocked ejector, loss of camera communication and restart. Record which unit is at which station when a fault is triggered. A failure of the reject device should not silently return suspect packages to good output. Preserve representative images or traces and equipment settings in the acceptance record.
At the site, verify the exact assembled line and approved recipe. Decide who may bypass a sensor, for what reason, and how product is isolated while it is unavailable. Trend defect rates by component lot, tool set, speed and intervention. An increasing rejected-cap trend can reveal process drift before a formal CCI failure appears, but the trend is a signal for investigation, not an integrity test.
| Fault challenge | Expected line response | Evidence to retain |
|---|---|---|
| Missing or wrong closure | Detect and remove or stop | Image, count and reject confirmation |
| Sensor offline | Alarm and controlled disposition | Event log and affected-unit boundary |
| Reject device blocked | Stop or safe-state response | Challenge record and reconciliation |
| Stop and restart | Defined segregation and first-off check | Timeline and approved release decision |
Connect Line States to CCI Sampling
Direct answer: A CCI sampling plan should represent the process states most likely to change seal formation, not only steady-state middle-of-batch units.
The manufacturer chooses the sample size, method, timing and acceptance criteria through its approved risk assessment and regulatory strategy. Equipment engineering should provide a map of starts, stops, speed changes, closure replenishment, tool changes, interventions and batch end. Label samples with the state, head or station, time, component lots and relevant machine recipe so a result can be investigated.
Build a deliberate bridge between in-line signals and off-line package tests. For example, retain a trace showing the actual stopper-position distribution around a sample set, then examine whether samples from the low and high process edges behave as intended. A pass at one setting does not qualify untested settings. If a method has detection limits, product interference or destructive handling, document those limits in the validation plan.
FDA's CCI guidance explicitly expects method validation specific to the product and package. EU GMP Annex 1 also frames integrity as part of a wider contamination-control strategy for sterile products. The correct sampling plan may differ among vial, syringe and ophthalmic bottle configurations. Do not insert an arbitrary universal frequency into a machine quotation and present it as a regulatory requirement.
Control Changes to Components and Machine Settings
Direct answer: CCI evidence must be reassessed when a change could alter the physical package interface or the process used to form it.
Examples include new stopper or cap supplier, changed elastomer or finish, different vial or barrel tolerance, revised crimp jaw, altered insertion motion, new capper head or a different transport path. A software or recipe change may also matter if it changes timing, force, inspection or reject behavior. Evaluate each change with the component supplier, packaging team, process engineer and quality unit.
Keep a traceable baseline: approved drawings, supplier specifications, incoming checks, tooling, recipe version, setting window, equipment qualification, CCI method and package-validation outcome. A change-control record should identify what remains valid and which bench, line or stability tests must be repeated. Supplier notification alone does not establish equivalence.
Investigate unexpected leak failures against that baseline. Examine failure location, component lot, assembly records, stop/restart events, retained samples and shipping history before changing a setting. Increasing crimp pressure or cap torque without understanding the mechanism could hide one symptom while creating another failure mode.
Write a CCI-Focused URS and Supplier Test Plan
Direct answer: A useful URS asks for controllable package-assembly behavior and evidence, not a blanket promise that a machine 'guarantees CCI.'
Send drawings and tolerance stacks for each container and closure, representative samples, product and process constraints, target line states, desired sensors, approved alarm and reject philosophy, and the owner's proposed test method. Ask the supplier to identify which functions are standard, configurable or not provided. Assign sample ownership, defect creation and test responsibility before FAT.
Request documented component feeding, placement and closing sequences; tool change and identification; recipe and user-role controls; parameter recording; alarm list; reject confirmation; traceability; cleaning and maintenance access; and a challenge matrix. FAT should use agreed samples and defects, with raw observations and open actions. Site qualification then verifies installed conditions, while the manufacturer retains the package-specific CCI validation decision.
A comparison between suppliers should record how each proposed control addresses an identified interface and how it will be tested. Do not score a camera, force sensor or leak tester merely by its presence. Ask for its measurement range, calibration approach, challenged defects, limits and data output under the actual package conditions.
Review Closure Controls with KING PACK
Direct answer: KING PACK can review the closing stations and acceptance evidence around a defined container and closure system.
KING PACK Machinery is a China-based manufacturer of pharmaceutical, veterinary, cosmetic and liquid filling and packaging equipment, with core solutions covering tube filling and sealing, vacuum emulsifying, liquid filling, pet spot-on filling and syringe production systems. The KING PACK pharmaceutical solutions page gives the application context. Equipment selection must remain tied to the actual product and package rather than a generic CCI claim.
For vial, syringe and eye-drop projects, the review can examine component presentation, stoppering or insertion, crimping or capping, inspection, safe states and FAT challenges. KING PACK can identify machine-control options and evidence it can supply; the manufacturer and its qualified laboratory determine method validation, acceptance criteria, stability and final product disposition.
Send component drawings and lots, a representative filled or unfilled sample set, intended operating range, defect list, current package-test method and line-layout constraints through the KING PACK contact page. The practical output is a traceable machine-and-package test plan with clear ownership and unresolved risks.
Frequently Asked Questions
Does a cap-height camera prove CCI?
No. It measures a visible or dimensional feature. Package-specific CCI testing and its validated acceptance criteria are separate evidence.
Is a visually correct vial crimp enough?
No. A correct-looking crimp is one in-process observation; component suitability and package integrity still require appropriate evaluation.
Which syringe seals need review?
Review the plunger-barrel interface and the tip cap, needle shield or luer closure, plus barrel condition and handling.
Can one CCI limit apply to all three formats?
No. The method, detection capability and acceptance criteria must suit the specific product and package system.
What should be sampled after a restart?
Use the approved risk-based plan to identify potentially affected units and capture machine state, timing, components and first-off results.
Does an in-line leak tester eliminate qualification?
No. The instrument and method need suitability, validation and integration with the wider package-control strategy.
Who approves the CCI strategy?
The drug manufacturer and its quality unit own product-specific acceptance, validation, change control and release decisions.
What should a supplier demonstrate at FAT?
Agreed closure-placement and closing challenges, alarms, rejects, records and failure responses using representative components and known defects.