
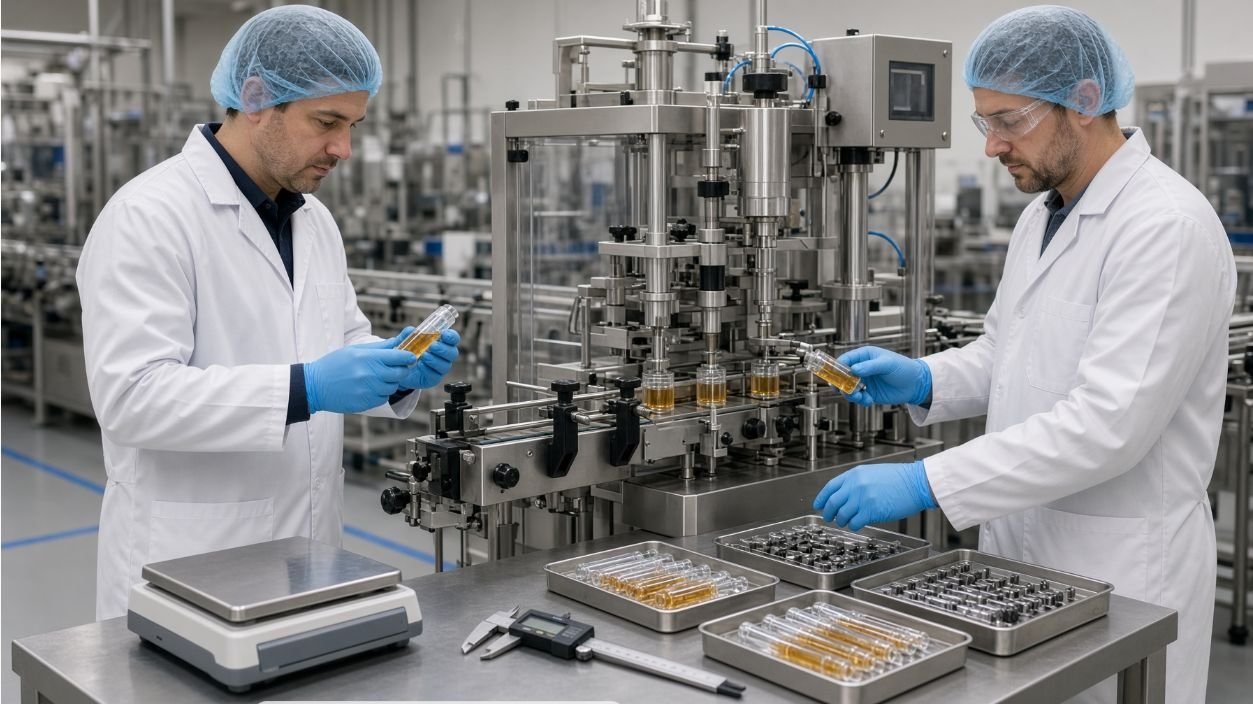
A factory acceptance test is the moment when a gel bait syringe filling line stops being a proposal and starts being a piece of equipment the buyer accepts. The line has been built to a specification; the test is the check that the specification matches the actual product, packaging, and output. When the test is poorly framed, the line can be “accepted” without proving anything that matters, and the first real production run is where the gaps appear. A useful FAT checklist is therefore not a list of machine features—it is a list of risks a buyer wants the test to answer.
This article walks through what a buyer should agree in advance, what to run, what to record, and what to do with deviations so the FAT produces evidence both sides can act on.
Why the FAT Is a Specification Match, Not a Machine Demo
A gel bait syringe filling line is configured around the product, the package, and the output target. A FAT that demonstrates machine features (press a button, watch a cycle) does not prove those features work for the buyer’s paste and barrel. The checklist exists to convert the proposal into a testable contract: what product, what package, what run conditions, what measurements, and what pass/fail rules. Without this, “passed FAT” is a phrase, not a result.
The line must arrive at the FAT with the configuration the buyer expects—not a generic machine that the supplier plans to reconfigure on the buyer’s site later. The buyer should confirm the line configuration (dosing station, piston insertion, closure station, inspection, controls) matches the URS before any product is run.
Agree the References Before Anyone Switches the Line On
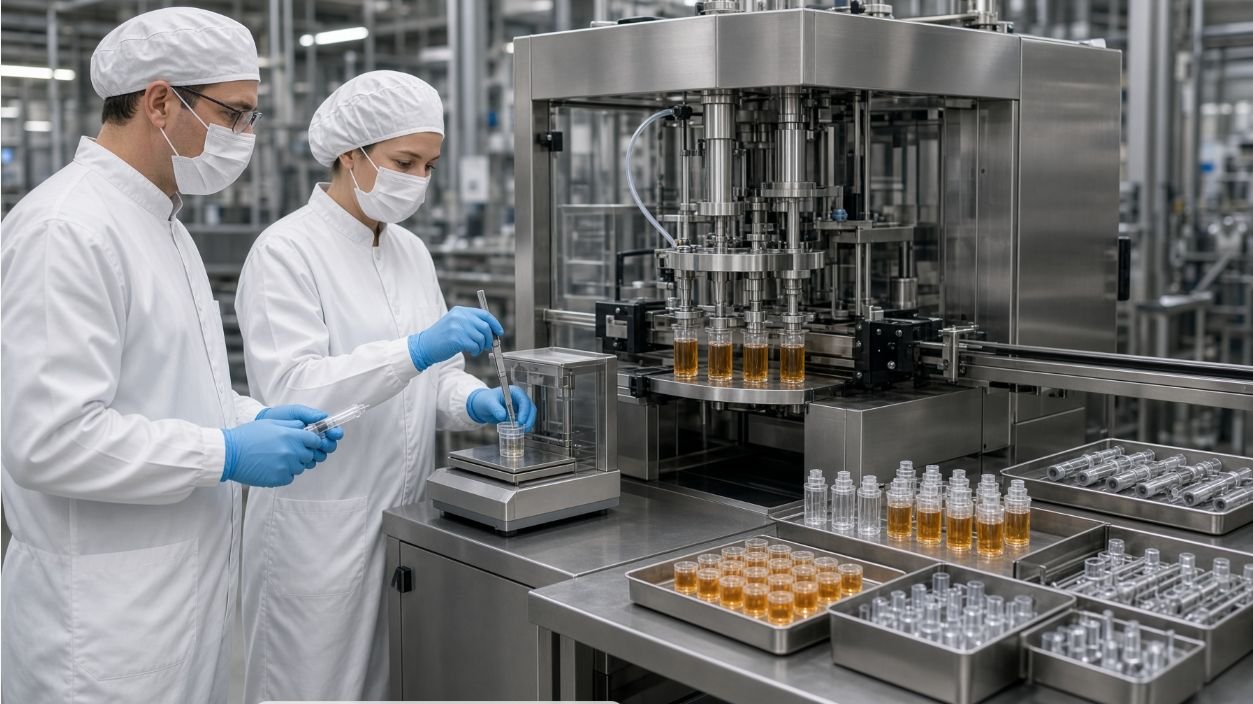
The first section of a gel bait syringe filling machine FAT is administrative but is the part most often left vague. Before the test starts, the buyer and the supplier should sign off on:
- Product reference. The exact paste to be used, with its batch or lot identity, SDS, and the storage conditions in the test room. Different batches of the same nominal product can behave differently; the FAT uses one agreed lot.
- Packaging reference. The exact barrel, piston, plunger, tip, and cap samples, with their lot identity and the supplier they came from. The packaging is part of the test, not a backdrop.
- Test protocol. A written procedure covering machine settings, run duration, sampling plan, and which defects are being investigated. The protocol should be signed by both sides before product is dosed.
- Acceptance criteria. The numeric targets and the pass/fail rules: net content tolerance, defect rate, throughput under agreed conditions, and what happens if any single criterion is missed.
If any of these is open, the test should not start. A “we’ll work it out during the test” agreement usually becomes a disagreement after the test.
Run Conditions and Measurement Methods
The FAT runs the line under conditions that match the buyer’s intended production, not the conditions the supplier finds convenient. The record should capture:
- Fill weight or volume target and the units in which it is recorded.
- Fill speed or throughput at which the test is run, with the understanding that real production may run faster or slower and that the FAT data point is a reference, not a maximum.
- Dosing temperature of the paste, the bulk container, and the ambient.
- Sampling frequency: how many units are pulled, at what intervals, and from which stations (e.g., dose, piston seat, closure, inspection).
- Measurement method: balance, calibrated volume reference, defect scoring method, and the operator role that records each reading.
These are the conditions under which any defect or deviation is judged. Without them, the test cannot be repeated on the buyer’s site with the same result.
Defects to Watch During the Run
A gel bait syringe filling line can produce four categories of defect, and a useful FAT investigates each separately.
- Fill defects. Net content outside the agreed tolerance; air pockets; voids at the tail under the piston; stringing or residue at the tip; gross overfill or underfill.
- Assembly defects. Piston mis-seat, twisted, or unsealed; plunger rod missing or mis-engaged; tip or cap not seated, crossed-threaded, or visibly loose.
- Package defects. Barrel deformation, flange damage, marking damage, tip damage from the fill nozzle, scratches or contamination introduced by the line.
- Process defects. Stoppages, restarts, manual interventions, alarms, rejects that were not flagged, and changes in cycle time during the run.
Each defect, when seen, is recorded with the time, the station, and the sample number. The list of “what to look for” is part of the test protocol; the list of “what was seen” is the test result.
Stoppages, Restarts, and Changeover Within the FAT
A line that runs without stopping for 30 minutes is not the same as a line that runs for 8 hours with two stoppages and a format change. The FAT should include the events that real production includes, or it should be honest about what it does not include.
- Stoppages. Both planned and unplanned stoppages are recorded. The cause, the duration, and how the line restarted are noted. A line that requires manual intervention to recover from a stoppage is not the same as one that auto-restarts.
- Restarts. The first units after a stoppage are often the worst units. The protocol should say whether restart units are counted, segregated, or both.
- Changeover. If the FAT covers more than one format, the changeover time, the parts changed, and the first-off checks on the new format are recorded. Changeover times written into a proposal are often aspirational; the FAT is where they become evidence.
The buyer should know, after the test, what the line does during the things that are not “good output.” That is usually where the real cost of ownership hides.
Deviations and Agreed Actions
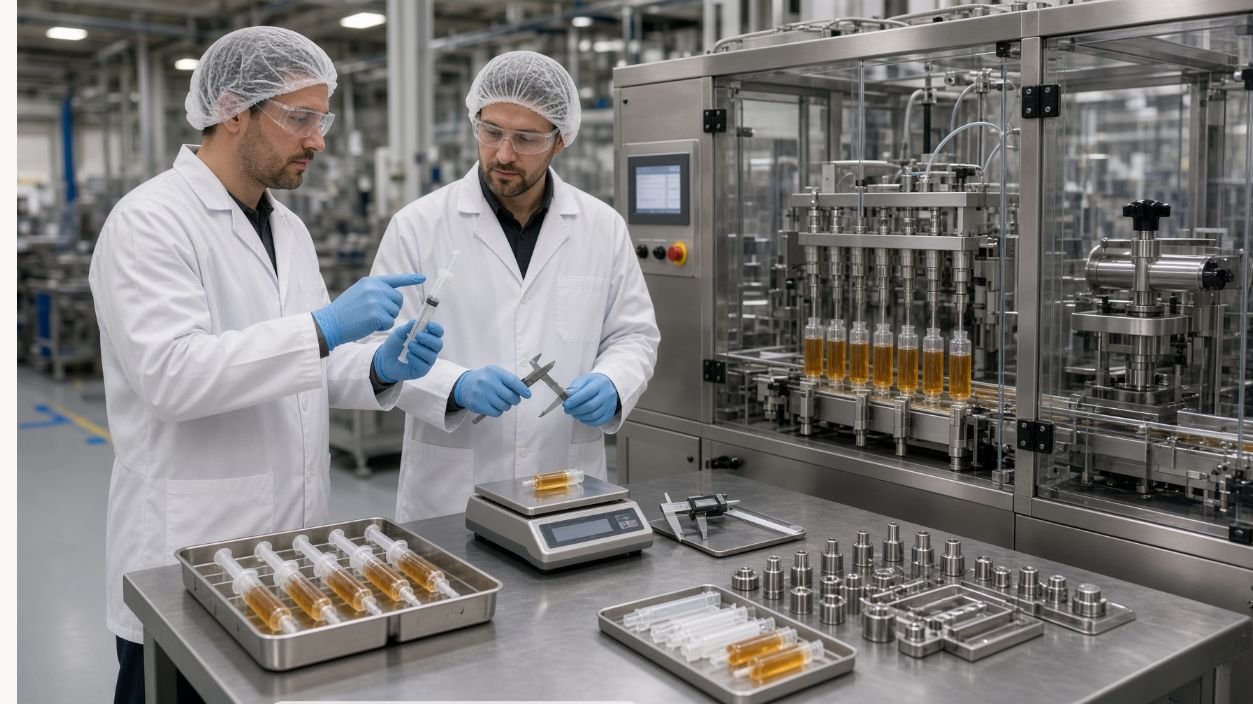
The most important column on a FAT record is not the pass/fail column; it is the deviation and action column. A deviation is anything that did not match the agreed protocol: a stoppage, a defect above the agreed rate, a measurement outside tolerance, a missing record, a setting change during the run. The agreed action says what will happen to the deviation: rework, concession, repeat test, or design change.
The supplier’s commitment to “fix it on site later” is a deviation, not a pass. It should be written down, with the responsible party and the closure date, so the buyer’s installation team can verify it later. A FAT record without deviations is suspicious; a line that runs long enough to generate none usually means the protocol was not strict enough.
Records the Buyer Should Take Away
The deliverable of a successful FAT is a record the buyer can keep. A minimum set:
- Signed test protocol with version and date.
- The product and packaging references used, with batch/lot numbers.
- The settings, speeds, and conditions run.
- The full set of measured results (net content, defect counts, cycle times, stoppages, changeovers).
- The deviation list with actions and owners.
- A signed statement of whether the line passed, passed with deviations, or failed.
Without the records, the FAT cannot be repeated. With them, the same protocol can be re-used during site acceptance, allowing a like-for-like comparison between the supplier’s floor and the buyer’s site.
Common Risks and Mistakes
- Treating the FAT as a machine demo. Without a protocol signed by both sides, the test is theatre, not evidence.
- Accepting the line because it ran. A line that runs without verifying net content or defect rates is unverified, not accepted.
- Letting deviations stay verbal. Anything that needs to be fixed on site should be written down with an owner and a date.
- Skipping changeover and restart in the test. Most real production includes both; if the FAT does not, the buyer should know what is unverified.
- Forgetting the data. A line that passed without a record cannot be defended at the buyer’s site or in a future audit.
How King Pack Supports This Application
King Pack Machinery (Wuxi King-Pack / Wuxi Jingpai Machinery Co., Ltd., founded 2009, with a core technical team carrying more than 20 years of industry experience) supports gel bait syringe filling line FATs as a buyer-driven acceptance step, not a sales event. The relevant support is:
- FAT protocol support. A draft test protocol built from the agreed URS, product, and packaging references, signed before product is run.
- Sample-based configuration. The line that arrives at the FAT is the configuration developed against the product and packaging the buyer supplies, not a generic machine.
- Records and deviation handling. Settings, results, deviations, and actions are recorded in a form the buyer can take away and re-use during site acceptance.
- Closure on agreed actions. Deviations carry owners and dates; the buyer’s installation team can verify the same list on site.
King Pack does not present a passed FAT as a marketing claim. A passed FAT is the buyer’s evidence that the line matches the specification the buyer wrote. That evidence is what should travel with the line.
Conclusion
A gel bait syringe filling line FAT protects the buyer only when it is treated as a specification match with a written protocol, agreed references, and a deviation list. The deliverable is a record, not a handshake. The record is what makes “passed FAT” mean the line will perform on the buyer’s site.
Ready to define the acceptance test for your line? Send your URS, product and packaging references, and the defects you need the test to investigate, and request a draft FAT protocol.