 Skip to content

Last reviewed: September 16, 2026.
Vial filling and stoppering defects should be investigated by machine zone and operating state. Fill-weight variation may originate in the bulk feed, dosing path, nozzle, vial position or measurement method. A tilted or incomplete stopper may originate in component preparation, bowl and track behavior, transfer tooling, vial centering, insertion motion or the selected stopper-vial combination. Looking only at the final defective unit can hide where the variation begins.
This is a defect-led FMEA and corrective-action guide, not another overview of vial packaging equipment. The existing KING PACK vial filling efficiency and accuracy overview remains the broad introduction; this page owns the diagnostic path from symptom to observation, confirmatory test and controlled action.
Quick answer: Map each defect to the earliest machine zone that can create it, then compare good and defective units by time, dosing head, vial lane, component lot and machine state. Confirm the suspected cause with one controlled change or challenge at a time. Fill-weight variation usually requires checking bulk condition, feed pressure or level, air, pump and valve behavior, nozzle cutoff, vial centering and the measurement system. Stopper tilt or incomplete seating requires checking component condition, feed orientation, pickup and transfer, vial support, tooling alignment, insertion motion and approved stopper-vial tolerances. Never use a generic machine setting or visual judgment as the sole acceptance rule.
1 Build a Defect Map Before Adjusting the Machine
Direct answer: Describe the defect, location, timing and affected population before changing a parameter.
Create a defect code with photographs or measurements for underfill, overfill, variable fill, foam, splash, nozzle drip, vial damage, missing stopper, tilted stopper, high or low seating and visible closure contamination. Record whether the result is continuous, intermittent, head-specific, lane-specific, lot-specific or linked to startup, refill, stop, restart or batch end.
Quarantine affected units according to site procedure and preserve raw results. Link the sample to product batch, bulk age and temperature, vial and stopper lots, machine recipe, operator, time, alarm and intervention history. Without that context, a maintenance adjustment can remove the symptom while the true cause remains.
Start with the earliest zone capable of generating the observation and move downstream. Use one justified controlled change at a time, document the result and restore the approved condition when the test ends. Changes to validated settings require the site change and deviation process.
| Observed defect | First zones to review | Confirmatory evidence |
|---|---|---|
| Fill variation | Bulk feed, pump/valve, nozzle, vial position | Time/head/state sample map |
| Foam or splash | Bulk air, fill profile, nozzle height | Video and stop/restart challenge |
| Tilted stopper | Feed, pickup, vial center, insertion | Component and tooling measurements |
| Incomplete seating | Stopper/vial, contamination, force and motion | Height/force and functional test |
2 Separate Filling Modes from Stoppering Modes
Direct answer: A unit can show both a dose defect and a stopper defect, but the investigation should test each failure chain separately before examining interactions.
For filling, follow material from the bulk vessel through transfer, hopper or balance tank, pump, valves, tubing and nozzle into a centered vial. For stoppering, follow prepared components through the hopper, bowl, track, escapement, pickup, transfer, insertion and final seated condition. Put each sensor and actuator on the map.
Then identify interactions. Splash can contaminate the vial finish or stopper zone and make closure placement unstable. An off-center vial can receive a poor fill and also meet the stopper tool incorrectly. A stoppering jam can create upstream accumulation and an unusual fill restart. The sequence of timestamps and affected units helps establish direction.
Assign observations to production, maintenance, quality and engineering roles before the trial. One team should control parameter changes and another should verify samples when required. This avoids multiple simultaneous adjustments and incomplete records.
3 Diagnose Vial Fill-Weight Variation
Direct answer: Fill-weight variation should be analyzed against product state, feed condition, dosing-head identity and line state.
Check bulk homogeneity, temperature, density when used in calculations, foaming or entrained air, hold time and transfer conditions. Review hopper level and refill cycles because changing inlet pressure or product head can expose a marginal pump or valve setup. Air leaks, incomplete priming and loose connections may produce intermittent low results.
Inspect pump chambers, seals, check valves, tubing, manifolds and nozzle cutoff for wear, blockage, trapped air and product buildup. Confirm the correct parts and recipe are installed. Compare results by dosing head and time. A consistent offset on one head points toward a local path; drift across all heads may point toward bulk, feed or measurement conditions.
Verify the weighing or analytical method before changing the filler. Use identified containers, a suitable in-calibration instrument, controlled tare and the approved calculation. Challenge startup, normal run, refill, low feed, stop, restart and batch end. FDA process-validation guidance supports monitoring that connects process inputs and variability to output rather than relying on a single final test.
4 Control Foaming, Splashing and Nozzle Drips
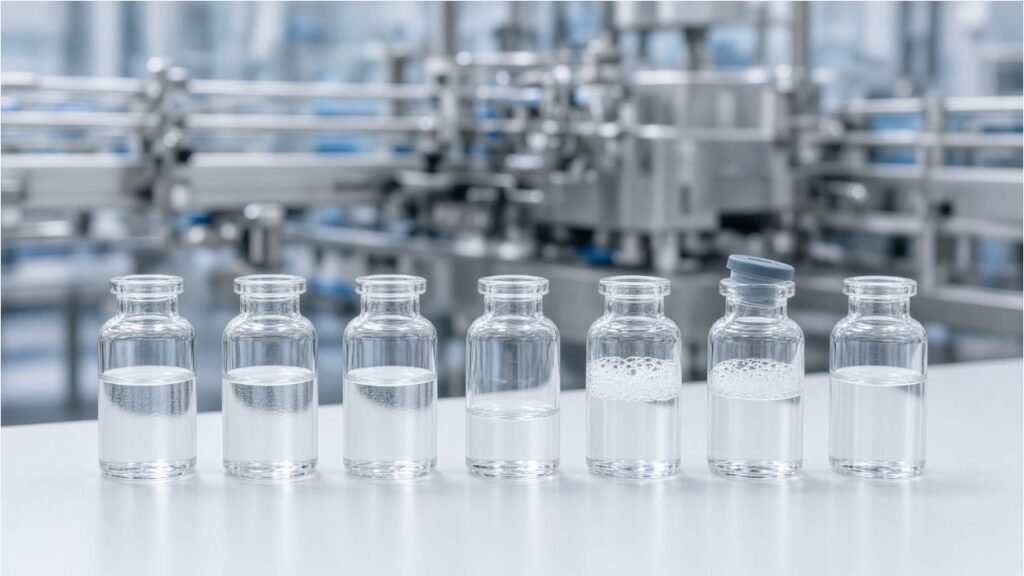
Direct answer: Reduce air at the source and synchronize the fill profile, nozzle position and cutoff with actual product behavior.
Investigate whether air entered during compounding, transfer, hopper refill or dosing. Excess agitation, a falling product stream, vortexing, leaky suction connection or aggressive return can create bubbles before the nozzle. Product temperature and viscosity can change bubble release and stringing, so record them during defect trials.
Review nozzle diameter, height, centering, entry depth, bottom-up motion, fill speed stages, cutoff and any suck-back. A very fast initial flow can splash an empty vial; a poorly timed withdrawal can entrain air or drag product onto the neck. Excessive suck-back can create its own dosing or air problems. Optimize the full sequence rather than one setting in isolation.
Use high-speed or ordinary video, white-background inspection and timed samples to compare acceptable and defective cycles. Include stop and restart because drips and strings often occur after dwell. Define cleaning and disposition when product reaches the closure zone; wiping without investigation can turn a process defect into an undocumented manual intervention.
5 Check Vial Transport and Centering
Direct answer: Stable filling and stoppering require each vial to arrive upright, supported and centered at the correct time.
Inspect infeed guides, feed screw, starwheels, pucks, side rails, dead plates, transfers and accumulation pressure. Look for chips, scuffs, wobble, sliding, gaps and contact at the neck or finish. Verify the format parts and recipe match the vial drawing and that adjustment points have not moved.
Use samples across expected dimensional tolerances and, where justified, different lots. Measure the vial datum that the machine actually controls. Nominal diameter alone may not explain a base, shoulder or finish variation that changes support. Transparent glass can also challenge presence sensors, so test under real lighting and background conditions.
Observe centering under the filling nozzle and stopper tool at startup, speed changes, accumulation and restart. A vial that appears centered while static may lag or bounce during indexing. Record mechanical marks and timing, then correct worn or misadjusted parts before compensating with nozzle or stopper-tool offsets.
6 Diagnose Stopper Feeding and Orientation
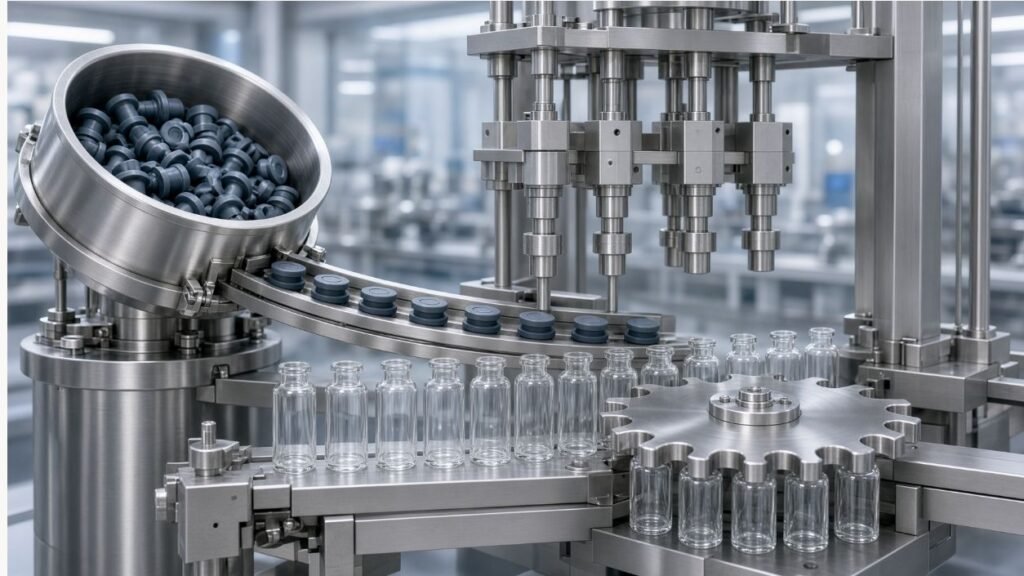
Direct answer: Stopper defects often begin before insertion, in component preparation, bulk presentation or feed-track control.
Confirm the stopper item, drawing revision, material, preparation method, surface condition, storage and lot. Prepared stoppers may behave differently from dry engineering samples. Moisture, sticking, static, deformation or excess bulk load can change bowl and track performance without an obvious machine fault.
Inspect the hopper, bowl surface, track width, air jets or mechanical aids, escapement and low-level control. Challenge inverted, nested, doubled, damaged and missing components using approved samples. The system should prevent or detect the defined fault and produce the specified stop or reject response.
Clean components and tracks according to approved procedures and avoid unrecorded lubricants or ad hoc surface treatments. If a feed setting is changed, test the full expected stopper condition and line speed range. A setting that resolves one lot may create damage or misorientation with another.
7 Correct Partial, Tilted and Incomplete Stopper Seating
Direct answer: Compare stopper-vial compatibility, vial support, transfer alignment and insertion motion before increasing force.
Measure incoming vial finish and stopper dimensions against approved specifications and inspect for damage, particles or product contamination. Confirm the stopper is correctly presented to the pickup tool and remains stable through transfer. Check tooling wear, vacuum or grip performance and release timing where applicable.
Verify vial center, support height, stopper-tool concentricity, vertical travel, speed profile and approved force or position indicators. Increasing insertion force can damage components or hide misalignment; it should not be the first response. Compare good and defective cycles with measured positions and video when possible.
Define the accepted seated state through the product and package control strategy. Visual appearance may be one check, but height, force, functional testing or container-closure integrity evidence may also apply. The equipment supplier can demonstrate repeatable placement; the manufacturer owns package suitability and release criteria.
| Finding | Likely check | Controlled action |
|---|---|---|
| Tilt always points one direction | Tool/vial center and guide alignment | Correct alignment and retest |
| Random tilt after feed disturbance | Stopper orientation and pickup stability | Correct feed/transfer cause |
| High seating after neck splash | Nozzle cutoff and closure-zone cleanliness | Control fill and segregate affected units |
| Lot-specific seating change | Component dimensions and surface state | Assess component lot and settings under change control |
8 Review Vacuum, Headspace and Process Interfaces
Direct answer: Vacuum or gas-handling settings must follow the approved product process and package studies, not a generic vial-line value.
Document whether the process uses ambient headspace, inert-gas overlay, vacuum stoppering, partial stoppering or another defined sequence. Identify the quality attribute or process purpose, required instrumentation, control range and alarm response. The equipment specification should match that approved intent.
Check seals, tubing, valves, filters, pressure or vacuum instruments, timing and the relationship to stopper placement. A leak or timing error can change the process while the final stopper appears acceptable. Use suitable challenge methods and traceable instruments, and separate machine-function evidence from product-specific headspace or integrity studies.
For sterile processing, apply the manufacturer's contamination-control strategy and applicable requirements. FDA aseptic-processing guidance and EU GMP Annex 1 provide current regulatory context but do not prescribe a universal vacuum level, residual oxygen limit or stopper position for every product.
9 Design In-Process Checks that Locate the Cause
Direct answer: An effective IPC plan samples by head, time and machine state so results can point back to a specific failure mechanism.
For fill results, define tare, weight or volume method, sample frequency, head or lane identification and calculation. For stoppers, define presence, orientation, height or position and the approved functional check. Add visual criteria for splash, foam, neck contamination and container damage with reference examples where possible.
Place additional samples around startup, bulk refill, planned stop, intervention, restart and batch end. Trend individual and grouped results rather than only a batch average. A satisfactory average can hide one unstable dosing head or a short cluster of tilted stoppers.
Link automatic inspection and reject data to offline checks. Challenge the reject device, confirmation sensor, bin presence and reconciliation using defined defect samples. Inspection limits should be documented honestly; no vision or sensor system should be described as detecting defects it has not been challenged to see.
10 Use an FMEA-Based Corrective-Action Checklist
Direct answer: Corrective action should remove or control the verified cause and include evidence that the defect did not move elsewhere.
State the failure mode, effect, suspected cause, current controls and objective evidence. Prioritize by patient or product risk, occurrence and detectability according to the site's method. Immediate correction may restore operation, while corrective action can require component, procedure, maintenance, training or design change.
After action, repeat the relevant challenge across the approved range and line states. Check related outputs: a nozzle change intended to stop splash may affect dose; a stopper-tool change may affect component damage or line speed. Update settings, drawings, recipes, maintenance tasks and training through change control.
Use the KING PACK vial filling maintenance guide for preventive-maintenance context, while keeping product and closure investigations within the approved quality system. Escalate recurring defects rather than normalizing repeated adjustment.
11 Evaluate Supplier Evidence and Review the Case with KING PACK
Direct answer: A supplier should convert the actual defect, product and package inputs into a controlled test plan rather than offer a generic setting change.
Request a product-path and component-path drawing, dosing rationale, nozzle and stopper-tool details, format-part list, sensor and reject matrix, alarm history, maintenance evidence and proposed challenge protocol. Ask which observations distinguish feed, dosing, transport and stoppering causes and which tests require the manufacturer's quality approval.
KING PACK Machinery supplies pharmaceutical, veterinary, cosmetic and liquid filling and packaging equipment, including vial filling and stoppering, bottle filling and capping, tube filling and sealing, syringe filling and vacuum emulsifying systems. The KING PACK pharmaceutical solutions page and filling and capping platform provide equipment context without replacing a product-specific investigation.
Send vial and stopper drawings and samples, fill volume, product viscosity and foaming behavior, bulk and line conditions, defect photographs or measurements, result trends, current settings and approved test methods through the KING PACK contact page. KING PACK can then review the responsible zones and propose a representative trial. Final corrective action, validation and batch disposition remain with the manufacturer.
Frequently Asked Questions
What is the first step when vial fill weight varies?
Confirm the measurement method and map results by time, dosing head, line state, bulk condition and component lot before changing a setting.
Can low hopper level cause fill variation?
It can expose feed-pressure, air or pump-response problems on some systems. Challenge the approved operating band with representative product instead of assuming a universal effect.
Why does a vial filler splash during startup?
Possible causes include trapped air, aggressive initial flow, incorrect nozzle height, off-center vials or unstable product condition. Observe the complete priming and first-fill sequence.
Why are stoppers tilted in only one direction?
A consistent direction often points to vial support, guide or tooling alignment, but measurements and cycle observation should confirm the cause.
Should insertion force simply be increased?
No. First check component condition, contamination, centering, pickup, tooling alignment and motion. Excess force can damage the closure or hide the real problem.
How should stopper seating be accepted?
Use the approved product-package criteria, which may include position, height, force, functional or integrity evidence. Visual appearance alone may be insufficient.
What should an IPC trend include?
Include head or lane, time, line state, component lot, product condition, intervention and individual results so clusters and local causes remain visible.
What should be sent to KING PACK for review?
Send vial and stopper samples and drawings, product and fill data, defect evidence, current recipe, operating-state history and approved test methods.
